

What is a High-Pressure Bin Pump Powder Handling Equipment? And What Are Its Design Principles?
High-pressure bin pumps are specialized industrial equipment designed for the efficient and reliable transport of bulk powder materials. These systems are widely used across various industries, including chemical, pharmaceutical, food processing, and mining, where the safe and controlled movement of powders is critical. The technology behind high-pressure bin pumps combines advanced engineering with robust construction to ensure optimal performance under demanding conditions.
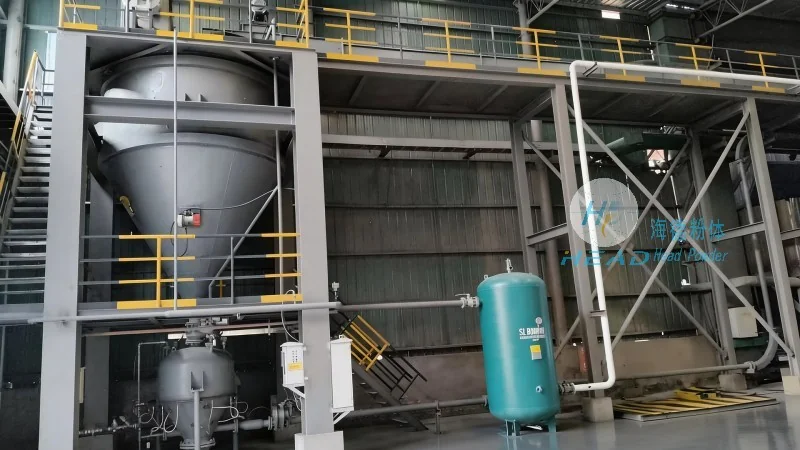
Overview of High-Pressure Bin Pump Systems
A high-pressure bin pump, often referred to as a pressure bin or pressure vessel pump, operates by creating a pressure differential to move powders from a storage bin or hopper to the discharge point. The core components typically include a hopper, a pump chamber, a drive mechanism, and a discharge valve. The hopper stores the bulk material, while the pump chamber is sealed and pressurized to force the powder through the discharge line. This design allows for continuous or intermittent operation, depending on the application requirements.
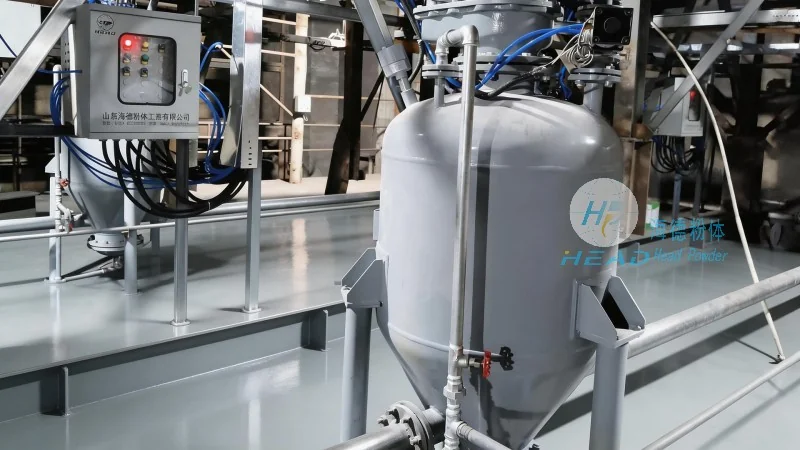
Key Design Principles of High-Pressure Bin Pumps
The design of high-pressure bin pumps is guided by several fundamental principles to ensure efficiency, safety, and durability. First, the system must maintain a consistent pressure within the pump chamber to prevent material bridging or caking, which can impede flow. This is achieved through precise control of the air or gas used to pressurize the chamber. Second, the construction materials must be compatible with the powder being handled, as some powders may be corrosive or abrasive. Stainless steel, alloy steels, and specialized polymers are commonly used to withstand wear and chemical exposure. Third, the pump's sealing system is critical to prevent leaks and maintain the pressure differential. Advanced sealing technologies, such as mechanical seals or double seals, are employed to ensure long-term reliability.
Operational Mechanisms and Efficiency Considerations
High-pressure bin pumps typically use a positive displacement mechanism, where the pump chamber is repeatedly filled and emptied to move material. This method ensures a consistent flow rate, even with varying powder characteristics. The drive mechanism, which may be electric, pneumatic, or hydraulic, controls the speed and pressure of the pump. Efficiency is further enhanced by features like automatic pressure regulation and material level sensors. These sensors monitor the hopper level and adjust the pump operation to prevent overfilling or underfilling, optimizing the overall process.
Applications and Industry Impact
High-pressure bin pumps are essential in industries where bulk powder handling is a core operation. In the chemical industry, they are used to transport raw materials and finished products, ensuring smooth production lines. In pharmaceutical manufacturing, the equipment's ability to handle sensitive powders with minimal contamination is crucial for maintaining product quality. The mining sector also benefits from these systems, as they efficiently move ore and other mineral powders from storage to processing facilities. The consistent and controlled flow provided by high-pressure bin pumps reduces downtime and improves overall operational efficiency.
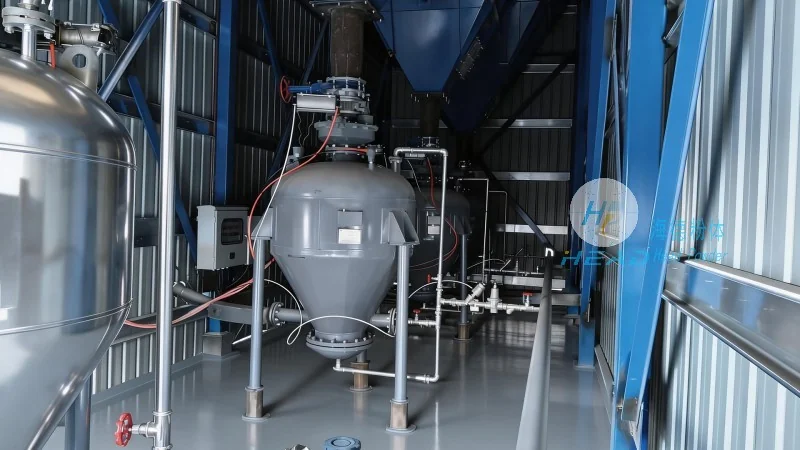
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of high-quality powder handling equipment. Based in Shandong, China, the company specializes in designing and producing advanced high-pressure bin pumps and related systems. HeadPowder's commitment to innovation and customer satisfaction has established it as a trusted partner in the industry, providing reliable solutions for diverse powder handling challenges. The company's products are engineered to meet international standards and are tailored to meet the specific needs of each client, ensuring optimal performance and longevity.