

What is a Fly Ash Silo Powder Conveying Machine? And What Are Its Design Principles?
Understanding the functionality and design principles of fly ash silo powder conveying machines is crucial for industries dealing with bulk material handling, particularly in power generation and construction sectors. These specialized equipment are engineered to efficiently transport fly ash from storage silos to processing or application points, ensuring smooth operational flow and material management.
Key Components and Design Principles
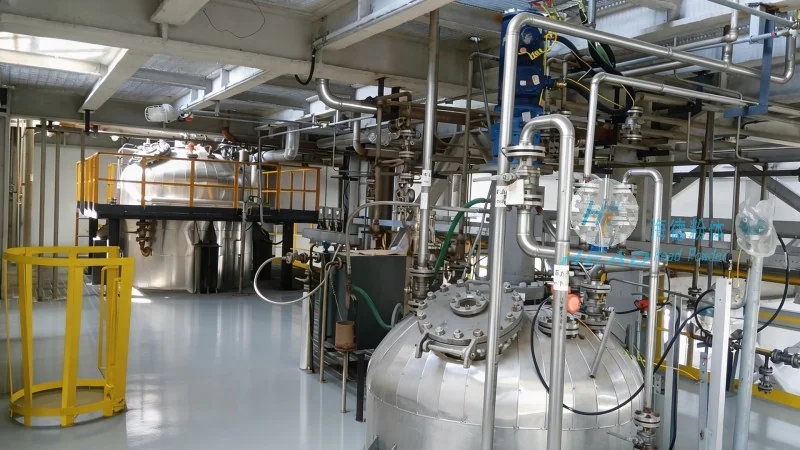
At the core of a fly ash silo powder conveying machine are several critical components that work in tandem to achieve reliable material transport. The system typically includes a silo hopper, a conveying mechanism (such as screw conveyors or pneumatic systems), and control units. The design emphasizes durability and efficiency, with materials like stainless steel or corrosion-resistant alloys used to withstand the abrasive nature of fly ash. The conveying mechanism is often designed with variable speed controls to adjust flow rates based on operational needs, ensuring precise material delivery.
How the Conveying Process Works
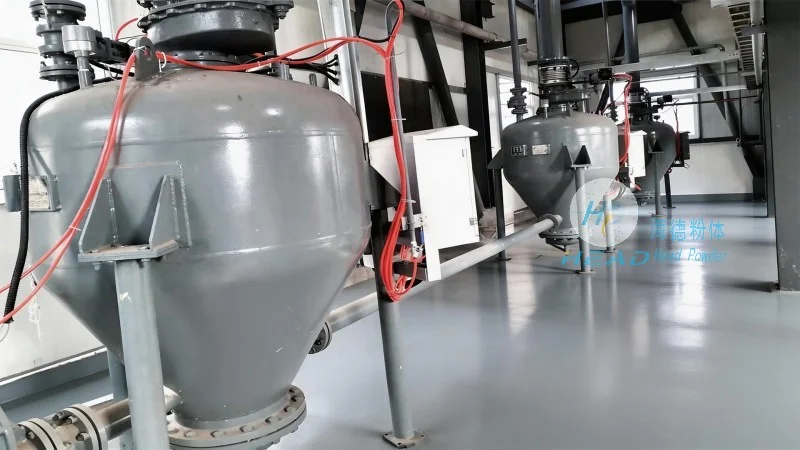
The operation of a fly ash silo powder conveying machine involves a sequence of steps that ensure seamless material transfer. Initially, fly ash is stored in the silo, where it accumulates under gravity. The conveying system then activates, drawing the material from the silo through the hopper and into the conveying pipe. Depending on the system type—whether mechanical (e.g., screw conveyors) or pneumatic (e.g., air-assisted systems)—the material is moved to the desired destination. Mechanical systems use rotating screws to push the material forward, while pneumatic systems utilize compressed air to create a flow that transports the fine particles. The design incorporates features like flow control valves and pressure sensors to maintain consistent performance and prevent blockages.
Applications and Industry Relevance
Fly ash silo powder conveying machines are widely used in power plants, where fly ash is a byproduct of coal combustion. The equipment facilitates the removal of fly ash from storage silos to disposal sites or recycling facilities. In construction, these machines are employed to transport fly ash for use as a supplementary cementitious material in concrete production, enhancing the durability and strength of building materials. The efficiency of these systems directly impacts operational costs and environmental compliance, making them essential for sustainable material handling practices.
Advantages of Using HeadPowder's Fly Ash Silo Powder Conveying Solutions
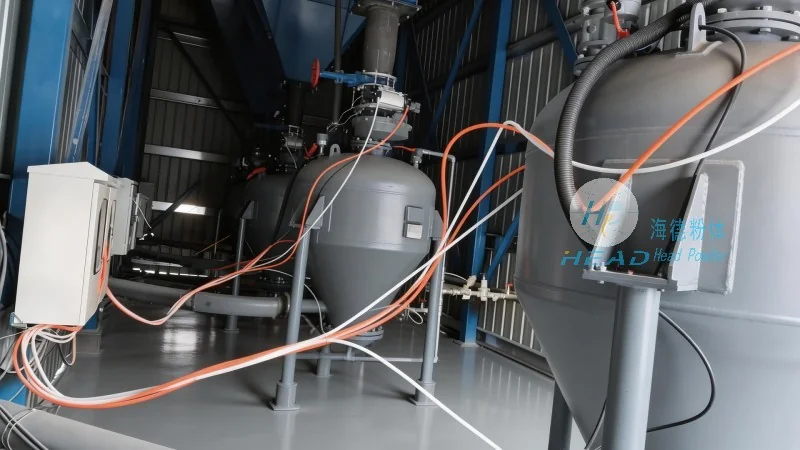
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, offers advanced fly ash silo powder conveying machines that combine reliability, efficiency, and durability. The company’s products are engineered to meet the specific needs of industrial applications, with features tailored to handle the unique characteristics of fly ash—such as its fine particle size and abrasive properties. HeadPowder’s systems are designed for low maintenance, with robust components that reduce downtime and operational costs. The company’s commitment to quality and innovation ensures that their conveying machines deliver consistent performance, supporting long-term operational efficiency for clients in the power and construction industries.