

What is a Coal and Coke Powder Conveyor? What Are Its Design Principles?
Coal and coke powder conveyors are specialized industrial equipment designed to transport fine powders, such as coal, coke, and other similar particulate materials. These systems are essential in various industrial sectors, including power generation, metallurgy, and chemical processing, where efficient and reliable material handling is critical for operational efficiency and safety. The design of these conveyors must address several key challenges, including the prevention of material segregation, the control of dust emissions, and the maintenance of consistent material flow rates. Understanding the underlying design principles is crucial for selecting the appropriate equipment for specific industrial applications.
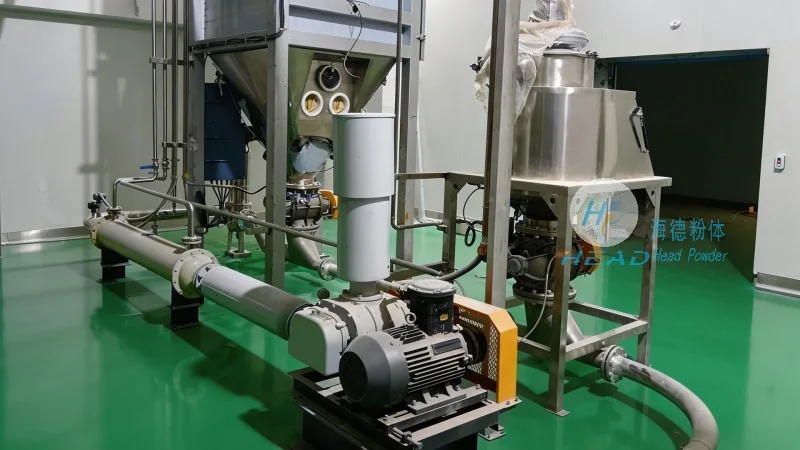
Key Design Principles of Coal and Coke Powder Conveyors
The design of coal and coke powder conveyors is governed by several fundamental principles that ensure optimal performance. One of the primary considerations is the selection of appropriate materials for the conveyor components, such as the hopper, ducting, and discharge mechanisms. These components must be resistant to corrosion and wear caused by abrasive powders, ensuring long-term durability and minimal maintenance. The hopper design is particularly important, as it must minimize material segregation and ensure uniform feeding into the conveyor system. A well-designed hopper with smooth, sloped walls helps prevent the accumulation of material and reduces the risk of blockages. Additionally, the ducting system is engineered to maintain consistent air velocity and pressure, which is vital for preventing dust accumulation and ensuring smooth material transport. The discharge mechanism, often equipped with adjustable valves or gates, allows for precise control over the flow rate, enabling operators to regulate the output based on downstream processing requirements.
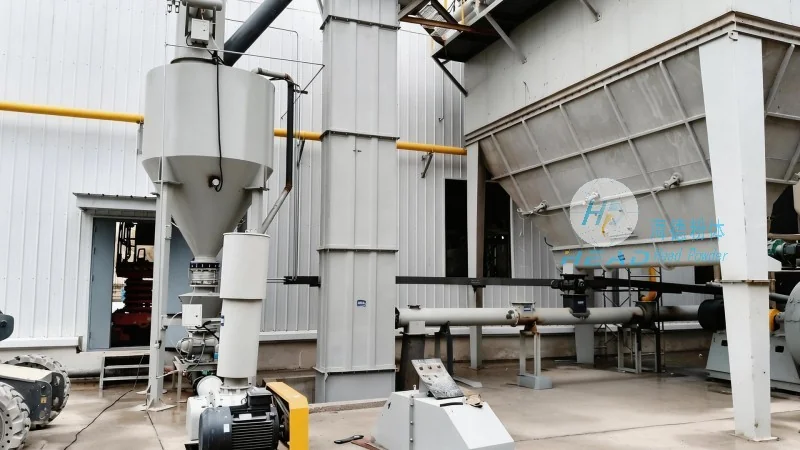
Components and Functional Aspects
Coal and coke powder conveyors typically consist of several key components that work in concert to achieve efficient material transport. The feeding hopper is the first component, responsible for receiving and storing the bulk material. It is usually equipped with a feeding device, such as a rotary valve or a screw feeder, which controls the rate at which material enters the conveyor. The conveyor itself, which can be a pneumatic or mechanical system, transports the material through the ducting network. Pneumatic conveyors use compressed air to move the powder, while mechanical conveyors rely on belts, screws, or buckets to transport the material. The choice between these systems depends on factors such as the material's properties, the required transport distance, and the desired flow rate. The ducting system is designed to minimize pressure drop and maintain consistent air flow, which is critical for preventing material settling and ensuring smooth transport. The discharge section is the final component, where the material is released into the processing equipment. This section is often equipped with filters or dust collection systems to control emissions and comply with environmental regulations.
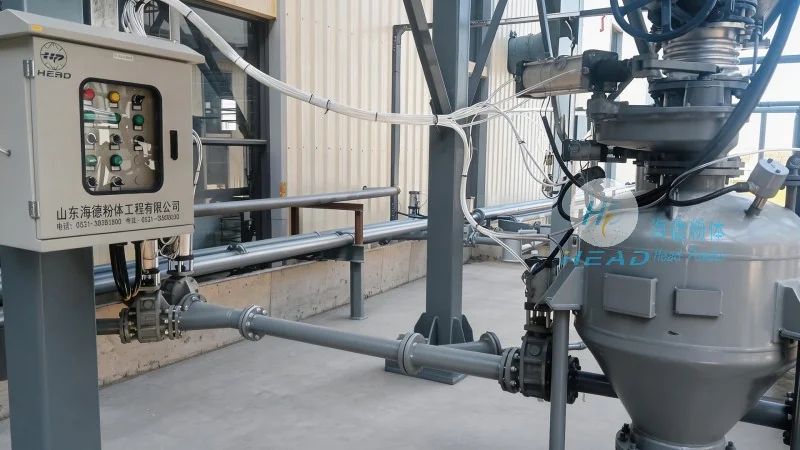
Applications in Industrial Settings
Coal and coke powder conveyors are widely used in various industrial applications where the handling of fine powders is essential. In power plants, these systems are used to transport coal from storage silos to the boiler, ensuring a continuous and reliable fuel supply. In metallurgical plants, they are employed to transport coke, a key ingredient in steel production, from storage areas to the blast furnace. The chemical industry also utilizes these conveyors for transporting raw materials such as limestone or coal ash, which are used in the production of chemicals and fertilizers. The ability to handle abrasive and fine materials makes these conveyors suitable for a wide range of applications, from small-scale processing to large-scale industrial operations.
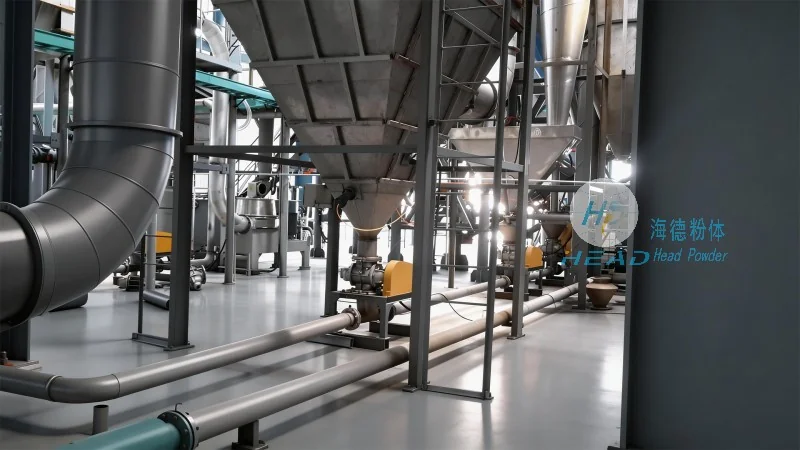
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial conveyor systems specializing in coal and coke powder handling. The company is headquartered in Shandong, China, and has established a strong reputation for providing high-quality, reliable equipment tailored to the specific needs of its clients. HeadPowder's team of engineers and technicians is dedicated to developing innovative solutions that address the unique challenges of powder transport in various industrial sectors. The company's products are designed with a focus on durability, efficiency, and safety, ensuring that they meet or exceed industry standards and regulatory requirements. With years of experience in the field, HeadPowder has built a comprehensive portfolio of conveyor systems, including pneumatic and mechanical designs, to cater to diverse industrial applications. The company's commitment to quality and customer satisfaction has made it a trusted partner for many industries worldwide.