

Coal Ash Material Handling Equipment: What It Is and Its Design Principles
Coal ash, a byproduct of coal combustion in power plants and industrial facilities, requires specialized equipment for safe and efficient transportation. This article explores the role of coal ash material handling equipment and the fundamental design principles that govern its operation, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
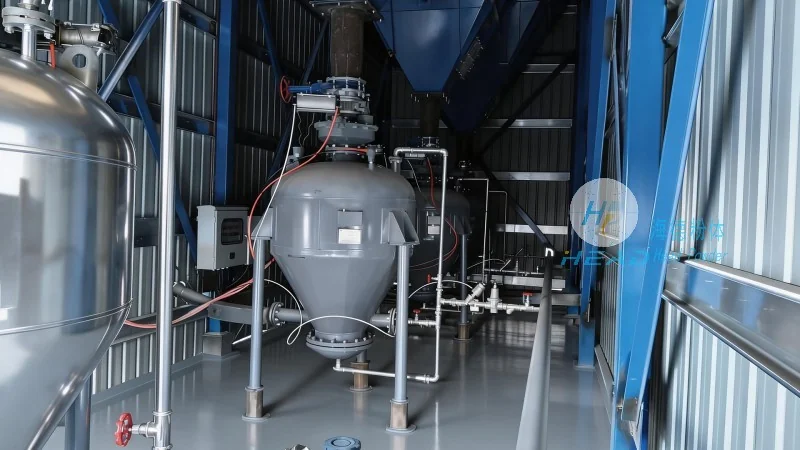
Introduction to Coal Ash Material Handling Equipment
Coal ash material handling equipment is a critical component in the management of coal ash, which is generated during the burning of coal for energy production. These systems are designed to collect, transport, and store coal ash from its source to disposal or utilization sites. The equipment must address the unique challenges posed by coal ash, such as its abrasive nature, varying particle sizes, and potential for dust generation. Effective handling equipment ensures compliance with environmental regulations and enhances operational safety in industrial settings.
Understanding the Core Function of Coal Ash Handling Systems
The primary function of coal ash material handling equipment is to facilitate the movement of coal ash from its generation point to subsequent processing or disposal. This involves several key processes, including collection, conveyance, and storage. The equipment must be capable of handling large volumes of ash while maintaining minimal dust emissions and preventing material degradation. For instance, conveyor belts, screw conveyors, and pneumatic systems are commonly used to transport coal ash, each with specific advantages depending on the application and ash characteristics.
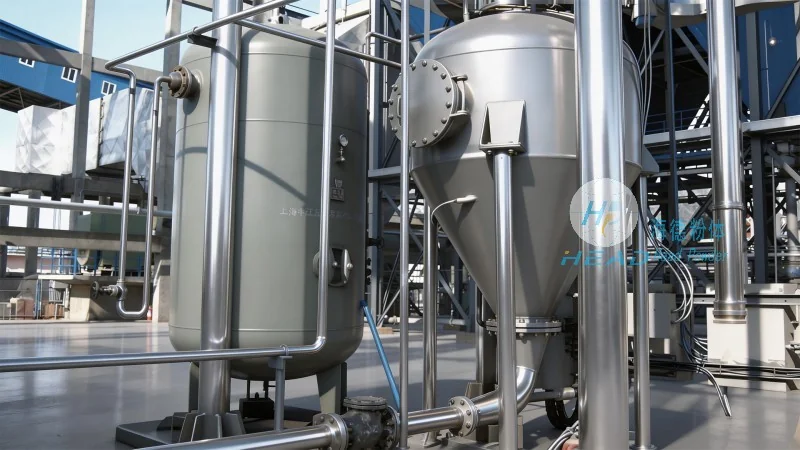
Key Design Principles Behind Coal Ash Material Handling Equipment
The design of coal ash material handling equipment is guided by several critical principles to ensure efficiency, durability, and safety. First, the equipment must be constructed from materials that can withstand the abrasive and corrosive properties of coal ash, such as high-strength steel or specialized coatings. Second, the system should minimize dust generation through features like sealed enclosures and efficient dust collection systems, as airborne ash particles pose health risks and environmental concerns. Third, the design must prioritize energy efficiency to reduce operational costs, often achieved through optimized conveyor speeds and reduced friction in components. Additionally, the equipment should be modular and adaptable to accommodate changes in ash volume or processing requirements, ensuring long-term usability.
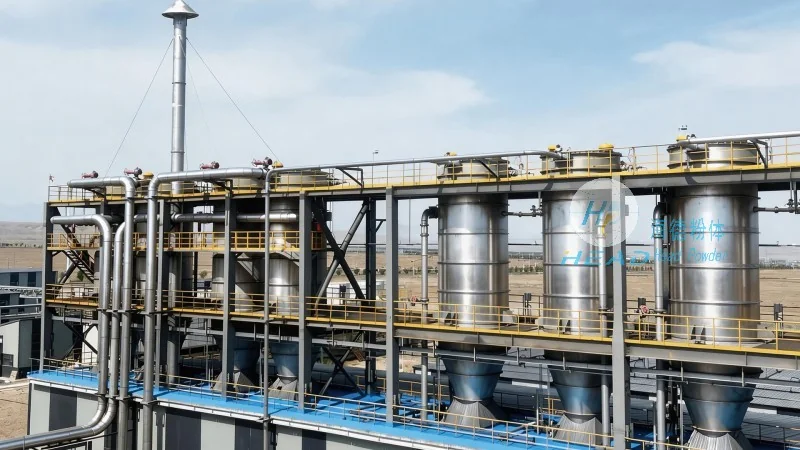
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of coal ash material handling equipment based in Shandong, China. The company specializes in the design, development, and production of advanced systems tailored to the unique needs of coal ash management. HeadPowder's expertise lies in integrating cutting-edge technology with robust engineering to deliver reliable and efficient solutions for industrial clients. The company's products are widely used in power plants, cement factories, and other facilities that generate significant amounts of coal ash, helping to improve operational efficiency and environmental compliance.
Technical Specifications and Application Scenarios
Coal ash material handling equipment from HeadPowder typically includes a range of components designed to handle different ash types and volumes. For example, their conveyor systems are engineered to handle ash with particle sizes ranging from fine powders to larger lumps, with adjustable speed controls to optimize material flow. The equipment also features dust suppression mechanisms, such as water sprayers or enclosed ducts, to minimize environmental impact. Applications of these systems include transporting ash from boilers to storage silos, conveying ash to utilization facilities for cement production, or moving ash to landfills in compliance with regulatory standards. Each system is customized to meet the specific requirements of the client, ensuring optimal performance and cost-effectiveness.