

What is Mineral Powder Material Handling? And What Are Its Design Principles?
Mineral powder material handling refers to the process of transporting, storing, and managing bulk mineral powders such as ores, coal, and other fine particulate materials. This critical operation is essential in industries like mining, chemical processing, and manufacturing, where efficient material movement directly impacts productivity and operational costs. The goal of mineral powder handling is to ensure safe, reliable, and cost-effective movement of these materials from extraction sites to processing facilities or storage areas. It involves a range of equipment and techniques designed to handle the unique challenges of mineral powders, including their tendency to flow, clog, or create dust. Proper material handling not only improves operational efficiency but also enhances workplace safety by reducing the risk of accidents and environmental contamination.
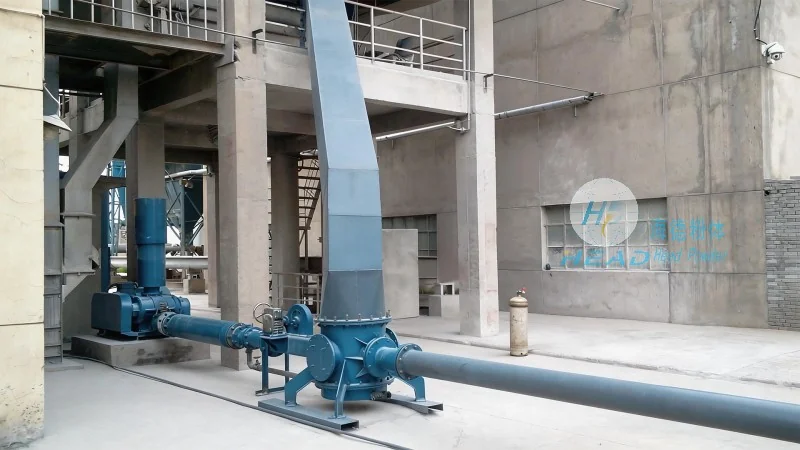
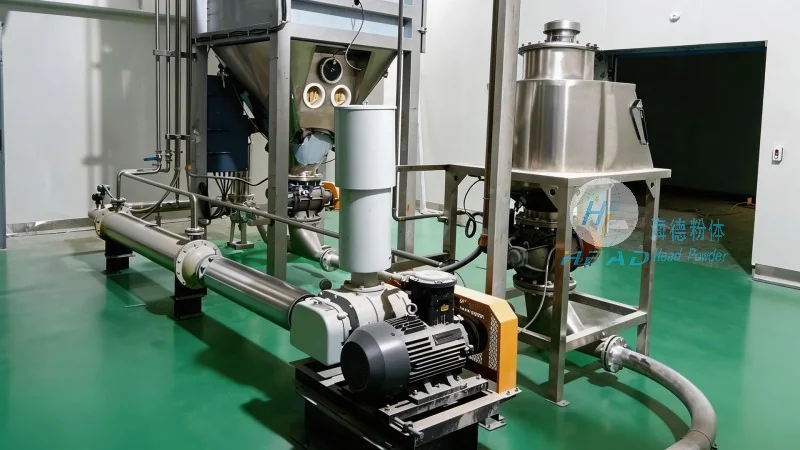
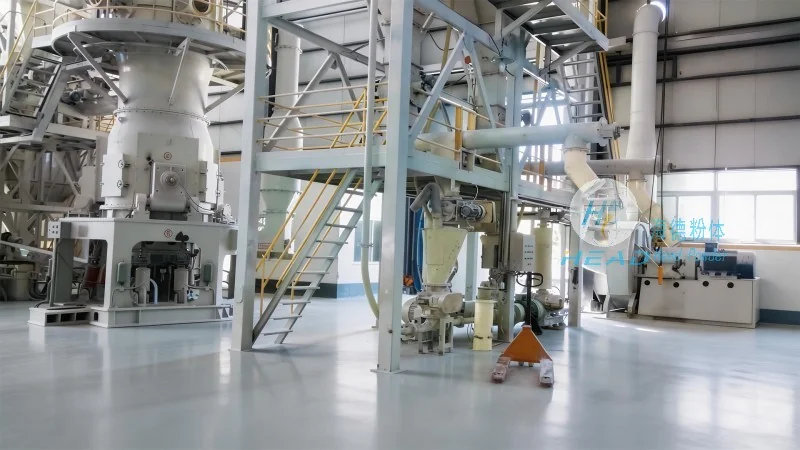
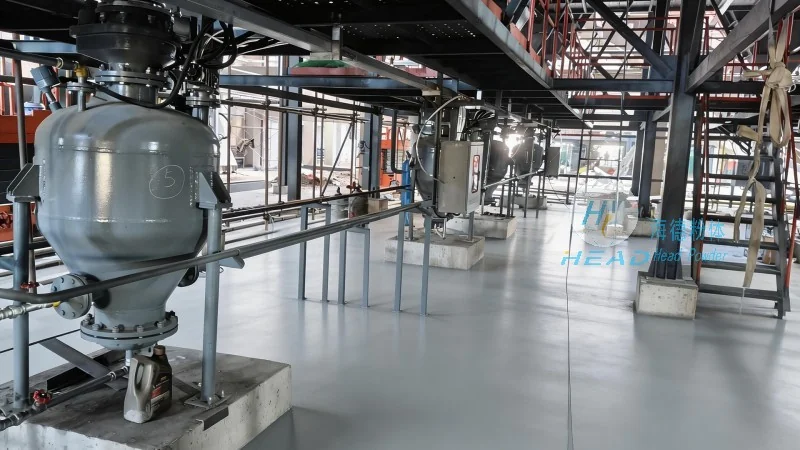
The Design Principles of Mineral Powder Material Handling Systems
The design of a mineral powder material handling system is a complex process that requires careful consideration of multiple factors to ensure optimal performance and safety. The primary design principles include material characterization, system integration, safety compliance, and cost optimization. First, material characterization is fundamental. Engineers must analyze the physical and chemical properties of the mineral powder, such as particle size distribution, density, moisture content, and flowability. This information is critical for selecting the appropriate equipment and determining the most effective conveying method. For instance, fine powders with high moisture content may require pneumatic conveying systems to prevent caking and blockages, while bulkier materials might be better suited for mechanical conveyors like belt or screw conveyors. Second, system integration is essential. A well-designed material handling system must seamlessly connect with other processes in the production line, such as crushing, grinding, and storage. This involves coordinating the flow of materials between equipment, ensuring that each stage operates efficiently without bottlenecks. For example, a feeder may need to supply a conveyor with a consistent flow rate, which is achieved through adjustable speed controls and level sensors. Third, safety is a non-negotiable design principle. Mineral powder handling systems are prone to dust explosions and material-related hazards, so the design must incorporate robust safety measures. These include explosion-proof components, dust collection systems, and emergency shutdown procedures. Additionally, regular maintenance and inspection protocols are integrated into the design to prevent equipment failure and ensure long-term reliability. Finally, cost optimization is a key consideration. The system should balance initial capital investment with long-term operational costs. This includes selecting energy-efficient equipment, minimizing maintenance requirements, and maximizing equipment lifespan. By adhering to these design principles, mineral powder handling systems can achieve high efficiency, low downtime, and enhanced safety, ultimately contributing to improved productivity and reduced operational costs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a reputable engineering firm specializing in mineral powder handling solutions. HeadPowder has established itself as a leading provider of customized material handling systems for the mining, chemical, and manufacturing industries. The company’s mission is to deliver innovative, reliable, and efficient solutions that meet the unique challenges of mineral powder processing. HeadPowder’s team of experienced engineers and technicians brings a wealth of knowledge and expertise to each project, ensuring that every system is tailored to the specific needs of the client. The company’s approach emphasizes collaboration with clients to understand their operational requirements and develop solutions that enhance productivity while minimizing risks. HeadPowder’s commitment to quality is reflected in its adherence to international standards and rigorous testing procedures for all equipment and systems. The company’s facilities in Shandong, China, are equipped with state-of-the-art technology and manufacturing capabilities, enabling the production of high-quality, durable equipment. HeadPowder serves clients both domestically and internationally, providing comprehensive support from system design and installation to maintenance and troubleshooting. With a focus on customer satisfaction and long-term partnerships, HeadPowder continues to be a trusted name in the mineral powder handling industry.