

What is a Sulfur Pellet Material Handling System? What Are Its Design Principles?
When it comes to efficiently transporting sulfur pellets, specialized systems are essential for optimizing industrial processes. The sulfur pellet material handling system is a critical component in various industries, particularly those involved in the production and distribution of sulfur-based products. This system is designed to ensure safe, reliable, and efficient movement of sulfur pellets from one location to another, supporting seamless operations in manufacturing and logistics.
Introduction to Sulfur Pellet Material Handling Systems
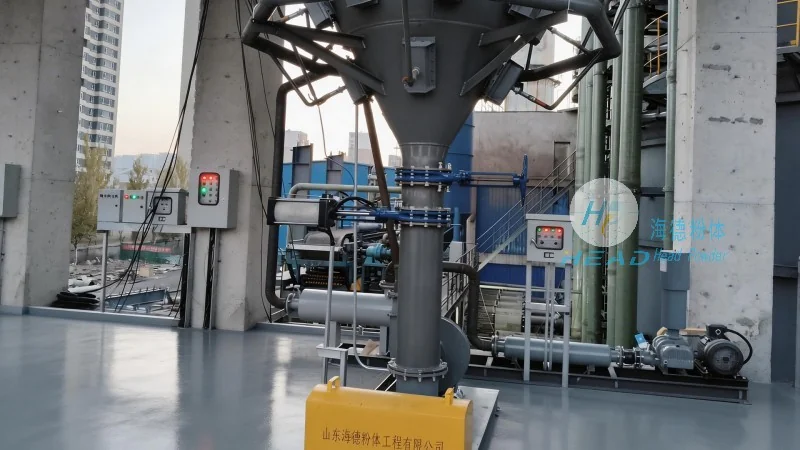
A sulfur pellet material handling system is a comprehensive setup that facilitates the transportation, storage, and processing of sulfur pellets. These systems are engineered to handle the unique properties of sulfur pellets, such as their density, moisture content, and potential reactivity. The primary goal of such a system is to enhance productivity while maintaining safety standards. By integrating various components like conveyors, storage silos, and control mechanisms, the system ensures that sulfur pellets are moved with minimal risk of spillage or damage.
Key Components and Design Principles of the System
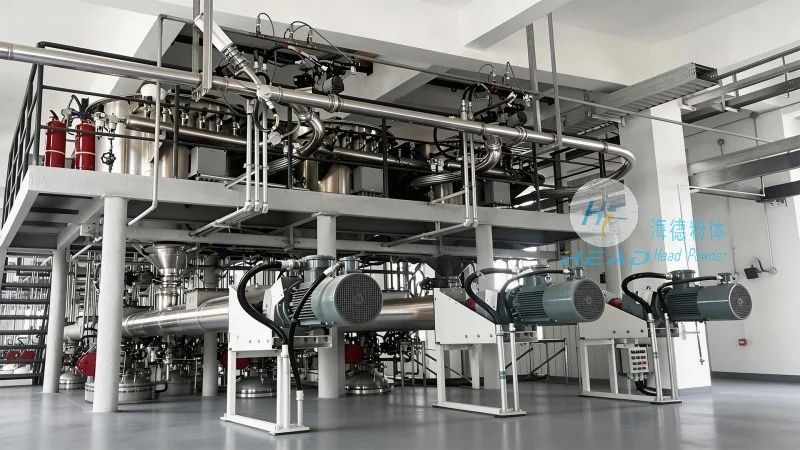
The design of a sulfur pellet material handling system is based on several fundamental principles to ensure optimal performance. Key components typically include bulk material handling equipment like belt conveyors, screw conveyors, and pneumatic conveyors. These components are selected based on the specific characteristics of the sulfur pellets, including their size, shape, and flowability. The system also incorporates storage solutions, such as silos or hoppers, to manage inventory levels and prevent material buildup. Additionally, control systems and safety features are integrated to monitor and regulate the flow of materials, ensuring operational efficiency and safety.
HeadPowder's Expertise in Engineering and Manufacturing
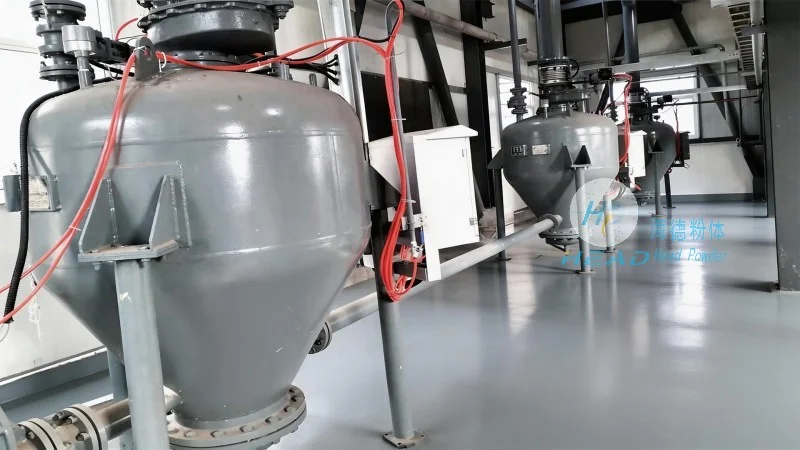
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of customized material handling solutions, specializing in the design and manufacturing of sulfur pellet material handling systems. With a strong commitment to quality and innovation, HeadPowder leverages advanced engineering techniques to develop systems tailored to the unique needs of its clients. The company's expertise spans the entire lifecycle of material handling, from initial design and planning to installation and maintenance. By working closely with clients, HeadPowder ensures that the final system meets all operational requirements and complies with industry standards.
Applications and Benefits of the Material Handling System
The sulfur pellet material handling system finds applications in various industries, including chemical manufacturing, mining, and energy production. In chemical plants, these systems are crucial for transporting sulfur pellets used in the production of sulfuric acid and other chemical products. In mining operations, they help in the handling of sulfur ore and pellets, facilitating the extraction and processing of raw materials. The benefits of using a well-designed material handling system include increased operational efficiency, reduced labor costs, and enhanced safety. By automating the movement of materials, the system minimizes human intervention, thereby reducing the risk of accidents and improving overall productivity.
Conclusion and Future Developments
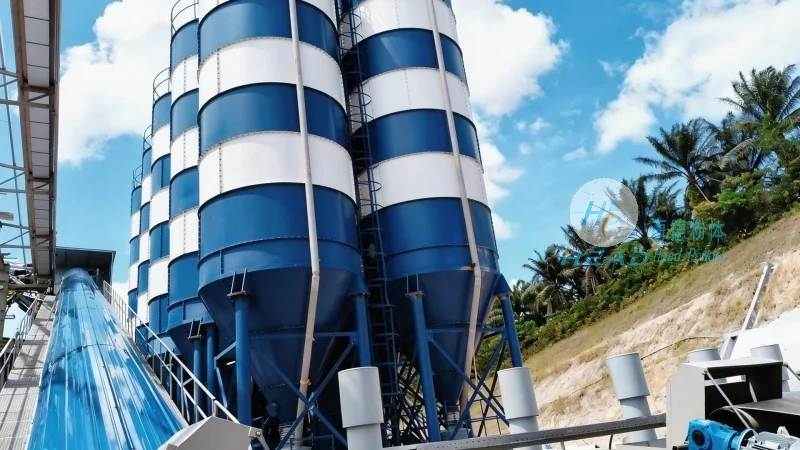
As industrial processes continue to evolve, the demand for efficient and reliable material handling systems remains high. The sulfur pellet material handling system, with its robust design and advanced features, plays a vital role in meeting these demands. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of developing innovative solutions that enhance operational performance and safety. With ongoing advancements in technology, future developments may include more automated and intelligent systems, further optimizing the handling of sulfur pellets and other bulk materials.