

What Are Intelligent Centralized Material Handling Equipment? And What Are Their Design Principles?
Intelligent centralized material handling equipment has become a crucial component in modern industrial operations, offering efficient and automated solutions for managing material flow within a facility. This equipment integrates advanced technologies to streamline processes, enhance productivity, and reduce operational costs. Understanding what these systems are and their underlying design principles is essential for businesses seeking to optimize their material handling strategies.
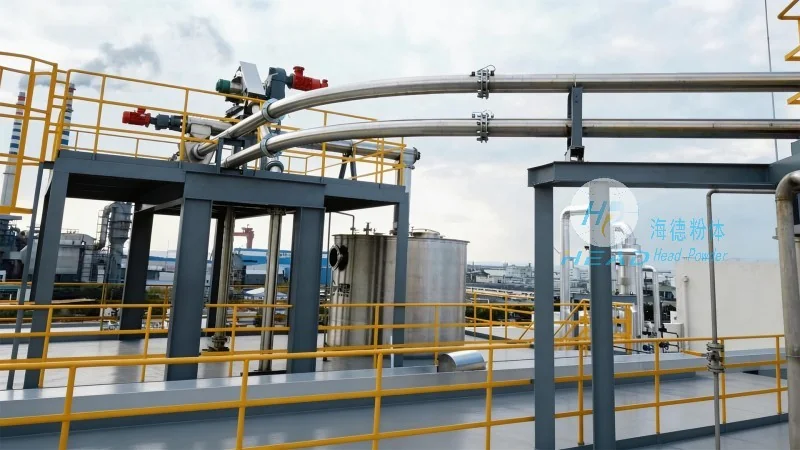
Understanding Intelligent Centralized Material Handling Equipment
Intelligent centralized material handling equipment refers to a suite of automated systems designed to consolidate, transport, and distribute materials from a central point to various workstations or storage areas within a production environment. These systems are typically equipped with sensors, control systems, and intelligent software that enable real-time monitoring and adaptive adjustments to changing operational demands. The primary goal is to minimize manual intervention, improve material flow efficiency, and ensure consistent performance across different production stages.
Key Components and Technologies
The design of intelligent centralized material handling equipment incorporates several critical components and technologies that work in synergy to achieve optimal functionality. These include automated guided vehicles (AGVs), conveyor systems, robotic arms, and advanced control software. Each component is engineered to handle specific material handling tasks, from picking and sorting to transporting and storing items. The integration of these technologies allows for seamless coordination and real-time data exchange, enabling the system to adapt to dynamic production requirements.
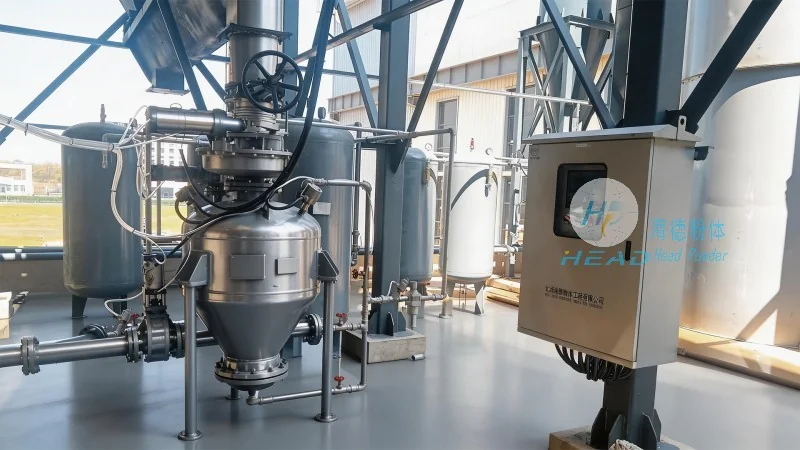
Design Principles for Efficient Material Handling
The design principles of intelligent centralized material handling equipment are centered on maximizing efficiency, flexibility, and reliability. Key principles include modularity, which allows for easy expansion or reconfiguration of the system to accommodate changing production needs. Another principle is scalability, enabling the equipment to handle varying volumes of materials without compromising performance. Additionally, the design emphasizes energy efficiency and low maintenance requirements, reducing long-term operational costs. The use of intelligent algorithms and predictive maintenance features further enhances the system's reliability and longevity.
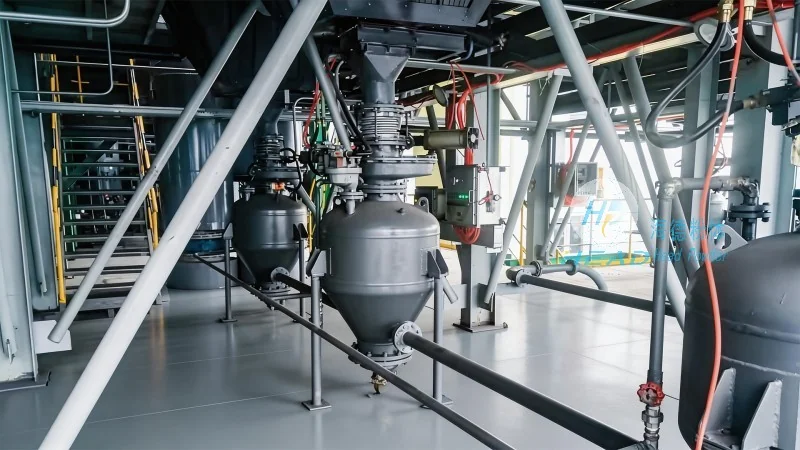
Applications in Industrial Settings
Intelligent centralized material handling equipment is widely used in various industrial sectors, including manufacturing, logistics, and warehousing. In manufacturing plants, these systems facilitate the smooth transfer of raw materials to production lines and finished products to storage or shipping areas. In logistics centers, they optimize the movement of packages and goods, reducing handling time and increasing throughput. The adaptability of these systems makes them suitable for diverse applications, from small-scale production environments to large-scale distribution centers.
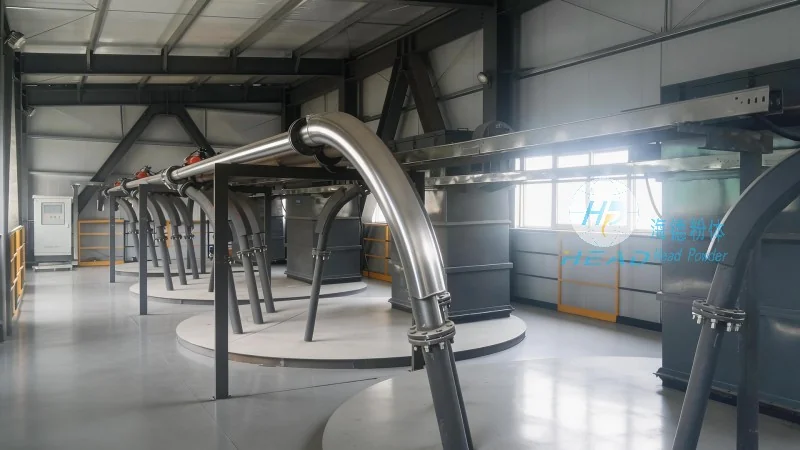
Benefits of Implementing Such Systems
Adopting intelligent centralized material handling equipment offers numerous benefits for businesses. These include significant reductions in labor costs, as the system minimizes the need for manual material handling. Enhanced productivity is another key advantage, as the equipment operates continuously and efficiently, reducing downtime and improving overall output. Improved safety is also a critical benefit, as the system reduces the risk of human error and workplace accidents. Furthermore, the integration of data analytics allows for better decision-making, enabling businesses to optimize their operations and improve profitability.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of intelligent material handling solutions. With a focus on innovation and customer-centric design, HeadPowder specializes in developing customized systems tailored to the unique needs of industrial clients. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing capabilities and technical expertise to deliver high-quality equipment. HeadPowder's commitment to excellence and continuous improvement ensures that its products meet the highest standards of performance and reliability, helping businesses achieve their operational goals effectively.