

What is a Potassium Fertilizer Material Handling System? And What Are Its Design Principles?
For agricultural operations, the efficient and safe transportation of potassium fertilizer is crucial for maintaining crop productivity and ensuring operational efficiency. A potassium fertilizer material handling system is a specialized set of equipment and processes designed to manage the movement, storage, and distribution of potassium-based fertilizers from production sites to application points. These systems are integral to modern agricultural practices, as they help optimize workflow, reduce material loss, and enhance overall operational safety.
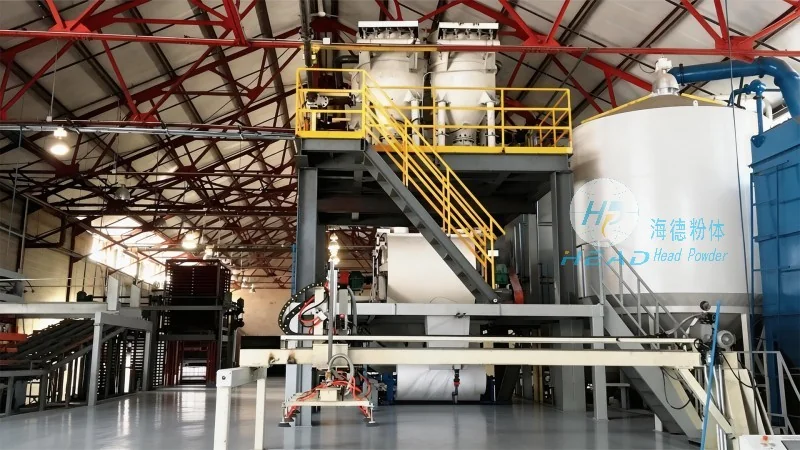
HeadPowder Engineering: A Leading Provider of Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., based in China, is a reputable company specializing in the design, manufacturing, and implementation of advanced material handling systems. With a focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner for agricultural and industrial clients seeking reliable fertilizer handling equipment. The company’s headquarters and operational base are located in Shandong, China, where it leverages local expertise and resources to deliver high-quality systems tailored to specific industry needs.
Key Components of a Potassium Fertilizer Material Handling System
A typical potassium fertilizer material handling system comprises several interconnected components that work in harmony to ensure smooth operation. The primary elements include bulk storage silos or hoppers, which are designed to hold large quantities of fertilizer while maintaining proper moisture and temperature levels. From these storage units, material is transferred to conveyor systems, such as belt conveyors or screw conveyors, which transport the fertilizer to processing or packaging areas. Control systems, often integrated with sensors and automation technology, monitor the flow of material, adjust conveyor speeds, and ensure that the system operates within safe parameters. Additionally, dust suppression and ventilation systems are incorporated to maintain air quality and prevent dust-related hazards, which is particularly important when handling fine potassium fertilizers.
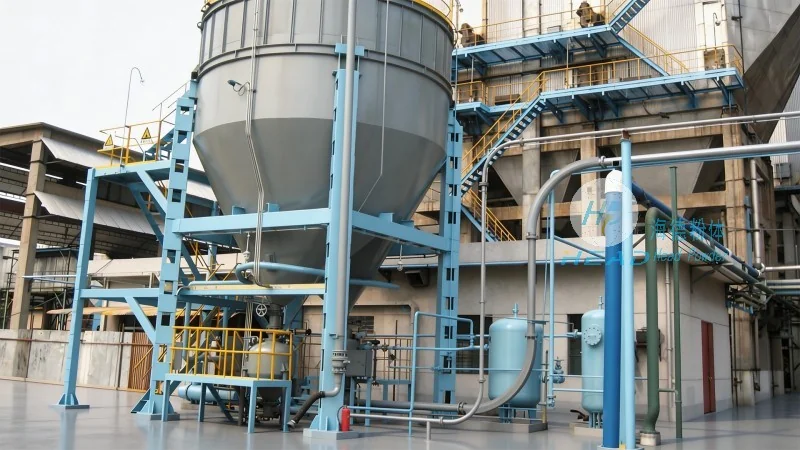
Design Principles for Optimal Performance
The design of a potassium fertilizer material handling system follows several key principles aimed at maximizing efficiency, safety, and durability. First, the system is engineered to handle the specific physical properties of potassium fertilizers, including their particle size, bulk density, and flow characteristics. This involves selecting appropriate equipment materials, such as corrosion-resistant stainless steel or specialized coatings, to prevent material buildup and ensure consistent flow. Second, the system prioritizes energy efficiency through the use of variable speed drives and optimized conveyor designs, reducing operational costs while minimizing environmental impact. Third, safety is a top priority, with features like emergency stop buttons, overload protection, and enclosed conveyor sections to prevent accidental exposure to the material. Finally, the system is designed for scalability, allowing for future expansion or integration with other agricultural technologies, such as precision application equipment.
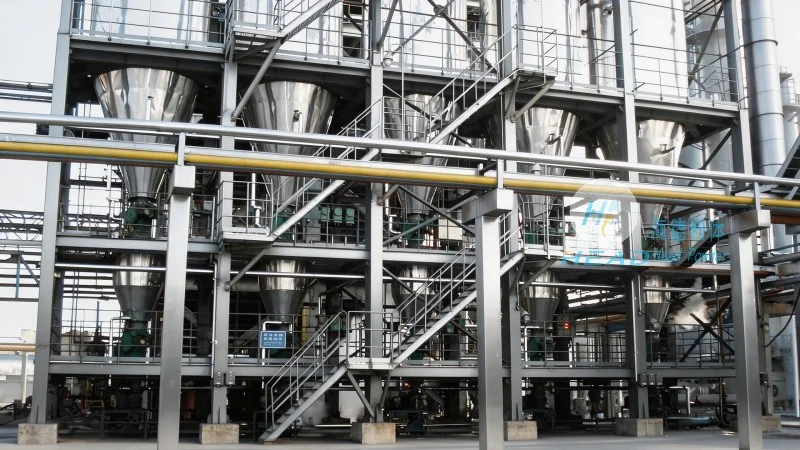
Benefits of Implementing a Potassium Fertilizer Material Handling System
Adopting a well-designed potassium fertilizer material handling system offers numerous benefits for agricultural businesses. By streamlining the transportation process, these systems reduce labor costs and improve operational speed, allowing farmers to apply fertilizers more efficiently and at optimal times. The reduction in material loss and spillage also contributes to cost savings and environmental sustainability. Furthermore, the automation and control features enhance safety for workers, minimizing the risk of accidents and exposure to harmful substances. For companies like HeadPowder, the implementation of such systems demonstrates a commitment to modern agricultural practices, aligning with global trends toward precision agriculture and sustainable resource management.
Conclusion: Choosing the Right Material Handling Solution
When selecting a potassium fertilizer material handling system, it is essential to consider the specific requirements of your operation, including the type of fertilizer, production volume, and application methods. Companies like Shandong HeadPowder Engineering Co., Ltd. offer comprehensive solutions that are tailored to meet these needs, combining advanced technology with expert engineering. By investing in a reliable material handling system, agricultural operations can enhance productivity, ensure safety, and contribute to the long-term sustainability of their farming practices. With a strong presence in China and a reputation for quality, HeadPowder continues to be a leading provider of material handling solutions for the global fertilizer industry.