

What is a Forage Storage Material Handling System Equipment? And What Are Its Design Principles?
Forage storage material handling systems are essential components in modern agricultural operations, designed to efficiently manage the storage and distribution of forage materials like silage or hay. These systems play a critical role in optimizing farm productivity by ensuring that feed is handled safely, hygienically, and with minimal waste. Understanding the equipment and its underlying design principles is crucial for farmers and agricultural professionals seeking to enhance their operations.
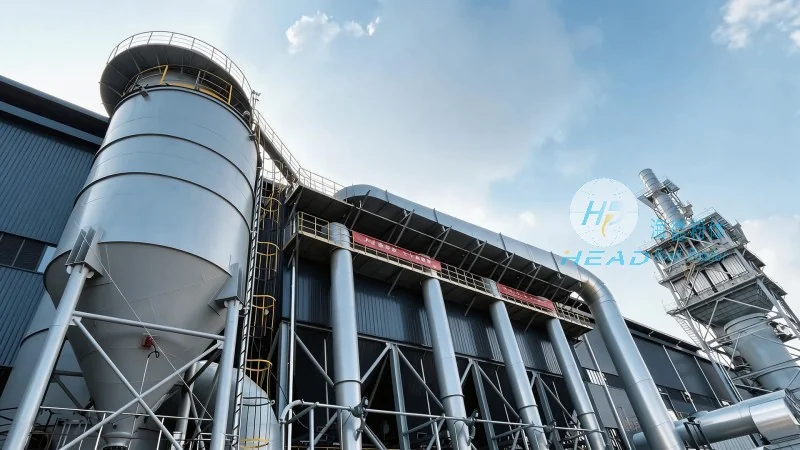
Key Components of the Forage Storage Material Handling System
The forage storage material handling system typically consists of several interconnected components that work in tandem to process and store forage materials. The primary components include:
- Conveyors: These are the backbone of the system, responsible for transporting forage from the field or storage area to the processing unit. Common types include belt conveyors, screw conveyors, and chain conveyors, each suited to different material characteristics and operational needs.
- Feeders and Distributors: After transport, feeders and distributors evenly distribute the forage into storage silos or bags. These components ensure uniform filling and prevent compaction, which is vital for maintaining the quality and nutritional value of the stored feed.
- Storage Silos or Bags: The storage vessels where processed forage is preserved. Modern systems often use large, airtight silos or flexible bags to minimize oxygen exposure and microbial growth, extending the shelf life of the feed.
- Control Systems: Advanced control systems manage the entire operation, from material intake to storage and distribution. These systems may include sensors for monitoring moisture levels, temperature, and fill levels, ensuring optimal conditions for feed preservation.
Design Principles and Operational Efficiency
The design of forage storage material handling systems is guided by several key principles aimed at maximizing efficiency and reliability. First, durability is a top priority, as the equipment must withstand harsh farm environments and heavy usage. Materials such as stainless steel and robust polymers are commonly used to ensure longevity and resistance to corrosion and wear.
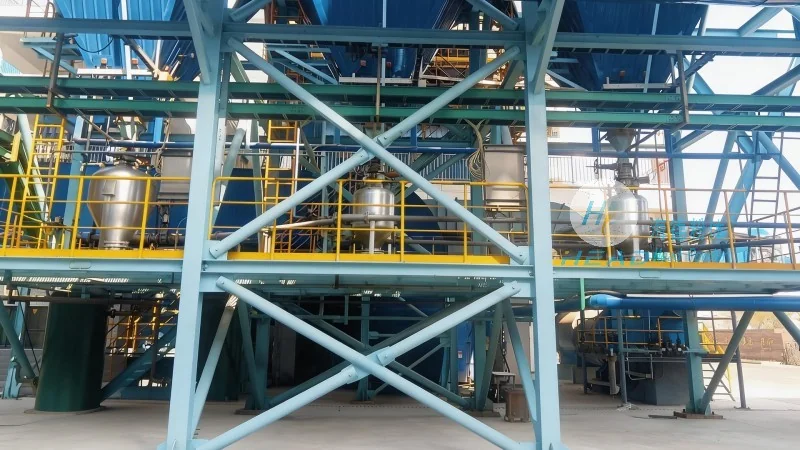
Second, energy efficiency is a critical consideration. Modern systems incorporate energy-saving features like variable speed drives and optimized conveyor designs to reduce power consumption without compromising performance. This not only lowers operational costs but also aligns with sustainable farming practices.
Third, ease of maintenance is incorporated into the design. Modular components and accessible maintenance points allow for quick repairs and routine checks, minimizing downtime and keeping the system operational year-round. Additionally, user-friendly interfaces on control panels simplify operation for farm staff, reducing the need for specialized training.
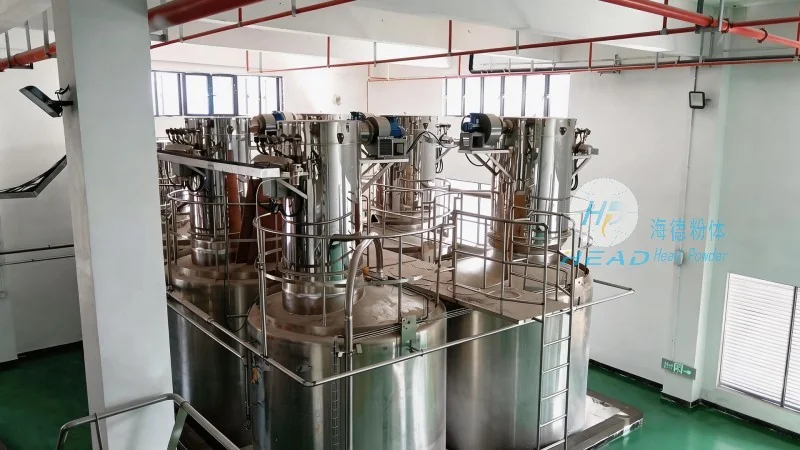
Application Scenarios and Industry Relevance
Forage storage material handling systems are widely used in various agricultural settings, particularly in dairy and livestock operations where consistent feed supply is essential for animal health and productivity. The equipment is also valuable in feed production facilities, where it streamlines the process of preparing and storing feed for sale or distribution.
In dairy farms, for example, these systems help manage large volumes of silage, ensuring that cows receive high-quality feed throughout the year. In livestock operations, the systems can handle a range of forage types, from grass to alfalfa, adapting to different animal needs. The ability to store feed for extended periods also supports year-round feeding, reducing the impact of seasonal variations in forage availability.
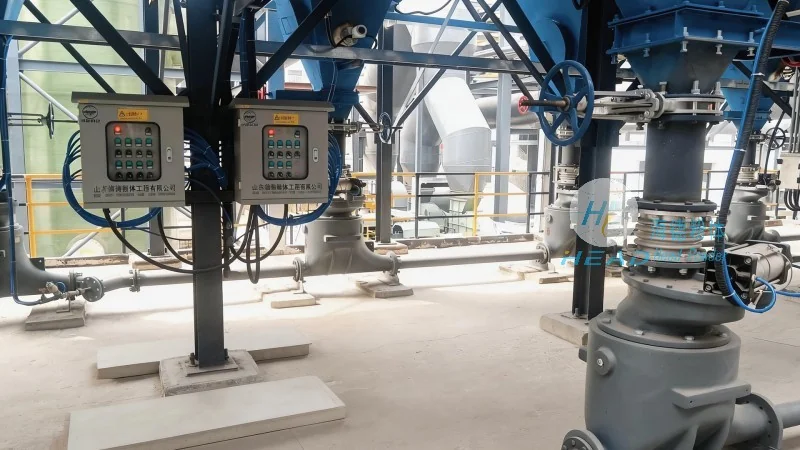
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of forage storage material handling systems. With a strong commitment to quality and innovation, the company has established itself as a trusted provider in the agricultural machinery sector. HeadPowder's products are engineered to meet the specific needs of modern farming, combining durability, efficiency, and user-friendly features.
Located in Shandong, China, HeadPowder leverages advanced manufacturing techniques and rigorous quality control processes to deliver reliable equipment that enhances farm operations. The company's expertise in material handling technology ensures that its systems are tailored to the unique challenges of forage storage and distribution, providing farmers with solutions that improve productivity and profitability.