

Working Principle and Features of Positive Pressure Dilute Phase Powder Conveyors
Positive pressure dilute phase powder conveyors are advanced industrial equipment designed for the efficient and reliable transportation of bulk powders over long distances. Unlike traditional dense phase or pneumatic conveying systems, these machines operate by maintaining a positive pressure within the conveying line, ensuring that the powder is continuously propelled forward through a mixture of air and solid particles. The "dilute phase" characteristic refers to the relatively low concentration of powder in the air stream, which allows for high velocity and reduced pressure drop, making them suitable for various applications in industries such as food processing, pharmaceuticals, chemicals, and minerals.
Working Principle of Positive Pressure Dilute Phase Powder Conveyors
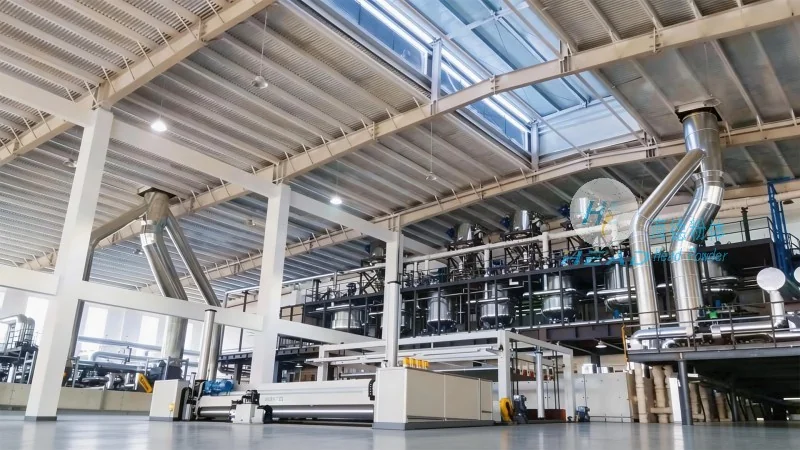
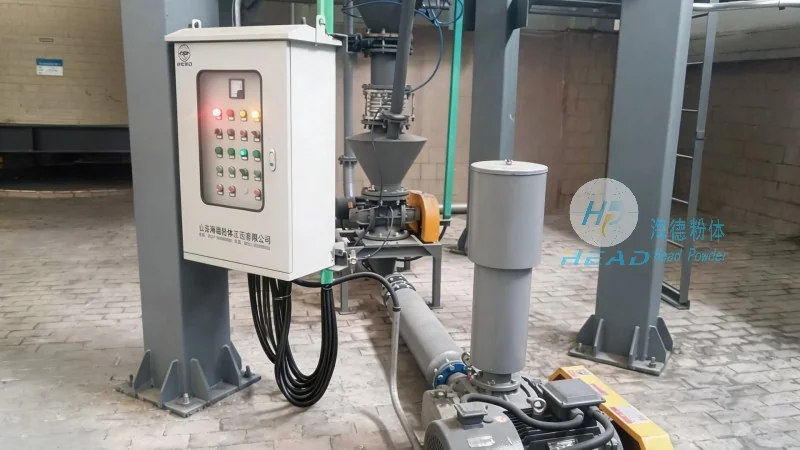
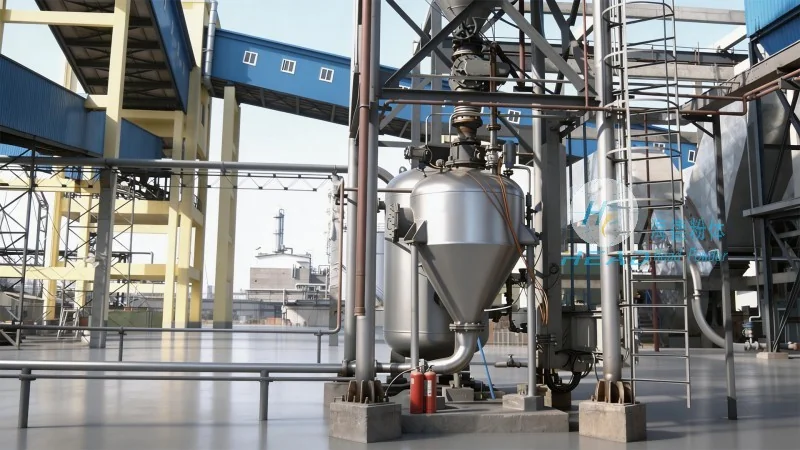
The operation of a positive pressure dilute phase powder conveyor is based on the principle of air pressure and particle suspension. The system typically consists of a blower or compressor that generates a high-pressure air flow, which is then introduced into the conveying line at the inlet. As the air flows through the pipe, it picks up the powder from the hopper or storage silo and carries it to the discharge point. The positive pressure ensures that the air and powder mixture remains in a continuous flow, preventing blockages and ensuring consistent material transport. The design often includes features such as pulse valves, which intermittently increase the air pressure to maintain the flow and prevent material settling in the line. Additionally, the system may incorporate filters and cyclones to separate the powder from the air at the discharge end, allowing for clean air release and powder recovery.
Key Features and Advantages of Positive Pressure Dilute Phase Powder Conveyors
Positive pressure dilute phase powder conveyors offer several distinct advantages that make them a preferred choice for many industrial applications. One of the primary benefits is their high conveying efficiency, as the positive pressure and high velocity of the air stream enable the transport of large quantities of powder over long distances with minimal energy consumption. The dilute phase operation also reduces the risk of material degradation or caking, as the particles are kept in suspension and do not come into direct contact with each other or the pipe walls. Another key feature is the flexibility in material handling, as these systems can accommodate a wide range of powder types, including fine powders, granules, and even sticky or cohesive materials, provided they are properly pre-treated. The positive pressure design also ensures that the conveying line remains sealed, preventing dust emissions and maintaining a clean working environment. Furthermore, the system's modular construction allows for easy integration into existing production lines and can be customized to meet specific operational requirements, such as varying flow rates or material types.
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-quality powder handling equipment, including positive pressure dilute phase powder conveyors. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry, providing reliable and efficient solutions for bulk material transportation. The company is headquartered in Shandong, China, and leverages advanced engineering and manufacturing capabilities to deliver products that meet international standards and customer specifications. HeadPowder's team of experienced engineers and technicians works closely with clients to understand their unique needs and develop tailored solutions that enhance operational efficiency and reduce costs. By combining cutting-edge technology with rigorous quality control, HeadPowder ensures that its products are durable, reliable, and perform optimally in various industrial environments.
Conclusion
In summary, positive pressure dilute phase powder conveyors are an essential component of modern industrial powder handling systems, offering efficient, flexible, and reliable solutions for transporting bulk materials. The working principle, which relies on positive pressure and dilute phase air flow, enables high throughput and minimal material degradation. The key features of these systems, including high efficiency, flexibility, and environmental benefits, make them suitable for a wide range of applications. As a leading manufacturer, HeadPowder Engineering Co., Ltd. continues to provide advanced powder conveying solutions that meet the evolving needs of industries worldwide, ensuring safe and effective material transport in various sectors.