

Working Principle and Features of High-Calcium Powder Conveyors
High-calcium powder conveyors are essential equipment in industries dealing with calcium-rich powders, such as cement, calcium carbonate, and other mineral powders. These conveyors are designed to efficiently transport bulk materials while maintaining product integrity and minimizing dust generation. Understanding the working principle and key features of high-calcium powder conveyors is crucial for optimizing material handling processes and ensuring operational efficiency.
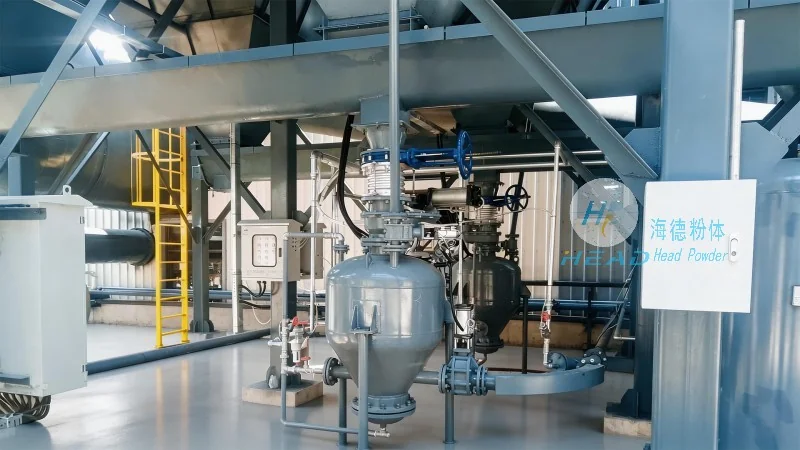
Company Introduction
HeadPowder, a leading manufacturer in the field of powder handling equipment, specializes in developing advanced solutions for high-calcium powder conveyors. With years of experience and a commitment to innovation, HeadPowder provides reliable and efficient equipment tailored to the specific needs of various industrial applications. The company is headquartered in Shandong, China, and has established a strong reputation for quality and performance in the global market.
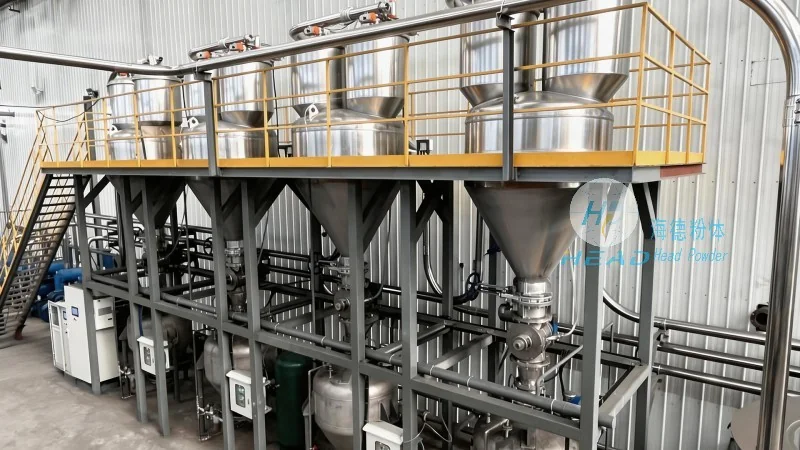
Working Principle of High-Calcium Powder Conveyors
The working principle of high-calcium powder conveyors typically involves a combination of mechanical components that work in tandem to move powders from the source to the destination. The primary mechanism often includes a conveyor belt or screw that transports the material through a sealed system, reducing dust exposure and ensuring consistent flow. For high-calcium powders, which can be abrasive and prone to caking, the design incorporates features like adjustable speed controls, anti-static measures, and material-specific wear-resistant components to enhance durability and performance. The conveyor system may also include a hopper or feeder at the inlet to regulate the flow rate, preventing overloading and maintaining smooth operation. At the discharge end, a control valve or outlet mechanism allows for precise material release, enabling accurate dosing and integration with downstream processes. The entire system operates under controlled conditions, with temperature and humidity monitoring to preserve the quality of the high-calcium powder during transport.
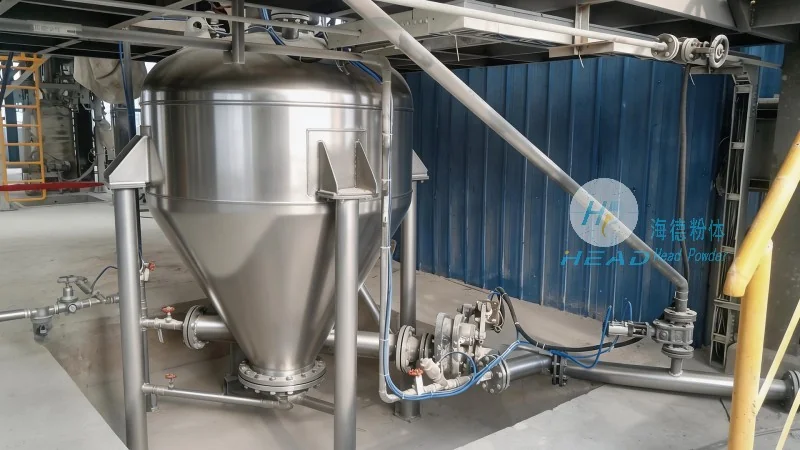
Key Features of High-Calcium Powder Conveyors
High-calcium powder conveyors from HeadPowder are equipped with several key features that distinguish them in the market. One of the most notable features is the robust construction, which includes stainless steel or corrosion-resistant materials to withstand the abrasive nature of high-calcium powders. This ensures long service life and minimal maintenance requirements. The conveyors also feature adjustable speed and flow control, allowing operators to optimize the transport rate based on production needs and material characteristics. Anti-static and dust suppression systems are integrated to comply with safety regulations and maintain a clean working environment. Additionally, the design incorporates easy access points for maintenance, such as removable panels and quick-release components, reducing downtime and operational costs. The sealed housing design minimizes dust emissions, making these conveyors suitable for applications where environmental compliance is critical. Furthermore, the conveyors are equipped with sensors and monitoring systems to detect blockages or malfunctions, providing real-time feedback and enhancing overall system reliability.
Applications and Benefits
High-calcium powder conveyors are widely used in various industries, including cement manufacturing, chemical processing, and food production. In cement plants, they are used to transport raw materials like limestone and calcium carbonate, which are essential for clinker production. The efficient handling of these materials improves production throughput and reduces energy consumption. In the chemical industry, the conveyors are used to transport calcium-based chemicals, ensuring precise dosing and preventing contamination. The benefits of using high-calcium powder conveyors extend beyond efficiency; they also contribute to improved product quality by maintaining the purity and consistency of the powder. The reduced dust generation and contamination also enhance the safety of the working environment, minimizing health risks for operators. Furthermore, the advanced control systems allow for seamless integration with other processing equipment, creating a streamlined production line that enhances overall operational efficiency.
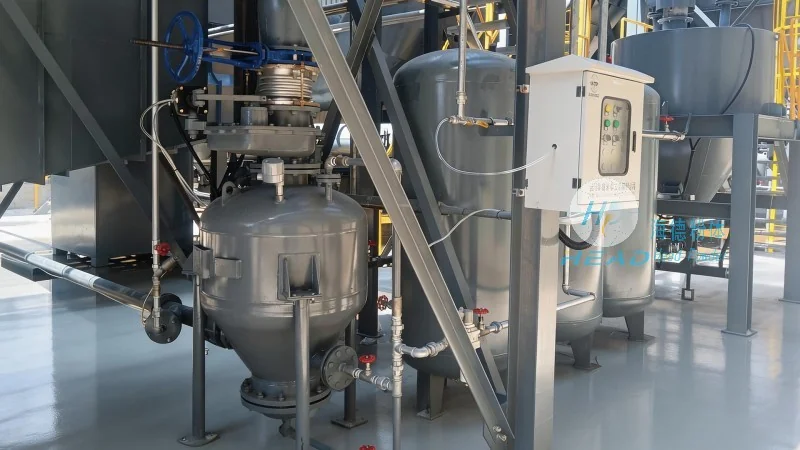
Conclusion
High-calcium powder conveyors are critical equipment for industries dealing with calcium-rich powders, offering efficient and reliable material handling solutions. The working principle, which combines mechanical transport with advanced control systems, ensures consistent performance and minimal downtime. The key features, including robust construction, adjustable flow control, and dust suppression, make these conveyors suitable for demanding applications. HeadPowder, with its expertise and commitment to quality, provides high-performance high-calcium powder conveyors that meet the needs of various industrial sectors. By investing in such equipment, companies can enhance their production efficiency, improve product quality, and ensure compliance with safety and environmental regulations.