

Working Principle and Features of Ammonia Fertilizer Powder Conveyors
Ammonia fertilizer powder conveyors are essential equipment in the agricultural and chemical industries, designed to efficiently transport bulk ammonia-based fertilizer powders from storage to processing or application points. These systems are engineered to handle the unique properties of ammonia fertilizers, which include high reactivity, hygroscopic nature, and the need for precise control during handling. The primary function of such conveyors is to ensure safe, reliable, and efficient movement of these powders, minimizing dust generation and preventing material degradation.
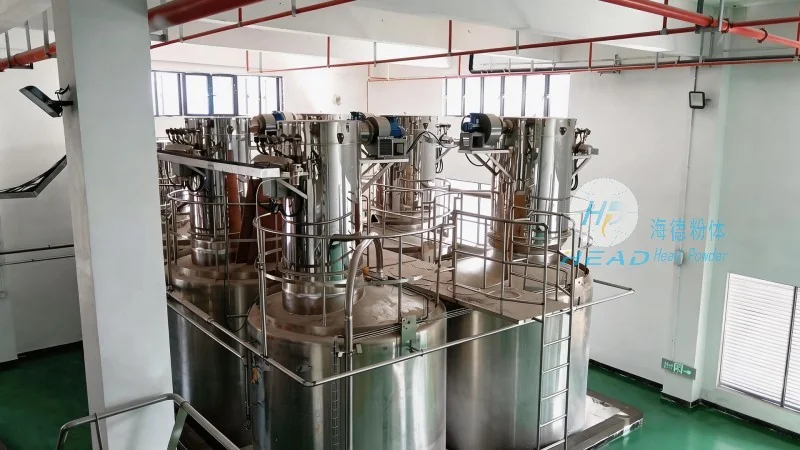
Working Principle of Ammonia Fertilizer Powder Conveyors
The working principle of ammonia fertilizer powder conveyors typically involves a combination of mechanical components that work in tandem to move the material. A common design includes a hopper or feed bin where the fertilizer is stored, equipped with a feeding mechanism such as a rotary valve or screw feeder to control the flow rate. The material then enters a conveyor section, which may be a pneumatic system (air-suspended or air-blast) or a mechanical system like a belt or screw conveyor. Pneumatic conveyors use compressed air to transport the powder through a pipeline, while mechanical conveyors rely on rotating components to push the material forward. The system is often equipped with pressure regulators, filters, and dust collection units to maintain air quality and prevent contamination. The control system monitors parameters like pressure, flow rate, and temperature to ensure optimal operation and prevent overloading or blockages.
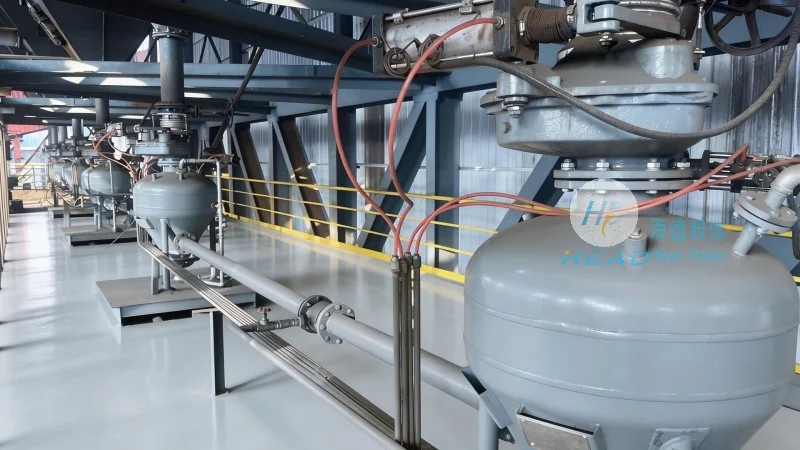
Key Features of Ammonia Fertilizer Powder Conveyors
Ammonia fertilizer powder conveyors from Shandong HeadPowder Engineering Co., Ltd. are characterized by several key features that enhance performance and safety. One of the primary features is the use of corrosion-resistant materials, such as stainless steel or specialized alloys, to withstand the chemical properties of ammonia fertilizers and prevent material degradation or equipment failure. The design incorporates dust suppression mechanisms, including sealed hoppers and enclosed conveyor lines, to minimize dust emissions and comply with environmental regulations. Additionally, the systems are equipped with advanced control technologies, such as PLC (Programmable Logic Controller) systems, which allow for precise control of flow rates, pressure, and other operational parameters. This ensures consistent and reliable performance, reducing downtime and maintenance costs. The conveyors also feature easy-to-clean designs, with smooth surfaces and removable components, facilitating regular maintenance and sanitation to prevent contamination. Safety features, including emergency shut-off valves and pressure relief systems, are integrated to protect operators and the environment from potential hazards.
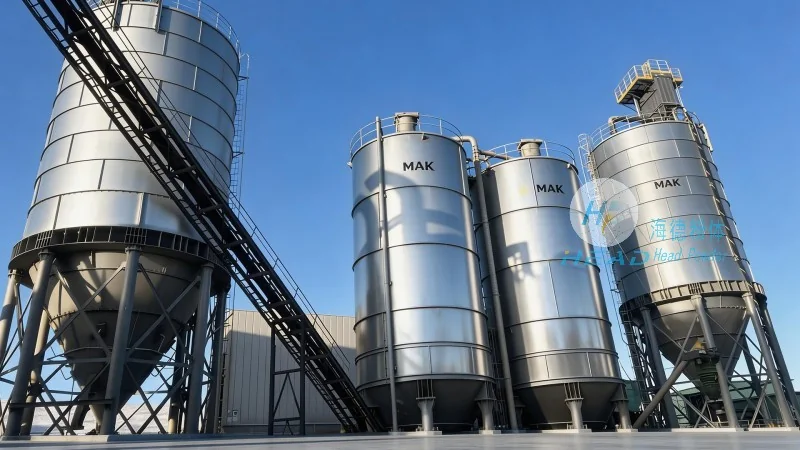
Application and Benefits in Fertilizer Handling
Ammonia fertilizer powder conveyors are widely used in fertilizer production and distribution facilities, where they play a critical role in the efficient handling of bulk ammonia-based fertilizers. The benefits of these systems include improved productivity through reduced handling time and increased throughput, as well as enhanced safety by minimizing manual handling of hazardous materials. The systems also contribute to cost savings by reducing material loss due to dust and spillage, and by optimizing energy consumption through efficient operation. In addition, the precise control capabilities of the conveyors help maintain consistent product quality, ensuring that the fertilizer meets the required specifications for agricultural use. The reliability of these systems is further enhanced by the use of durable components and regular maintenance, which minimizes breakdowns and extends the lifespan of the equipment.
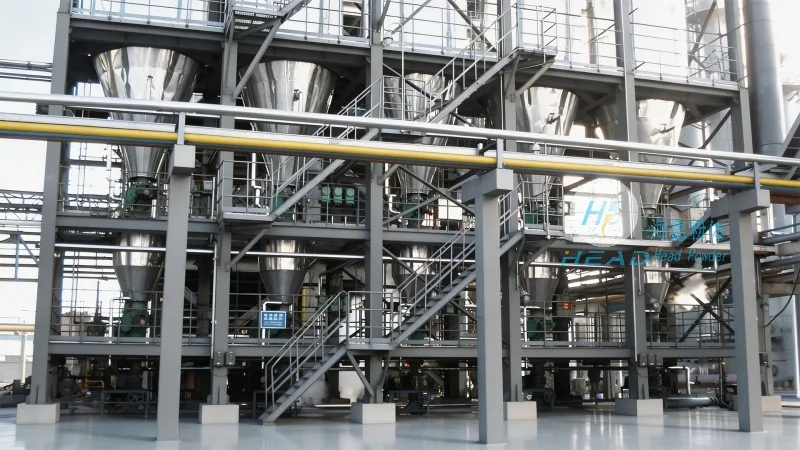
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of specialized powder handling equipment, including ammonia fertilizer powder conveyors. The company is headquartered in Shandong, China, and has a strong reputation for producing high-quality, reliable equipment tailored to the specific needs of the agricultural and chemical industries. With years of experience in the field, headpowder has developed a deep understanding of the challenges associated with handling ammonia fertilizers and has engineered solutions that address these challenges effectively. The company's commitment to innovation and quality has led to the development of advanced conveyor systems that meet the highest standards of performance and safety. Headpowder's products are designed to be durable, efficient, and easy to maintain, providing long-term value to customers in the fertilizer industry.