

Working Principle and Features of Ammonium Bicarbonate Powder Conveyors
Ammonium bicarbonate is a widely used chemical in various industrial applications, and efficient handling of this powder is crucial for maintaining production efficiency and product quality. The Ammonium Bicarbonate Powder Conveyor, manufactured by Shandong HeadPowder Engineering Co., Ltd., is a specialized equipment designed to address the unique challenges associated with transporting this specific chemical. This article explores the working principle and key features of this conveyor system, providing insights into how it enhances operational performance in industrial settings.
Working Principle of the Ammonium Bicarbonate Powder Conveyor
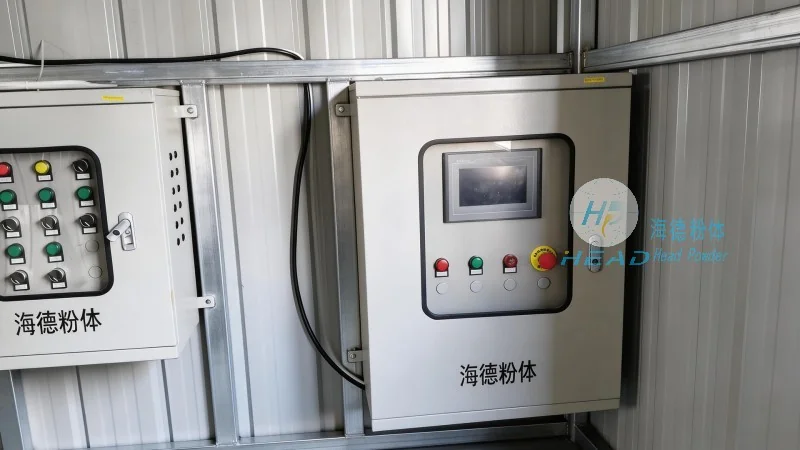
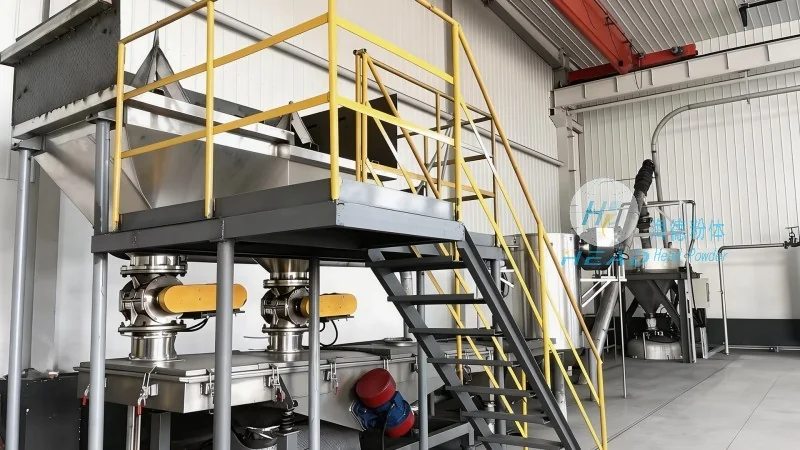
The Ammonium Bicarbonate Powder Conveyor operates on a principle of continuous material handling, utilizing a combination of mechanical components to ensure reliable and efficient transport of the powder. The system typically consists of a hopper for material storage, a conveyor belt or screw mechanism for movement, and a discharge mechanism for delivering the material to the next stage of processing. The hopper is designed to accommodate the bulk storage of ammonium bicarbonate, ensuring a consistent feed to the conveyor. The conveyor mechanism, which may vary in design depending on the specific application, is engineered to handle the low bulk density and potential caking properties of ammonium bicarbonate. By using a low-speed, high-torque drive system, the conveyor minimizes the risk of material degradation or blockage, which are common issues with traditional high-speed conveyors. The discharge section is equipped with a controlled outlet to regulate the flow rate, preventing overloading of downstream equipment and maintaining a stable processing environment. The entire system is integrated with sensors and control panels to monitor operational parameters such as flow rate, pressure, and temperature, ensuring optimal performance and safety. This closed-loop control system allows for real-time adjustments to maintain consistent material handling, which is critical for processes that require precise dosing or continuous operation.
Key Features of the Ammonium Bicarbonate Powder Conveyor
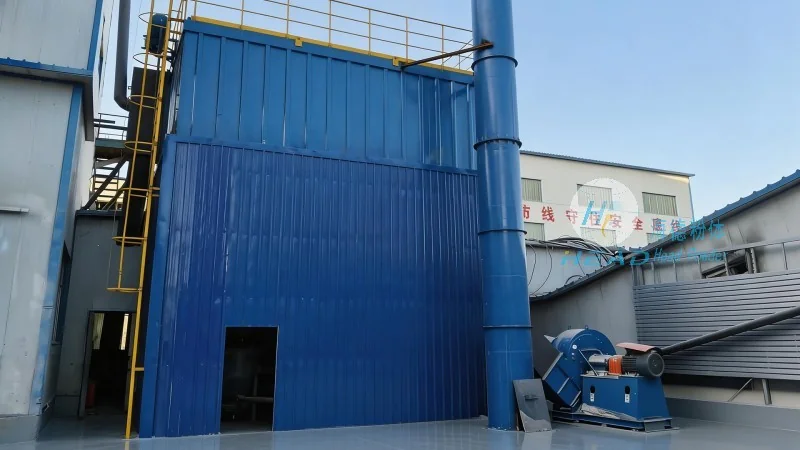
Shandong HeadPowder Engineering Co., Ltd. has incorporated several advanced features into the Ammonium Bicarbonate Powder Conveyor to enhance its functionality and durability. One of the primary features is the use of corrosion-resistant materials, particularly in areas that come into direct contact with the ammonium bicarbonate. The conveyor components are made from stainless steel or specialized alloys that resist chemical attack, ensuring long-term reliability and minimizing maintenance requirements. Another significant feature is the dust control system, which includes sealed housing and air filtration to prevent the release of fine particles into the environment. This not only improves workplace safety but also complies with environmental regulations. The conveyor is also equipped with a self-cleaning mechanism, which helps to prevent material buildup and clogging, especially in areas prone to caking. This feature reduces downtime and increases the overall efficiency of the system. Additionally, the system is designed for easy maintenance, with accessible components and modular design that allows for quick replacement of parts. The control system is user-friendly, with intuitive interfaces that enable operators to monitor and adjust settings without extensive training. This enhances operational flexibility and reduces the learning curve for new personnel. The conveyor also features energy-efficient motors, which help to reduce operational costs while maintaining high performance. By optimizing power consumption, the system contributes to lower energy bills and a more sustainable operation. The robust construction of the conveyor ensures it can withstand the rigors of continuous industrial use, with a design that minimizes wear and tear from frequent operation. This durability is essential for maintaining consistent performance over extended periods, which is critical for long-term operational success.
Application and Operational Benefits
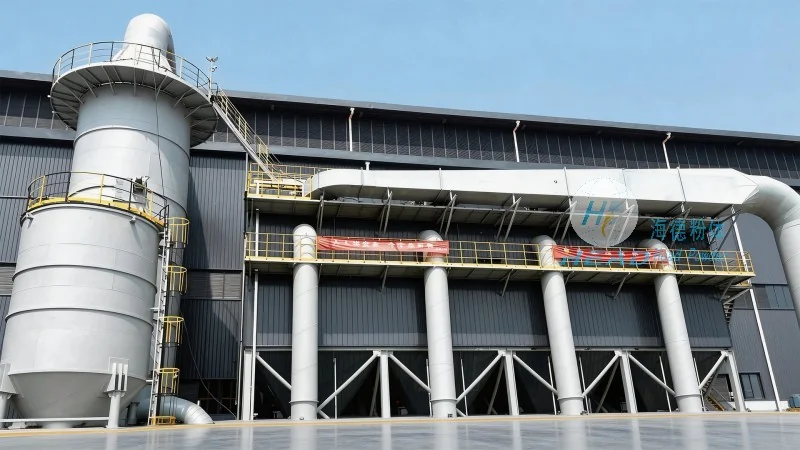
The Ammonium Bicarbonate Powder Conveyor is widely used in industries such as food processing, pharmaceuticals, and chemical manufacturing, where the handling of ammonium bicarbonate is essential. In food processing, it is used for the transport of baking powders and other leavening agents, ensuring consistent quality and dosing. In pharmaceutical applications, the conveyor is used to handle raw materials and intermediates, maintaining the purity and integrity of the products. The chemical industry also benefits from this equipment, as it facilitates the transport of ammonium bicarbonate in production lines for fertilizers and other chemical products. The operational benefits of using this conveyor include improved process efficiency, reduced material loss, and enhanced safety. By minimizing the risk of material degradation and clogging, the system ensures a consistent flow rate, which is crucial for maintaining production schedules and meeting quality standards. The dust control features also contribute to a safer working environment, reducing the risk of respiratory issues and other health hazards associated with fine powder handling. Additionally, the energy-efficient design helps to lower operational costs, making the equipment a cost-effective solution for industrial applications. The durability of the conveyor ensures a long service life, reducing the need for frequent replacements and associated maintenance costs. Overall, the Ammonium Bicarbonate Powder Conveyor from Shandong HeadPowder Engineering Co., Ltd. provides a reliable and efficient solution for handling ammonium bicarbonate, enhancing operational performance and contributing to the success of industrial processes.