

Working Principle and Features of Coal Particle Material Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of material handling technology, specializes in the design, manufacturing, and supply of advanced coal particle conveying systems. With a focus on innovation and precision engineering, the company has established itself as a trusted partner for industries requiring efficient and reliable transportation of bulk materials. HeadPowder's solutions are tailored to meet the specific needs of clients, ensuring optimal performance and durability in demanding operational environments. The company's headquarters is located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services.
Understanding the Working Principle of Coal Particle Conveying Systems
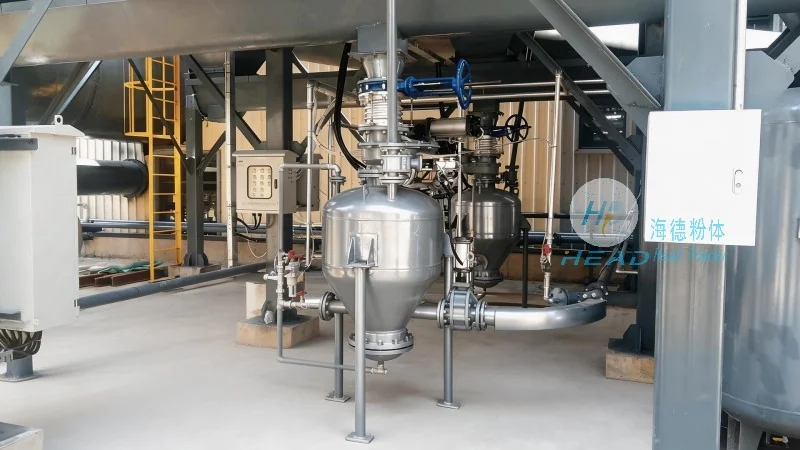
Coal particle conveying systems are engineered to transport bulk coal efficiently from one location to another within industrial facilities or between different processing stages. The core working principle involves the use of specialized equipment such as belt conveyors, screw conveyors, or pneumatic conveyors, which are designed to handle the physical properties of coal particles—such as size, density, and moisture content. The system typically operates by feeding coal into the conveyor inlet, where it is then moved along the conveyor path through mechanical or pneumatic forces. For belt conveyors, a motor-driven pulley system pulls the belt, which carries the coal along its length. Screw conveyors utilize a rotating screw to push the coal forward, while pneumatic conveyors use air pressure to transport the material through a pipeline. Each component of the system is carefully designed to ensure smooth material flow, minimal loss, and consistent performance. The working principle emphasizes the integration of mechanical efficiency with material compatibility, allowing for the reliable transfer of coal in various industrial applications.
Key Features of Coal Particle Material Conveying Systems
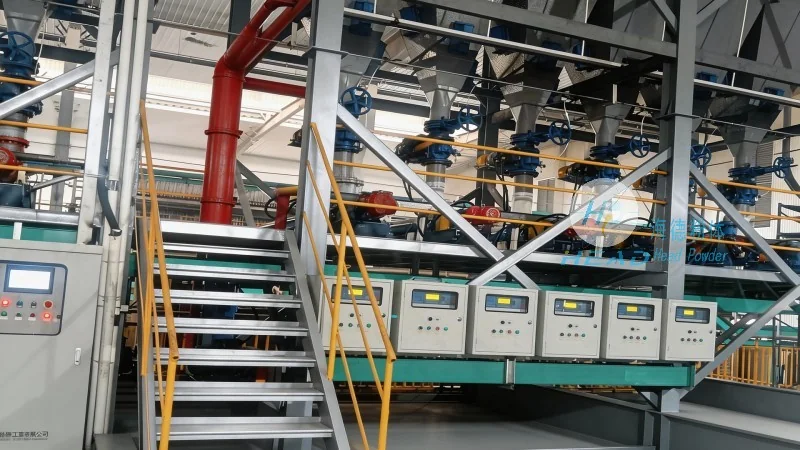
HeadPowder's coal particle conveying systems are distinguished by several key features that enhance their performance and adaptability. Firstly, the systems are constructed with robust materials, such as high-strength steel and corrosion-resistant coatings, to withstand the harsh conditions of coal handling, including abrasion, moisture, and temperature fluctuations. This durability ensures long service life and minimal maintenance requirements, reducing operational costs for clients. Secondly, the conveyors are equipped with advanced control systems that allow for precise regulation of speed, flow rate, and direction, enabling seamless integration with other processing equipment. These controls enhance operational flexibility and allow for real-time adjustments based on production demands. Thirdly, the systems incorporate safety features, including overload protection, emergency stop mechanisms, and monitoring sensors, to ensure safe and reliable operation. Additionally, the design of the conveyors prioritizes energy efficiency, with optimized motor drives and reduced friction to minimize power consumption. The combination of these features makes HeadPowder's coal particle conveying systems not only effective but also cost-effective and environmentally friendly.
Advantages and Applications in Industrial Settings
The coal particle conveying systems offered by Shandong HeadPowder Engineering Co., Ltd. provide significant advantages for industries involved in coal processing, power generation, and mining. These systems are particularly effective in applications where large volumes of coal need to be transported over long distances or through complex layouts. For example, in power plants, the systems efficiently move coal from storage silos to boilers, ensuring a steady supply of fuel for energy production. In mining operations, the conveyors transport mined coal from the extraction site to processing facilities, streamlining the overall production process. The systems also support the integration of automated material handling, allowing for the seamless connection of different processing stages and reducing manual labor requirements. Furthermore, the systems are designed to handle a wide range of coal types, from low-grade to high-grade varieties, making them versatile for various industrial needs. The reliability and efficiency of HeadPowder's coal particle conveying systems contribute to improved productivity, reduced downtime, and enhanced safety in industrial environments.
Conclusion and Company Commitment
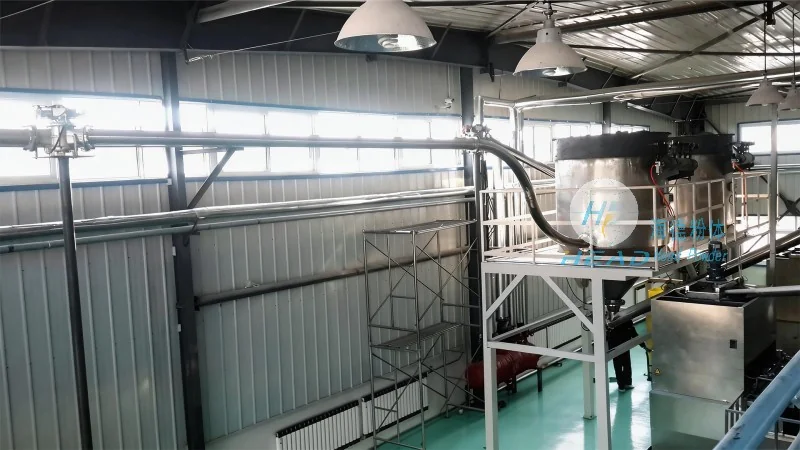
Shandong HeadPowder Engineering Co., Ltd. continues to innovate in the development of coal particle material conveying systems, focusing on delivering solutions that meet the evolving needs of the industry. By combining advanced engineering, robust construction, and user-friendly controls, the company ensures that its products deliver superior performance and durability. The systems are designed to adapt to changing operational requirements while maintaining high standards of safety and efficiency. As a leading provider in the field, HeadPowder is committed to supporting its clients with reliable, cost-effective solutions that enhance their operational capabilities. With its headquarters in Shandong, China, the company leverages local expertise and resources to provide comprehensive support, including installation, maintenance, and technical assistance. The commitment to quality and customer satisfaction has made HeadPowder a trusted name in the material handling industry, offering coal particle conveying systems that are both effective and sustainable for the future.