

Working Principle and Features of Dry Stone Powder Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced material handling solutions for industries dealing with dry stone powders. The company's core product, the dry stone powder material handling system, is designed to efficiently transport and manage these materials with precision and reliability. This system is crucial for applications in construction, mining, and other sectors where consistent material flow is essential.
Working Principle of the Dry Stone Powder Material Handling System
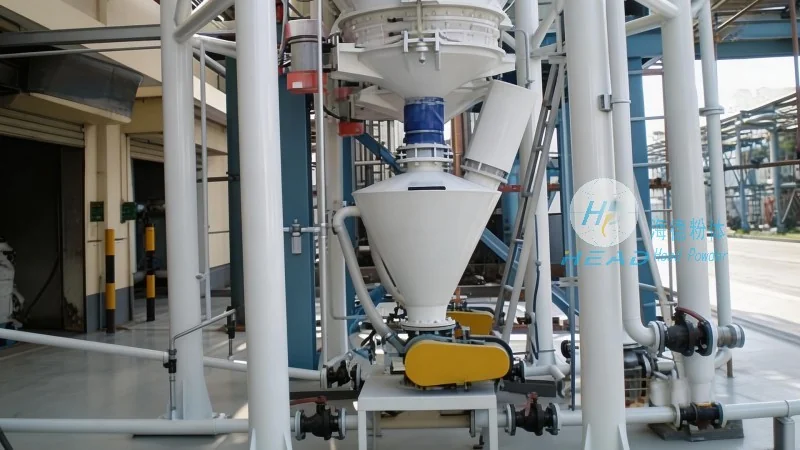
The system operates on a combination of mechanical and pneumatic principles to ensure smooth material transport. At its core, the equipment uses a series of conveyor belts, hoppers, and airlocks to move dry stone powders from the source to the destination. The process begins with the material being fed into a hopper, where it is then transferred to a conveyor system. Airlocks are integrated to prevent dust leakage and maintain a controlled environment. The system's design minimizes material degradation and ensures consistent flow rates, which is critical for maintaining product quality.
Key Features of the Dry Stone Powder Material Handling System
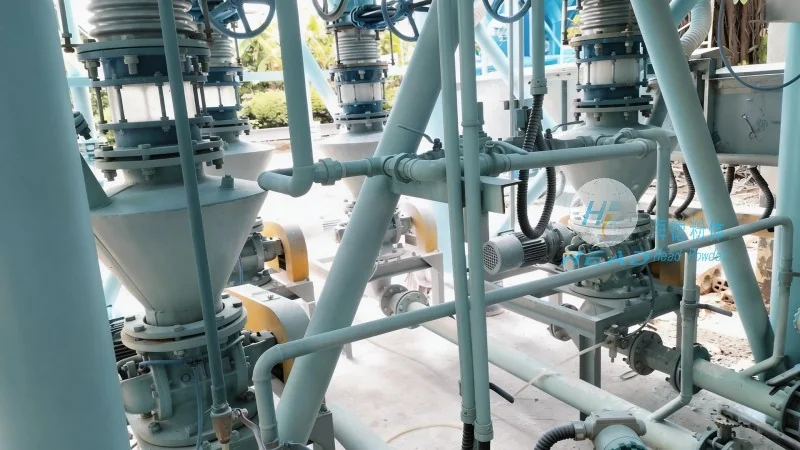
One of the standout features of this system is its high efficiency in handling fine powders without clogging or blockages. The use of special materials for the conveyor belts and components ensures resistance to abrasion and corrosion, which is vital for long-term performance. Another key feature is the system's adaptability, allowing it to be customized for different particle sizes and flow rates. The integration of dust collection systems further enhances safety and compliance with environmental regulations. Additionally, the system's low maintenance requirements and energy efficiency make it a cost-effective solution for businesses.
Benefits for Industrial Applications
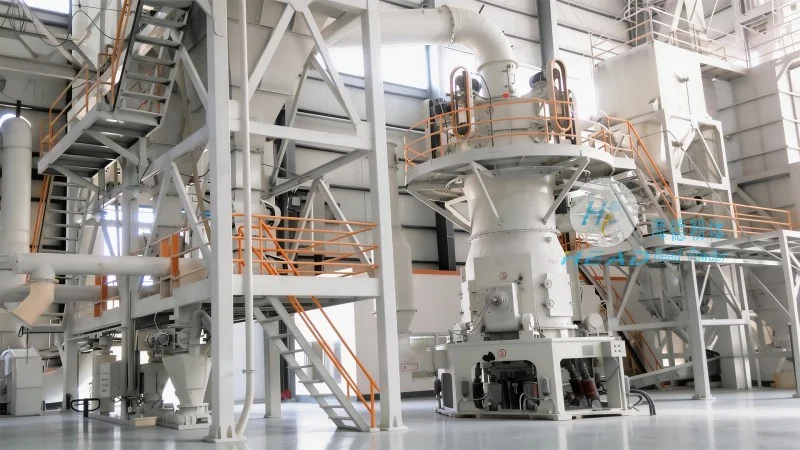
For industries such as construction and mining, the dry stone powder material handling system offers significant advantages. It reduces labor costs by automating the material transport process, while also improving safety by minimizing manual handling of powders. The system's ability to maintain consistent material quality is particularly important in applications where particle size and purity are critical. Furthermore, the system's scalability allows it to be expanded as production needs grow, providing a flexible solution for evolving business requirements.
Conclusion
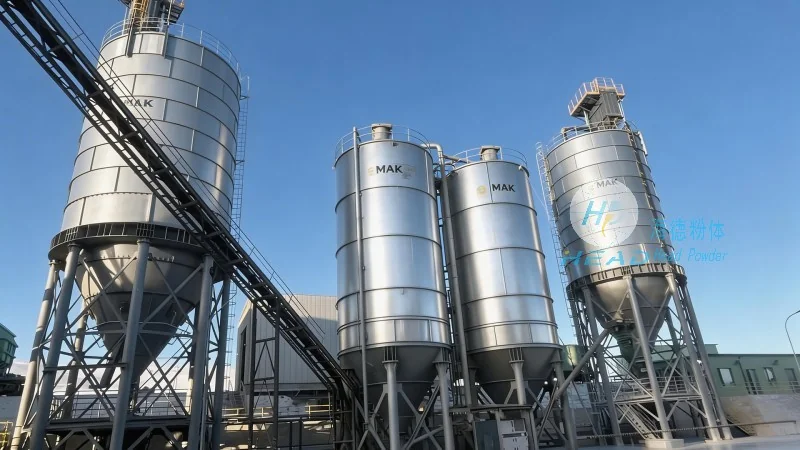
Shandong HeadPowder Engineering Co., Ltd. offers a reliable and efficient dry stone powder material handling system that combines advanced technology with practical design. The system's working principle and features make it an ideal choice for industries requiring precise and safe material transport. With its headquarters in Shandong, China, the company is committed to delivering high-quality solutions that meet the specific needs of its clients.