

Working Principle and Features of Calcined Ash Material Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced calcined ash material conveying system equipment. This article provides an in-depth exploration of the working principle and key features of such systems, highlighting their importance in industrial applications.
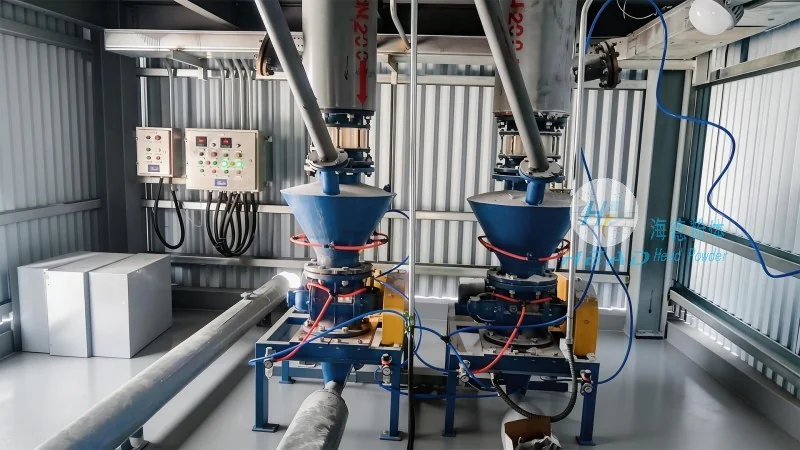
Working Principle of the Calcined Ash Material Conveying System
The calcined ash material conveying system operates through a series of integrated components that ensure efficient and reliable transportation of calcined ash from its source to the designated destination. The core working principle involves the use of specialized machinery, such as belt conveyors, screw conveyors, or pneumatic conveying systems, tailored to handle the unique properties of calcined ash. The system typically begins with the collection of calcined ash, which is then fed into the conveying equipment. Through mechanical or pneumatic forces, the ash is transported along the designated path, maintaining consistent flow rates and minimizing material loss. The process is often automated, with sensors and control systems monitoring the operation to ensure optimal performance and safety.
Key Features of the Calcined Ash Material Conveying System
1. High Efficiency and Capacity: The conveying system is engineered to handle large volumes of calcined ash with minimal downtime. Advanced drive systems and robust construction ensure consistent operation, even under heavy load conditions. This efficiency is crucial for industrial plants that require continuous material flow to maintain production schedules.
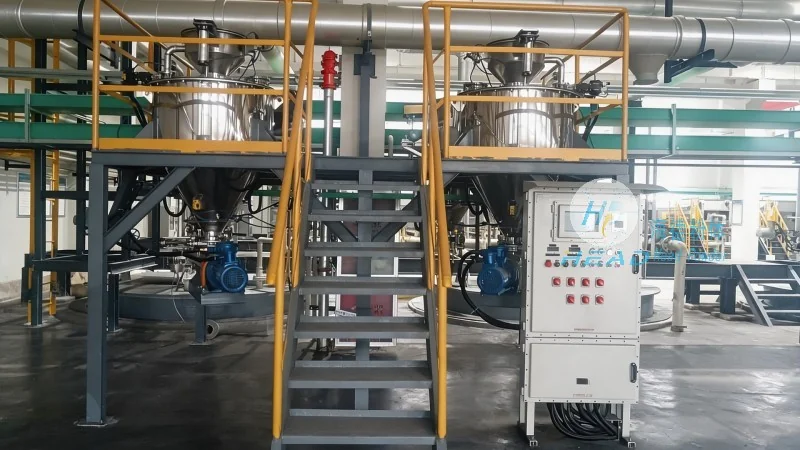
2. Robust and Durable Construction: Built to withstand the harsh conditions associated with calcined ash, the equipment features corrosion-resistant materials and heavy-duty components. This durability reduces maintenance requirements and extends the service life of the system, providing long-term cost savings for users.
3. Adaptability to Material Properties: The system is designed to accommodate the varying characteristics of calcined ash, including its particle size, moisture content, and abrasiveness. Adjustable speed controls and customizable components allow for seamless integration into existing industrial processes, ensuring optimal performance regardless of the material's specific attributes.
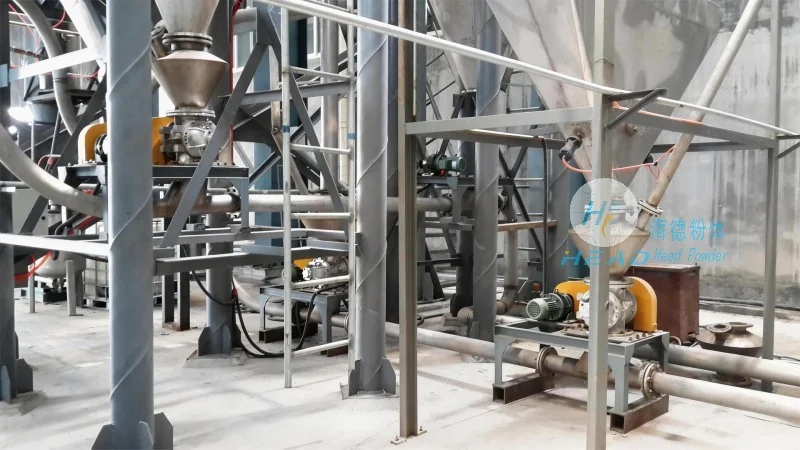
4. Safety and Environmental Compliance: Safety is a top priority in the design of the calcined ash material conveying system. The equipment incorporates features such as emergency stop mechanisms, overload protection, and dust containment systems to prevent accidents and minimize environmental impact. Compliance with industry standards and regulations ensures that the system operates within safe and sustainable parameters.
Applications and Benefits in Industrial Settings
The calcined ash material conveying system is widely used in various industrial sectors, including power generation, cement production, and waste management. Its ability to efficiently transport calcined ash enhances operational efficiency, reduces labor costs, and improves overall productivity. By streamlining the material handling process, the system contributes to a more sustainable and cost-effective operation, aligning with the industry's growing emphasis on efficiency and environmental responsibility.