

Working Principle and Features of Material Pneumatic Conveying Equipment in Dust Collection Stations
For industrial facilities that rely on dust collection systems, efficient material handling is crucial for maintaining operational efficiency and safety. The material pneumatic conveying equipment in dust collection stations plays a vital role in transporting bulk materials from collection points to processing or storage areas. This equipment is designed to handle various types of powders and granules, ensuring smooth and reliable material transfer while minimizing dust dispersion and operational disruptions.
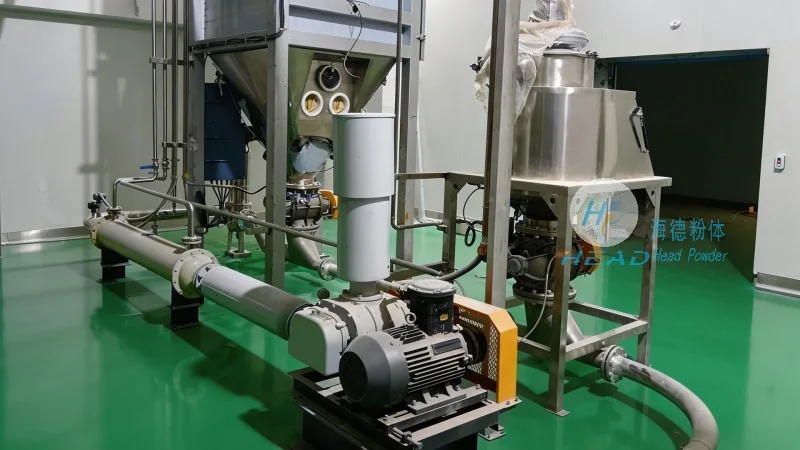
Working Principle of Pneumatic Conveying Systems
The core of a pneumatic conveying system is its ability to use air pressure to move materials through a pipeline. The working principle involves several key components and processes. First, the material is fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air, generated by a blower or fan, is introduced into the system, creating a flow that propels the material forward. The system can operate in either positive pressure or negative pressure modes, depending on the application and material characteristics. Positive pressure systems use air to push the material, while negative pressure systems use suction to draw the material. The choice of mode depends on factors such as material density, particle size, and the distance and layout of the conveying line.
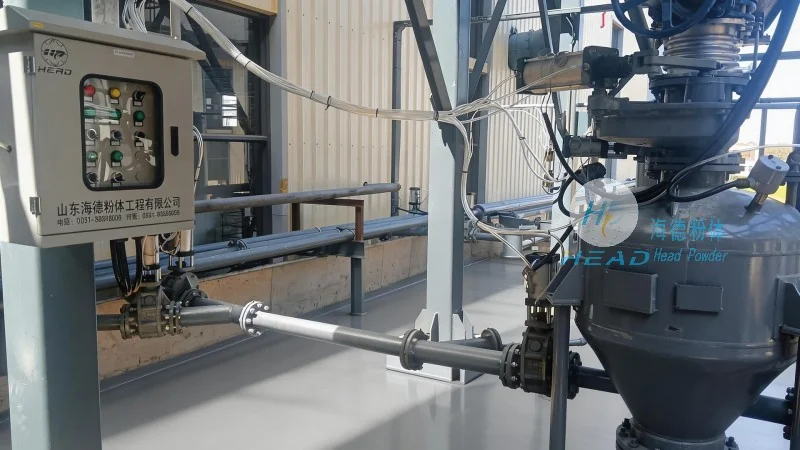
Key Features and Advantages of Pneumatic Conveying Equipment
Material pneumatic conveying equipment in dust collection stations offers several distinct features and advantages that make it an ideal solution for industrial material handling. One of the primary benefits is its ability to handle a wide range of materials, from fine powders to bulk granules, without the need for mechanical components like belts or buckets that can cause wear and tear or material contamination. The system is also highly flexible, allowing for changes in the conveying line layout or material flow rates without significant modifications. Additionally, pneumatic conveying systems are relatively compact and can be integrated into existing dust collection infrastructure, reducing installation time and costs. Another key feature is the minimal dust generation during operation, as the material is enclosed within the pipeline, preventing exposure to the environment and reducing the risk of dust explosions or health hazards. The equipment also provides efficient material transfer over long distances, often with minimal energy consumption compared to traditional mechanical systems.
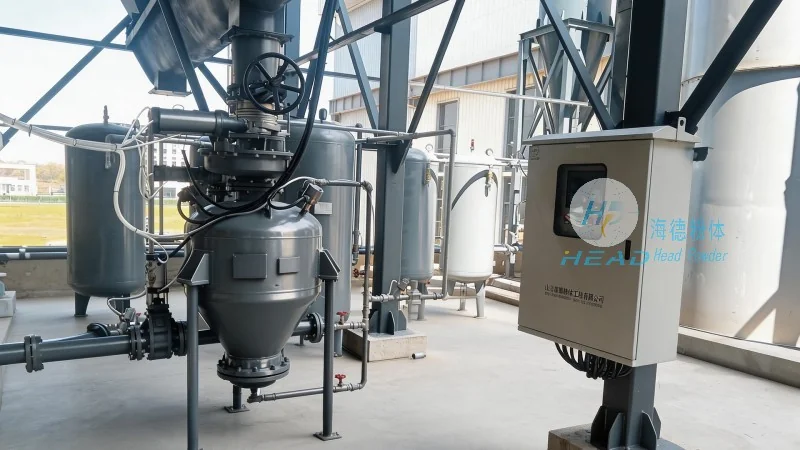
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of material handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the needs of dust collection stations. With years of experience and a commitment to innovation, the company has developed advanced solutions that combine efficiency, reliability, and safety. The company's products are engineered to meet the stringent requirements of industrial applications, ensuring long service life and low maintenance costs. HeadPowder's team of experts works closely with clients to understand their specific material handling challenges and provides customized solutions that optimize operational performance. The company's facilities are equipped with state-of-the-art technology and quality control measures, ensuring that every product meets the highest standards of performance and durability. HeadPowder's dedication to customer satisfaction and technical excellence has made it a trusted partner for industrial facilities worldwide.
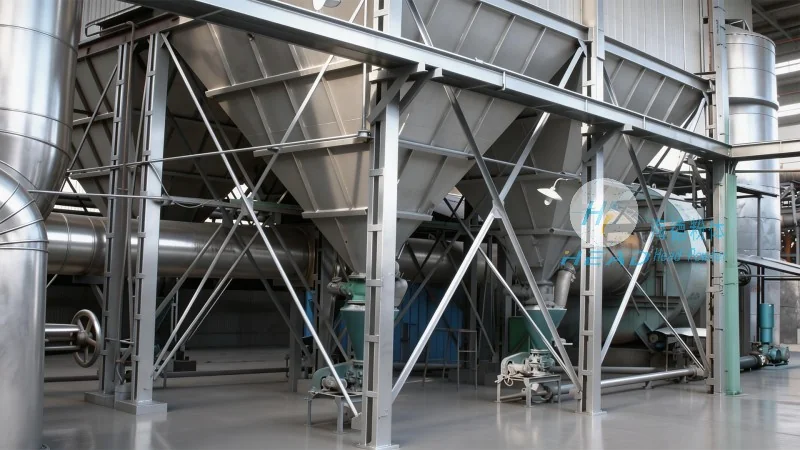
Conclusion
In conclusion, material pneumatic conveying equipment in dust collection stations is a critical component for efficient industrial material handling. By leveraging the principles of air pressure and enclosed transport, these systems offer numerous advantages, including flexibility, minimal dust generation, and efficient long-distance transfer. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced solutions that meet the evolving needs of industrial operations, ensuring safe and reliable material handling in dust collection systems.