

Working Principle and Features of Borax Granular Material Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling borax granular materials. This article delves into the working principle and key features of our borax granular material pneumatic conveying equipment, providing a comprehensive overview for potential clients and industry professionals.
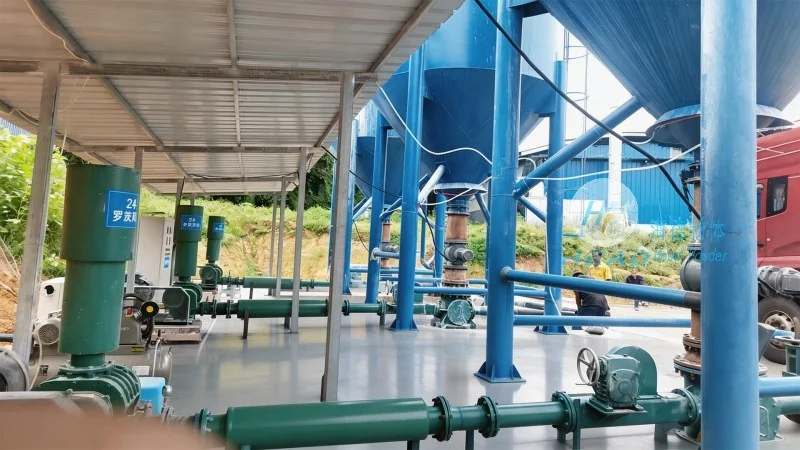
Company Profile and Location
HeadPowder Engineering Co., Ltd. is a reputable company dedicated to delivering high-quality industrial solutions. Our headquarters is located in Shandong, China, where we leverage local manufacturing expertise and advanced technology to develop efficient and reliable pneumatic conveying systems. The company's commitment to precision engineering ensures that our products meet stringent industry standards and customer requirements.
Introduction to Borax Granular Material Pneumatic Conveying Equipment
Borax granular material pneumatic conveying equipment is a critical component in many industrial processes, particularly in the chemical and mineral processing sectors. This system is designed to transport borax granules from one location to another using a combination of air pressure and vacuum, eliminating the need for traditional mechanical conveyors that may cause material degradation or contamination. The equipment is engineered to handle the unique properties of borax granules, such as their size, density, and moisture content, ensuring optimal performance and minimal downtime.
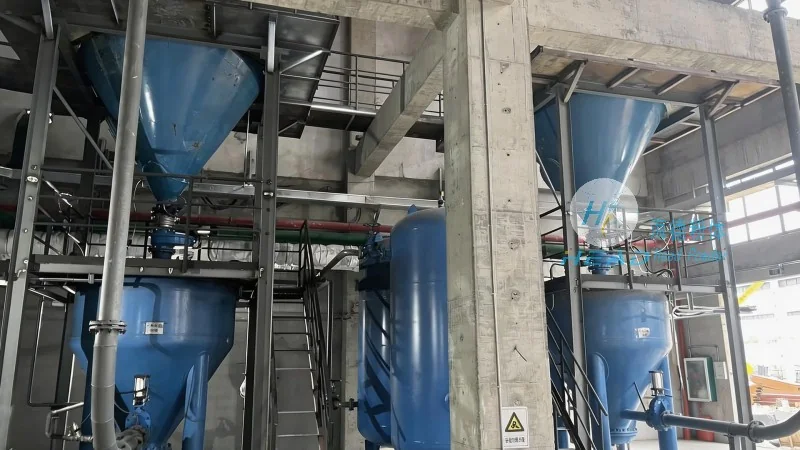
Working Principle of the Pneumatic Conveying System
The operation of borax granular material pneumatic conveying equipment is based on the fundamental principles of fluid dynamics and particle transport. The system typically consists of a hopper, a rotary valve, a pipeline, and a receiver. The process begins when the borax granules are fed into the hopper. A rotary valve then controls the flow of material into the pipeline, where it is mixed with compressed air or a vacuum is applied to create a slurry or suspension. This mixture is then transported through the pipeline to the receiver, where the material is separated from the air and collected. The air is either filtered and recycled or released, depending on the system design. The entire process is automated, allowing for precise control over the flow rate and pressure, which is crucial for maintaining the integrity of the borax granules.
Key Features and Advantages
Our borax granular material pneumatic conveying equipment offers several distinct advantages over traditional conveying methods. Firstly, it provides a clean and hygienic method of material transport, as there is no direct contact between the material and the conveyor components. This is particularly important for borax, which is often used in food and pharmaceutical applications where contamination must be strictly avoided. Secondly, the system is highly efficient, with minimal energy consumption compared to mechanical conveyors. The use of air as the conveying medium reduces wear and tear on equipment, leading to lower maintenance costs and longer service life. Additionally, the equipment is flexible and can be easily integrated into existing production lines, allowing for seamless expansion or modification of the system. The automated control system ensures consistent performance and reduces the risk of human error, enhancing overall operational reliability.
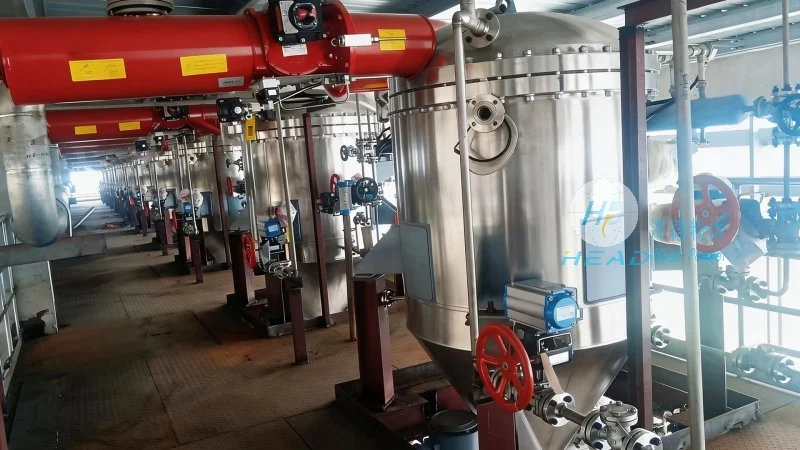
Application Scenarios and Benefits
Borax granular material pneumatic conveying equipment is widely used in various industries, including chemical manufacturing, food processing, and mineral processing. In chemical plants, it is used to transport borax from storage silos to reaction vessels, ensuring a continuous and controlled supply of raw material. In food processing facilities, the system is employed to move borax granules for use in baking powders, detergents, and other consumer products. The benefits of using this equipment in these applications include improved product quality, reduced labor costs, and enhanced safety in the workplace. The system's ability to handle large volumes of material quickly and efficiently makes it an ideal solution for high-throughput production environments.
Conclusion and Contact Information
HeadPowder Engineering Co., Ltd. offers a range of borax granular material pneumatic conveying equipment designed to meet the specific needs of our clients. Our products are engineered with precision and reliability in mind, ensuring that they deliver optimal performance and long-term value. Based in Shandong, China, we are committed to providing high-quality industrial solutions that enhance operational efficiency and product quality. For more information about our pneumatic conveying systems or to discuss your specific application requirements, please contact us at our headquarters in Shandong, China.