

Principle and Working Scene Characteristics of Bulk Bag Unloading Station Pneumatic Conveying
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced bulk bag unloading stations equipped with pneumatic conveying systems. This article delves into the fundamental principles of pneumatic conveying technology used in such stations and explores the key characteristics of their operational environments.
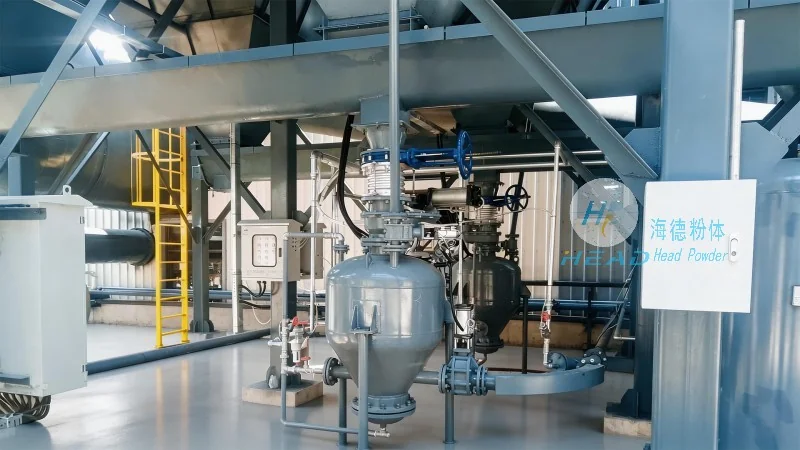
Understanding Pneumatic Conveying in Bulk Bag Unloading Stations
Pneumatic conveying is a method of transporting bulk materials through a pipeline using air or other gas as the conveying medium. In bulk bag unloading stations, this technology is employed to transfer materials from the flexible container (bulk bag) into a storage silo or processing unit efficiently and safely. The process typically involves several key components: a hopper or receiving bin to collect the material from the bulk bag, a vacuum or pressure system to create the airflow, and a pipeline network that directs the material to its destination.
The principle of operation centers on the creation of a pressure differential. When the system is activated, air is drawn into the hopper or is pressurized within the pipeline. This movement of air generates a flow that lifts and transports the bulk material particles through the pipeline. The design of the conveying system, including the size of the pipeline, the velocity of the air, and the angle of the pipeline, all play critical roles in ensuring efficient material transport with minimal degradation or loss.
Key Working Scene Characteristics of Bulk Bag Unloading Stations
The operational environment of bulk bag unloading stations with pneumatic conveying systems is characterized by several distinct features that influence their design and performance. First, the stations are often integrated into industrial facilities handling various bulk materials, such as powders, granules, or fine particles. These materials may vary in density, flowability, and abrasiveness, requiring tailored system configurations to handle specific material properties.
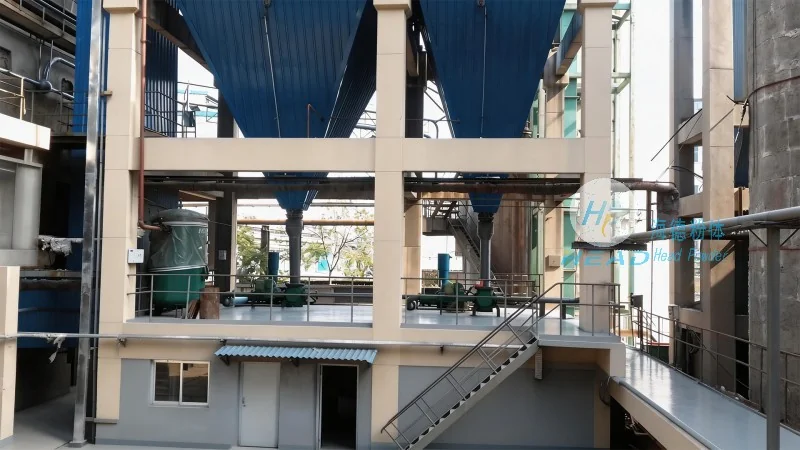
Second, the stations are designed for high throughput and reliability. They are typically used in continuous or semi-continuous operations, where the unloading of bulk bags needs to be completed quickly to maintain production schedules. The systems are engineered to minimize downtime, with features like automatic bag opening, material flow monitoring, and quick system cleaning to ensure smooth operation.
Third, safety and environmental considerations are paramount in these working scenes. Pneumatic conveying systems are equipped with dust collection and filtration systems to control airborne particles and comply with environmental regulations. Additionally, the stations are designed with safety interlocks and emergency stop mechanisms to protect operators and prevent accidents during material handling.
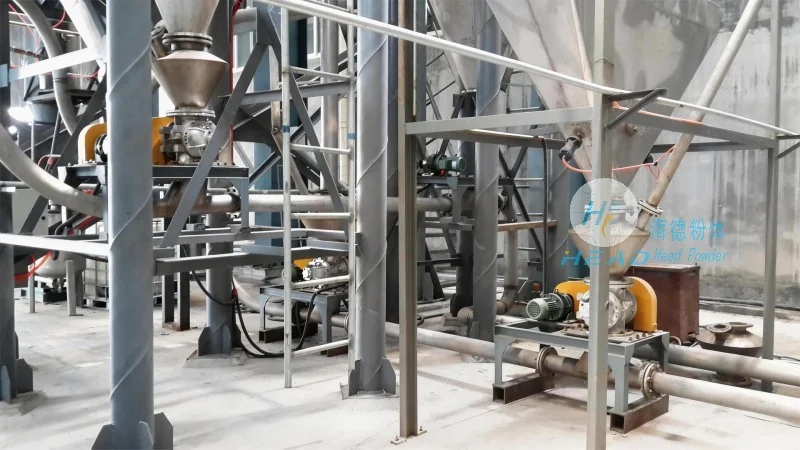
Applications and Benefits in Industrial Settings
Bulk bag unloading stations with pneumatic conveying technology find widespread application across various industries, including chemical, pharmaceutical, food processing, and mining. The primary benefits of these systems include increased operational efficiency, reduced labor costs, and improved material handling safety compared to traditional methods like manual bag emptying or mechanical conveying.
For example, in the chemical industry, where materials may be hazardous or sensitive to moisture, pneumatic conveying systems provide a sealed, dust-free environment that prevents contamination and exposure risks. In the food industry, the systems are designed to meet stringent hygiene standards, with stainless steel components and easy-to-clean designs that maintain product quality and safety.
Conclusion
HeadPowder's expertise in engineering bulk bag unloading stations with pneumatic conveying systems ensures that industrial facilities can achieve efficient, safe, and reliable material handling solutions. By understanding the fundamental principles of pneumatic conveying and the specific characteristics of operational environments, companies can optimize their material handling processes and enhance overall productivity. As a trusted partner in Shandong, China, HeadPowder continues to deliver innovative solutions tailored to the diverse needs of modern industrial operations.