

Principle and Working Scene Characteristics of Intelligent Tonne Bag Loading Station Pneumatic Conve
This section introduces the core concept of the intelligent tonne bag loading station with pneumatic conveying technology. It highlights how this system integrates advanced automation and efficient material handling for industrial applications. The system is designed to streamline the process of loading bulk materials from tonne bags into processing equipment, ensuring high accuracy and minimal waste. By combining intelligent control with pneumatic conveying principles, the system offers a reliable solution for industries requiring precise and consistent material transfer.
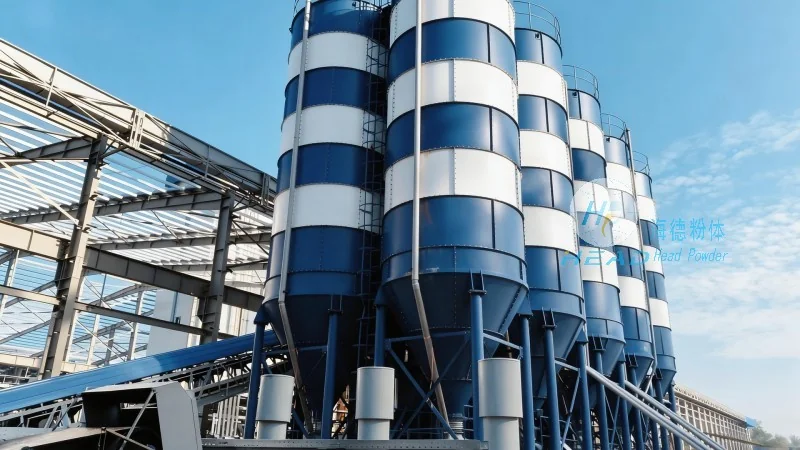
Company Overview
HeadPowder, as the manufacturer, is a professional engineering company based in Shandong, China. With years of experience in the field of material handling and processing, HeadPowder specializes in developing customized solutions for various industrial sectors. The company's commitment to quality and innovation has established it as a trusted partner in providing efficient and reliable pneumatic conveying systems. HeadPowder's team of engineers and technicians work closely with clients to understand their specific needs and design systems that meet or exceed industry standards.
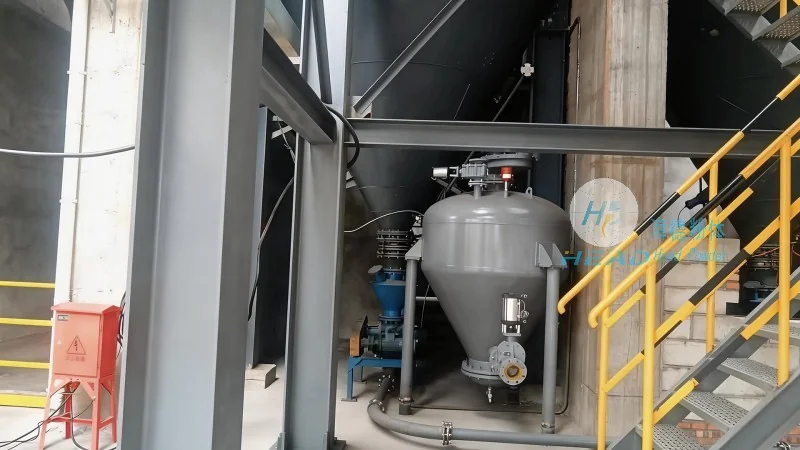
Principle of Pneumatic Conveying in the System
The pneumatic conveying system operates on the principle of using compressed air to transport bulk materials. In the context of the tonne bag loading station, the system draws material from the bag and conveys it through a pipeline to the target equipment. This process involves several key components, including the loading hopper, airlock valve, and conveying pipeline. The system ensures that the material is transported smoothly and without segregation, maintaining consistent flow rates and pressure levels. The compressed air acts as the driving force, creating a pressure differential that moves the material through the system. This method is particularly effective for handling fine powders and granules, which are prone to clumping or degradation in traditional conveying methods.
Working Scene Characteristics and Application Advantages
The intelligent tonne bag loading station is particularly suitable for industries such as chemical, food, and pharmaceuticals, where material purity and hygiene are critical. The system's design allows for easy integration into existing production lines, reducing downtime and increasing overall productivity. Additionally, the system's automated features minimize human intervention, enhancing safety and operational efficiency. The working scene characteristics include high throughput, low maintenance requirements, and the ability to handle a wide range of materials, from powders to granules. The system's compact design also makes it suitable for facilities with limited space, providing a flexible solution for various operational needs.
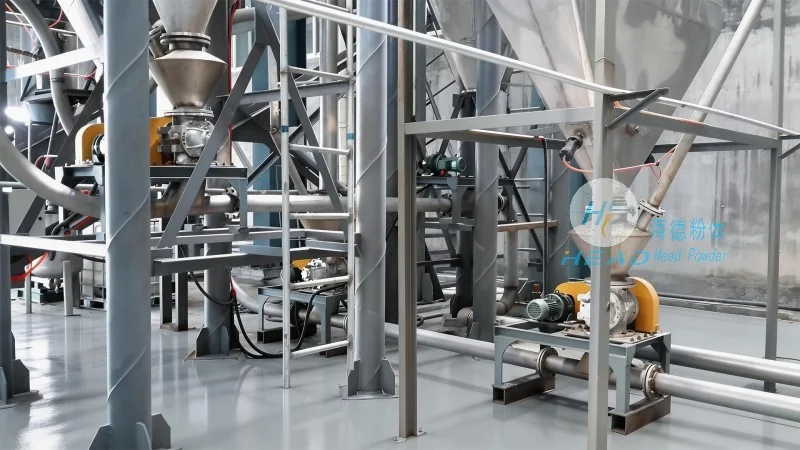
Technical Features and Operational Efficiency
The system incorporates advanced control systems that monitor and adjust the conveying process in real-time. This ensures optimal performance and prevents issues such as blockages or pressure fluctuations. The use of high-quality materials in the construction of the components ensures durability and long-term reliability. The operational efficiency of the system is further enhanced by its energy-saving design, which reduces power consumption while maintaining high conveying rates. The intelligent control system also allows for remote monitoring and diagnostics, enabling quick troubleshooting and minimizing downtime. Overall, the intelligent tonne bag loading station with pneumatic conveying technology offers a comprehensive solution for efficient material handling in industrial settings, combining performance, reliability, and cost-effectiveness.