

Principles and Working Scene Characteristics of Food Powder Conveying Systems
Food powder conveying systems are critical components in the food processing industry, designed to efficiently transport bulk powders such as flour, sugar, and other dry ingredients. These systems ensure smooth material handling, maintain product quality, and enhance operational efficiency in various food production environments. Understanding the underlying principles and diverse working scenarios of these systems is essential for optimizing production lines and meeting industry standards.
Core Principles of Food Powder Conveying
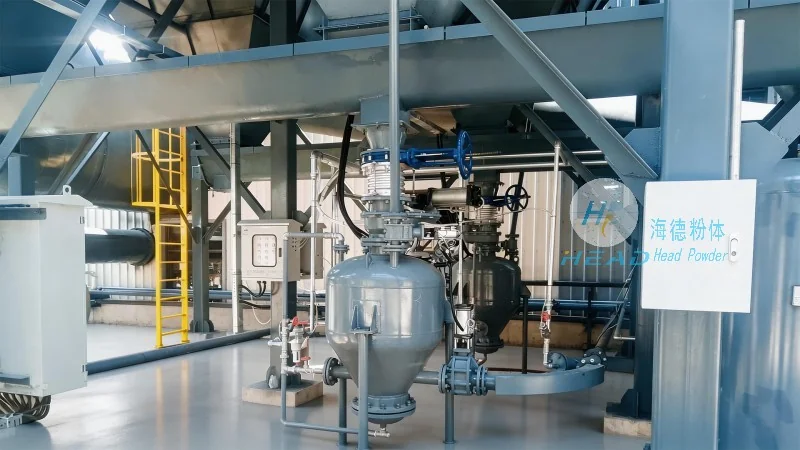
The fundamental principles of food powder conveying systems revolve around the use of mechanical and pneumatic technologies to move powders from one location to another. Key mechanisms include screw conveyors, pneumatic conveyors, and bucket elevators, each tailored to specific powder characteristics and operational requirements. For instance, screw conveyors utilize rotating screws to push powders forward, while pneumatic systems employ air pressure to transport materials through pipelines. These principles ensure consistent flow rates, minimal product degradation, and compliance with hygiene standards essential in food processing.
Working Scene Characteristics
Food powder conveying systems operate across a wide range of industrial settings, each with unique characteristics that influence system design and performance. In bakery facilities, for example, systems must handle high volumes of flour and sugar while maintaining low moisture levels to prevent caking. In dairy processing plants, conveying systems for powdered milk require strict temperature control and contamination prevention measures. Additionally, in pharmaceutical food production, systems must adhere to GMP (Good Manufacturing Practice) guidelines, ensuring that all components are easy to clean and maintain. The versatility of these systems allows them to adapt to different production scales, from small-scale artisanal operations to large-scale industrial facilities.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
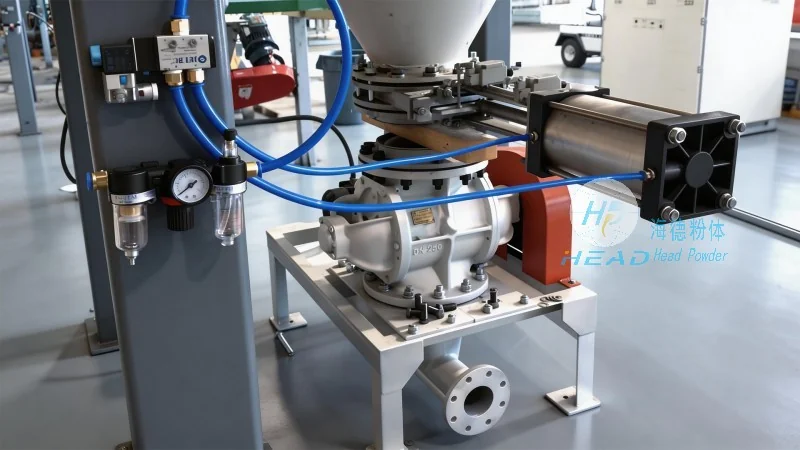
HeadPowder, a leading provider of specialized engineering solutions, specializes in designing and manufacturing advanced food powder conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the food processing industry. HeadPowder's team of experienced engineers and technicians works closely with clients to understand their specific needs, offering customized solutions that enhance operational efficiency and product safety. The company's headquarters is located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services to global markets.
Applications in Food Production
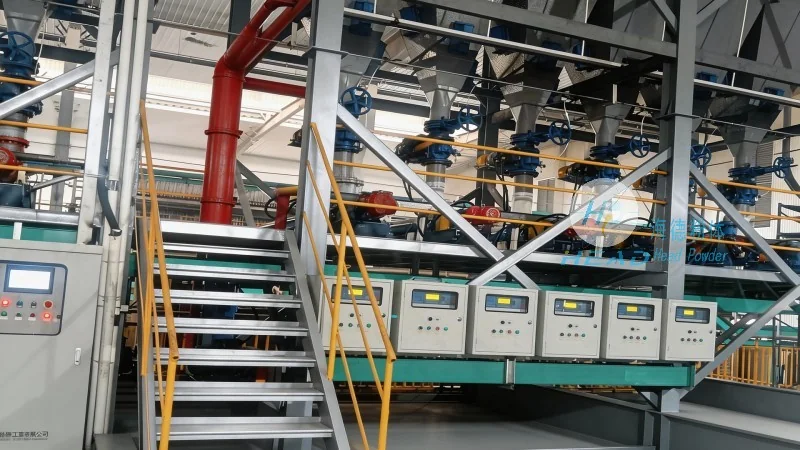
Food powder conveying systems are integral to various stages of food production, from raw material handling to final product packaging. In the initial stages, these systems efficiently transport raw powders from storage silos to processing lines, reducing manual labor and improving workflow. During processing, they ensure consistent material distribution, which is crucial for maintaining product uniformity. In packaging, conveying systems transfer finished powders to packaging machines, streamlining the final production step. By integrating these systems into production lines, food manufacturers can achieve higher throughput, lower operational costs, and improved product quality.
Advantages of Advanced Conveying Solutions
Modern food powder conveying systems offer several advantages over traditional methods, including improved hygiene, reduced product loss, and enhanced energy efficiency. Hygienic design features, such as smooth surfaces and easy-to-clean components, minimize the risk of contamination and ensure compliance with food safety regulations. Reduced product loss is achieved through optimized flow control and minimal material degradation during transport. Energy efficiency is achieved through the use of variable speed drives and efficient air compression systems, which lower operational costs and environmental impact. These advantages make advanced conveying solutions a valuable investment for food manufacturers looking to stay competitive in today's market.