

Principle and Working Scene Characteristics of Nitrogen-Protected Powder Handling Equipment
The efficient and safe handling of powders is a critical concern in various industrial applications, especially when dealing with materials that are sensitive to moisture, oxidation, or contamination. In such scenarios, nitrogen-protected powder handling equipment emerges as a vital solution, ensuring the integrity and quality of the processed materials. This article delves into the underlying principles of these systems and explores the distinct working scene characteristics that define their application in modern industrial settings.
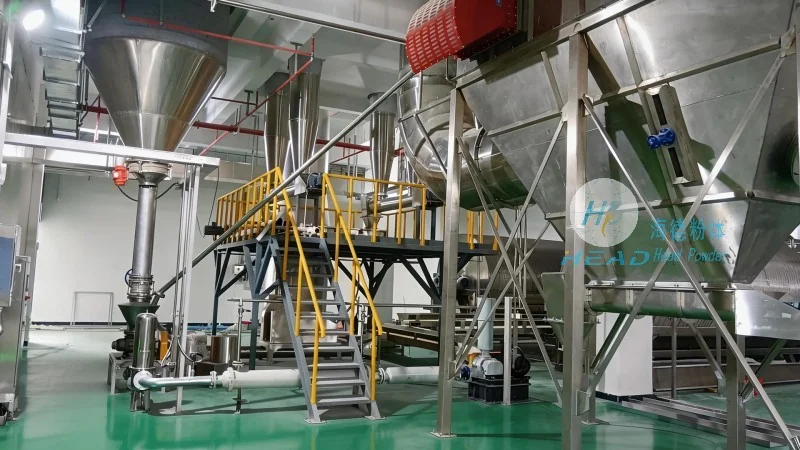
The Core Principle of Nitrogen-Protected Powder Handling Equipment
The fundamental principle of nitrogen-protected powder handling equipment is the establishment of an inert gas environment, primarily utilizing nitrogen gas, to isolate the powder from atmospheric contaminants. This is accomplished through a closed-loop system where nitrogen is continuously circulated or introduced to maintain a positive pressure within the handling system. Key components such as gas generators, high-efficiency filters, and pressure regulators work in tandem to ensure a consistent and high-purity nitrogen supply. By maintaining an oxygen level below the flammability limit and preventing moisture ingress, the system effectively safeguards the powder's chemical and physical properties, extends its shelf life, and mitigates the risk of spontaneous combustion or explosion.
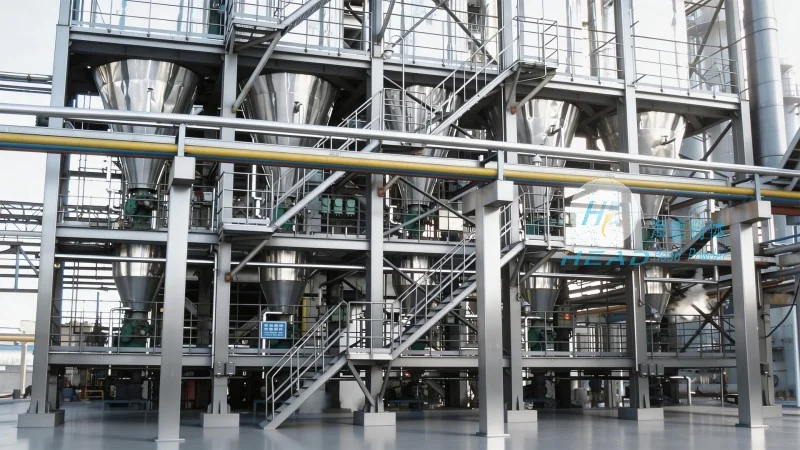
Working Scene Characteristics and Application Diversity
The working scene characteristics of nitrogen-protected powder handling equipment are tailored to specific industrial needs, making them highly adaptable across various sectors. These systems are commonly employed in pharmaceutical, food processing, chemical, and aerospace industries where material purity is non-negotiable. The equipment is designed to handle a wide spectrum of powder types, ranging from fine pharmaceutical actives to bulk food additives and chemical reagents. The working environment is characterized by precision control, minimal contamination, and strict adherence to safety and regulatory standards. For instance, in pharmaceutical manufacturing, the nitrogen-protected system ensures that active ingredients remain stable and free from degradation, which is crucial for maintaining product efficacy and compliance with stringent regulatory requirements. Similarly, in food processing, the system prevents microbial growth and oxidation, preserving the nutritional value and shelf life of sensitive food products.
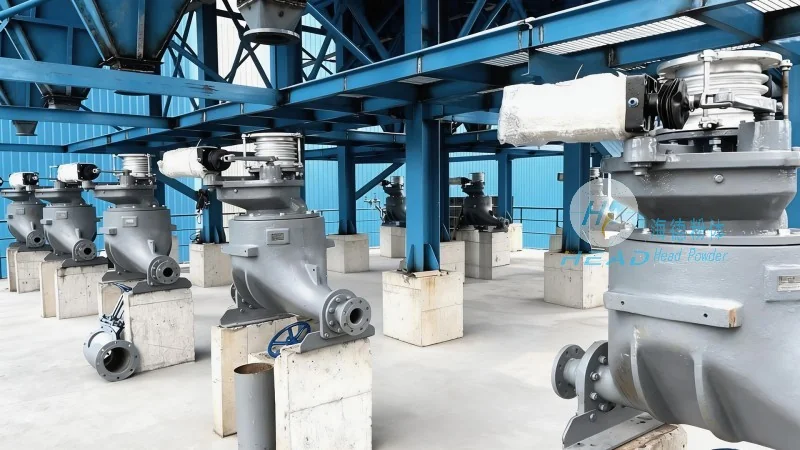
HeadPowder: A Leading Provider of Nitrogen-Protected Solutions
HeadPowder, operating as Shandong HeadPowder Engineering Co., Ltd. from its base in Shandong, China, specializes in the design, manufacturing, and integration of nitrogen-protected powder handling equipment. The company leverages advanced engineering, rigorous quality control, and customer-centric approaches to deliver tailored solutions that meet the unique demands of diverse industries. With a strong commitment to innovation and safety, HeadPowder has established itself as a trusted partner for businesses seeking to enhance their powder handling processes while ensuring compliance with industry standards and regulatory requirements. The company's expertise in material science and process engineering enables it to develop systems that optimize efficiency, reduce downtime, and improve overall operational safety.
Key Advantages in Industrial Applications
Implementing nitrogen-protected powder handling equipment offers several advantages that contribute to improved operational performance and product quality. These include enhanced material stability, reduced contamination risks, extended product shelf life, and improved safety in handling hazardous powders. The closed-loop nitrogen system minimizes exposure to external contaminants, ensuring that the powder remains in its original state throughout the handling and processing stages. Additionally, the positive pressure environment prevents the ingress of air, further protecting the material from oxidation and moisture-related degradation. In industrial settings, this translates to higher product yields, lower waste, and reduced maintenance costs due to the reduced risk of equipment damage from corrosion or fire.
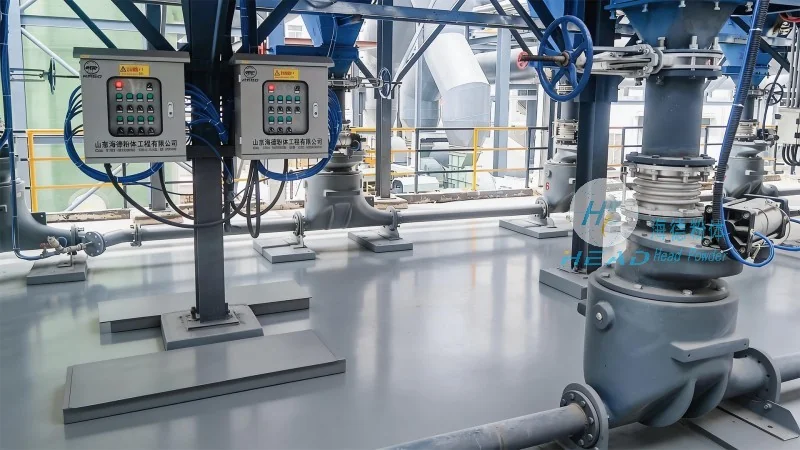
Conclusion: The Role of Nitrogen-Protected Systems in Modern Manufacturing
As industries continue to prioritize efficiency, safety, and product quality, nitrogen-protected powder handling equipment plays an increasingly vital role in modern manufacturing processes. By understanding the core principles and working scene characteristics of these systems, businesses can make informed decisions to integrate effective solutions that meet their specific operational needs. With companies like Shandong HeadPowder Engineering Co., Ltd. leading the way in innovation and quality, the adoption of nitrogen-protected technology continues to advance, ensuring that powder handling remains a reliable and safe component of industrial operations across various sectors.