

Principle and Working Scene Characteristics of Fully Automatic Bulk Bag Unloading Powder Conveying S
For industrial applications that require efficient handling of bulk powders, the fully automatic bulk bag unloading powder conveying system has emerged as a critical solution. This advanced equipment is designed to streamline the process of transferring materials from bulk bags into processing lines, ensuring high efficiency, safety, and reliability in various industrial settings.
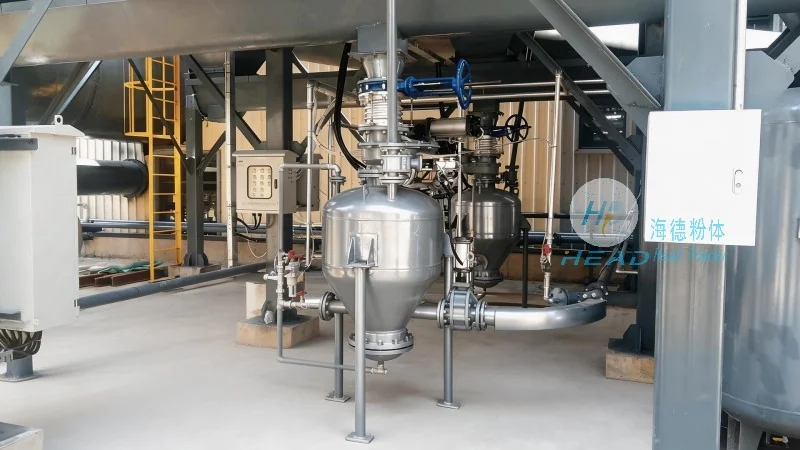
Overview of the Fully Automatic Bulk Bag Unloading Powder Conveying System
The system, developed by Shandong HeadPowder Engineering Co., Ltd., integrates multiple components to achieve seamless operation. At its core, the system comprises a bulk bag unloader, a powder conveyor, and control systems that work in tandem to automate the entire material handling workflow. The unloader is engineered to safely open and empty bulk bags, while the conveyor transports the material to the desired destination, such as silos, storage tanks, or processing equipment. This integration minimizes manual intervention, reduces labor costs, and enhances operational consistency.
Principle of Operation
The working principle of the fully automatic bulk bag unloading powder conveying system is based on a combination of mechanical and pneumatic technologies. The bulk bag is placed on a support frame, and the system uses a series of mechanisms to open the bag's top, allowing the powder to flow into a hopper or directly into the conveyor. The unloader typically employs a valve or a discharge port that is activated by a pneumatic actuator. Once the bag is opened, the powder is drawn into the conveyor via a vacuum or pressure system, depending on the design. The conveyor then transports the material to the processing area, where it can be further handled or stored. The control system monitors the entire process, ensuring that the unloading and conveying operations are synchronized and that any anomalies are detected and addressed promptly.
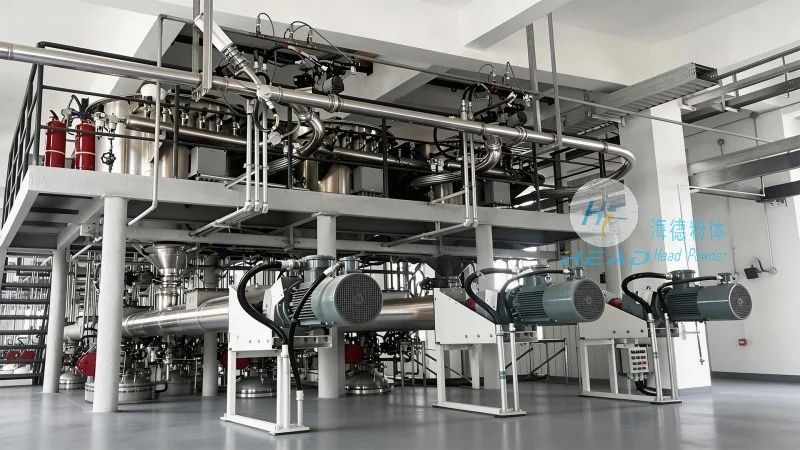
Key Working Scene Characteristics
The fully automatic bulk bag unloading powder conveying system is particularly suited for industrial environments where bulk powders are frequently used, such as food processing, pharmaceutical manufacturing, chemical production, and mining operations. In these settings, the system offers several advantages that enhance operational efficiency and product quality. For instance, in food processing facilities, the system ensures that powders are handled hygienically and without contamination, meeting stringent safety and regulatory standards. In pharmaceutical manufacturing, the system maintains a clean and controlled environment, preventing cross-contamination and ensuring product purity. In chemical plants, the system handles abrasive or corrosive powders with minimal wear and tear, extending the equipment's lifespan and reducing maintenance costs. Additionally, the system's automation capabilities make it ideal for high-volume production lines, where consistent and reliable material handling is essential to meet production targets.
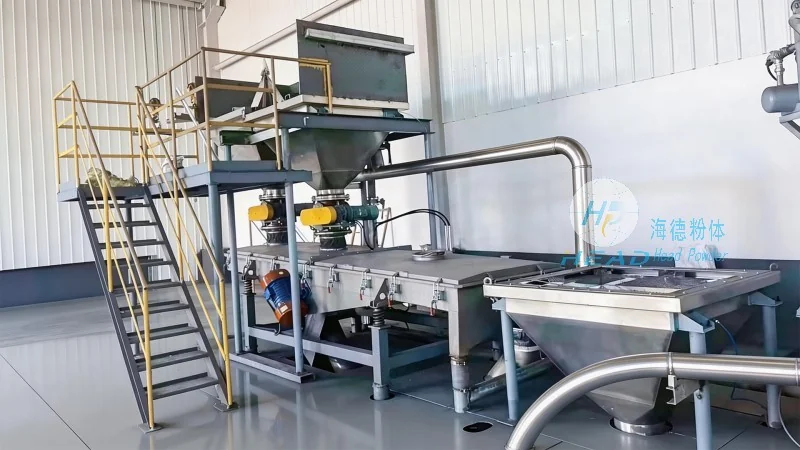
Benefits and Advantages
Implementing a fully automatic bulk bag unloading powder conveying system provides numerous benefits to industrial operations. Firstly, it significantly reduces labor requirements by automating the entire unloading and conveying process, allowing workers to focus on other critical tasks. This not only improves productivity but also enhances workplace safety by minimizing manual handling of heavy or hazardous materials. Secondly, the system ensures consistent material flow, reducing the risk of bottlenecks or interruptions in production. The precise control of the conveyor speed and unloading rate helps maintain a steady supply of powders to downstream processes, preventing downtime and improving overall efficiency. Thirdly, the system enhances product quality by minimizing material loss and contamination. The enclosed design of the conveyor and unloader prevents dust and particles from escaping, maintaining a clean working environment and ensuring that the powders remain free from impurities. Finally, the system offers cost savings through reduced maintenance and operational costs. The automated components require less frequent manual intervention, and the durable construction of the equipment reduces the need for frequent repairs or replacements.
Application Examples
The fully automatic bulk bag unloading powder conveying system is widely used in various industrial applications. For example, in a food processing plant, the system may be used to handle ingredients such as flour, sugar, or spices from bulk bags into storage silos or mixing equipment. In a pharmaceutical facility, the system could transport raw materials like active pharmaceutical ingredients (APIs) or excipients into processing lines, ensuring that the materials are handled under sterile conditions. In a chemical manufacturing plant, the system may be employed to convey bulk chemicals, such as powders used in fertilizer production or industrial coatings, to reactors or storage tanks. Each application benefits from the system's ability to handle different types of powders, including fine, coarse, or abrasive materials, with consistent performance and reliability.