

Principles and Working Scene Characteristics of Recycled Sand Material Conveying
Understanding the principles and operational characteristics of recycled sand material conveying is crucial for optimizing material handling processes in various industrial applications. This article explores the fundamental mechanisms behind the transport of recycled sand, alongside key working scene characteristics that define its effective implementation.
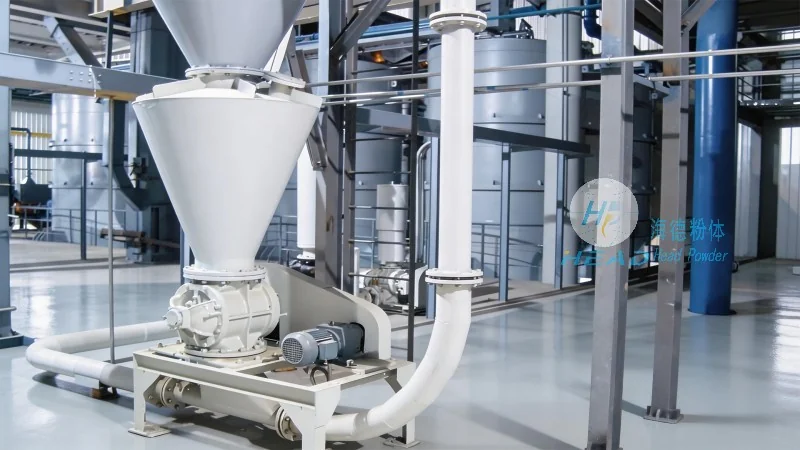
Company Overview and Expertise
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized material handling solutions. With a strong presence in China, particularly in Shandong, the company has built a reputation for delivering innovative and efficient systems tailored to the unique demands of the construction and recycling industries. Their expertise lies in the design, manufacturing, and integration of conveying equipment that ensures reliable and cost-effective movement of recycled sand materials.
Principles of Recycled Sand Material Conveying
The core principle of recycled sand material conveying involves the use of mechanical systems to transport sand that has been reclaimed from construction and demolition sites. This process typically begins with the collection and sorting of waste materials, followed by processing to recover the sand. The conveying system then takes over, utilizing various technologies such as belt conveyors, screw conveyors, or pneumatic systems to move the sand from one location to another. The effectiveness of this process hinges on several key factors, including the material's properties, the conveying equipment's design, and the operational environment.
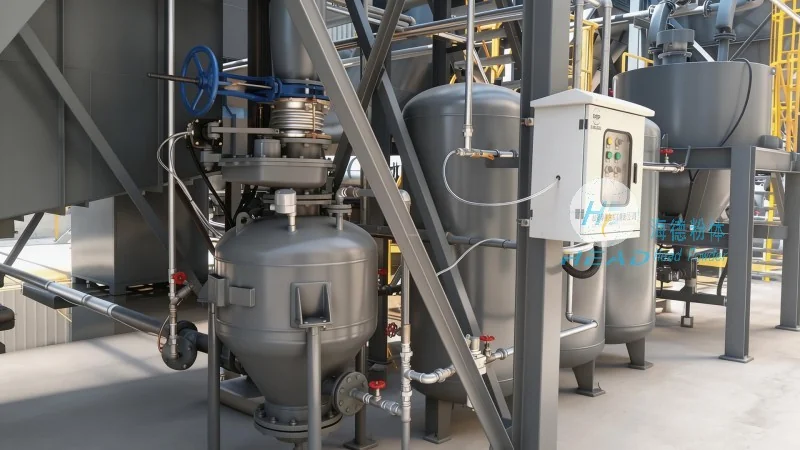
Working Scene Characteristics
The working scene characteristics of recycled sand material conveying vary significantly based on the specific application and industry. For instance, in concrete recycling operations, the conveying system must handle sand mixed with debris and moisture, requiring robust equipment capable of handling abrasive and wet materials. In contrast, applications within foundries or casting processes may involve conveying sand with higher temperatures or specific grain sizes, demanding specialized components like heat-resistant belts or adjustable speed controls.
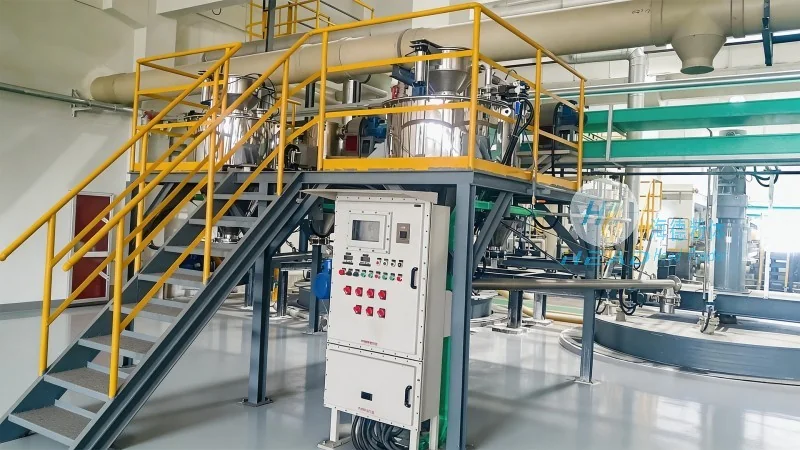
Key Operational Considerations
Several operational considerations are essential for the successful implementation of recycled sand conveying systems. First, the system must be designed to minimize material degradation and loss during transport. This often involves using smooth, non-abrasive surfaces and proper sealing to prevent dust emissions and material spillage. Second, energy efficiency is a critical factor, as conveying systems can consume significant power. Modern solutions incorporate variable frequency drives and optimized belt tensions to reduce energy consumption while maintaining performance. Third, maintenance and durability are paramount, given the abrasive nature of recycled sand. High-quality materials and regular maintenance schedules are necessary to ensure long-term reliability and minimize downtime.
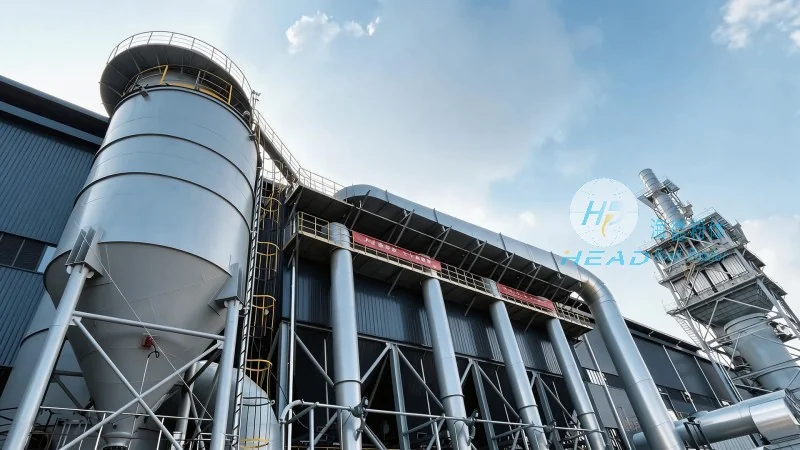
Application Examples and Industry Impact
Recycled sand material conveying finds widespread application across multiple industries, including construction, foundry, and environmental remediation. In the construction sector, it enables the reuse of sand from demolition sites, reducing the need for virgin materials and lowering project costs. In foundries, the system ensures a consistent supply of reclaimed sand for casting processes, improving product quality and reducing waste. The environmental benefits are also substantial, as the recycling of sand reduces landfill usage and conserves natural resources. By integrating efficient conveying solutions, industries can achieve greater sustainability and operational efficiency.
Conclusion
In summary, the principles and working scene characteristics of recycled sand material conveying are integral to modern material handling strategies. With advancements in technology and design, these systems offer reliable, efficient, and sustainable solutions for transporting reclaimed sand. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing the expertise and equipment needed to implement these systems effectively, contributing to the growth of recycling and sustainable practices in the industry.