

Principle of Stone Pneumatic Conveying System
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of pneumatic conveying systems for various bulk materials, including stones and aggregates. The company, based in Shandong, China, leverages advanced engineering principles to deliver efficient and reliable systems tailored to the unique requirements of the construction and industrial sectors.
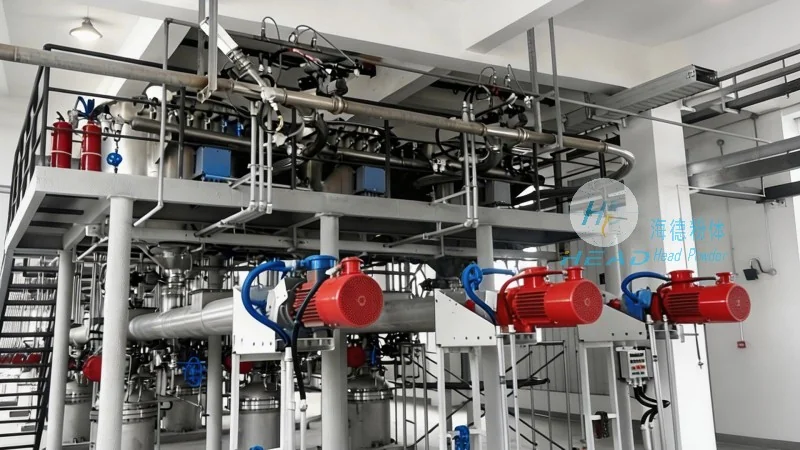
Understanding Pneumatic Conveying Systems for Stone Materials
Pneumatic conveying systems utilize air or gas to transport solid materials like stones, gravel, and crushed aggregates from one location to another. This method offers a non-contact, low-maintenance approach compared to traditional mechanical conveyors. The core principle involves creating a pressure differential that propels the material through a pipeline using air flow. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The choice of system type—such as dilute phase or dense phase—depends on factors like material characteristics, distance, and desired flow rate. Dilute phase systems use higher air velocities to transport material in a suspended state, while dense phase systems employ lower velocities to move material in a slurry-like state, minimizing particle degradation.
Key Components and Their Functions in a Stone Pneumatic Conveying System
The effectiveness of a pneumatic conveying system for stone materials hinges on several critical components, each playing a vital role in the overall operation. The hopper serves as the storage vessel, holding the bulk material before it is fed into the system. It is designed with a sloped bottom to facilitate smooth material discharge. The feeder, often a rotary or vibratory type, regulates the material flow rate into the conveying line, ensuring consistent and controlled transport. The conveying line is typically made of durable materials like stainless steel or PVC to withstand the abrasive nature of stone particles. It may include bends, expansions, and filters to maintain system efficiency and prevent material buildup. The receiver or discharge hopper collects the conveyed material, allowing for further processing or storage. Additionally, air compressors and filters are essential for generating the necessary air pressure and maintaining air quality, respectively. Proper maintenance of these components is crucial to ensure the longevity and performance of the system.
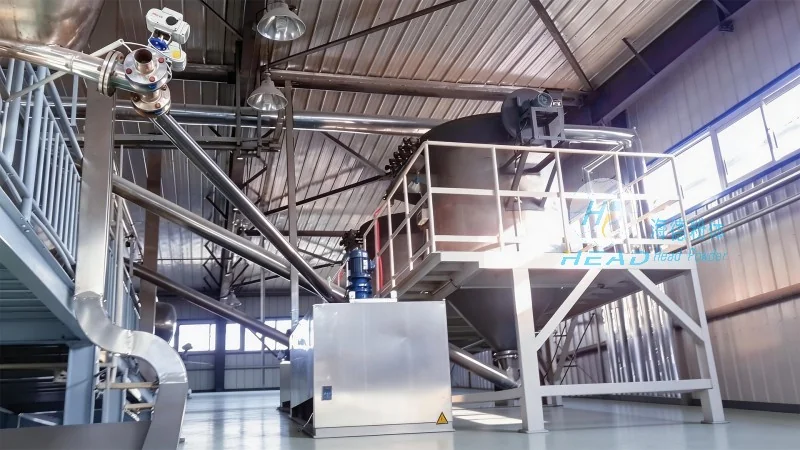
Advantages of Using Pneumatic Conveying for Stone Handling
Compared to traditional conveyor systems, pneumatic conveying offers several advantages when handling stone materials. First, it eliminates the need for physical contact between the material and the conveyor components, reducing wear and tear on both the equipment and the material itself. This is particularly beneficial for abrasive stones that can cause significant damage to mechanical conveyors over time. Second, pneumatic systems are highly flexible, allowing for changes in material flow direction and distance without major structural modifications. This adaptability makes them suitable for complex layouts in industrial and construction sites. Third, the system operates with minimal noise and dust emissions, contributing to a safer and more environmentally friendly working environment. Furthermore, pneumatic conveying can handle a wide range of stone sizes and types, from fine gravel to large crushed stones, making it a versatile solution for various applications. The ability to transport materials in a closed system also helps in controlling dust and preventing contamination, which is critical in food processing or pharmaceutical industries, though not directly applicable here, it highlights the system's versatility.
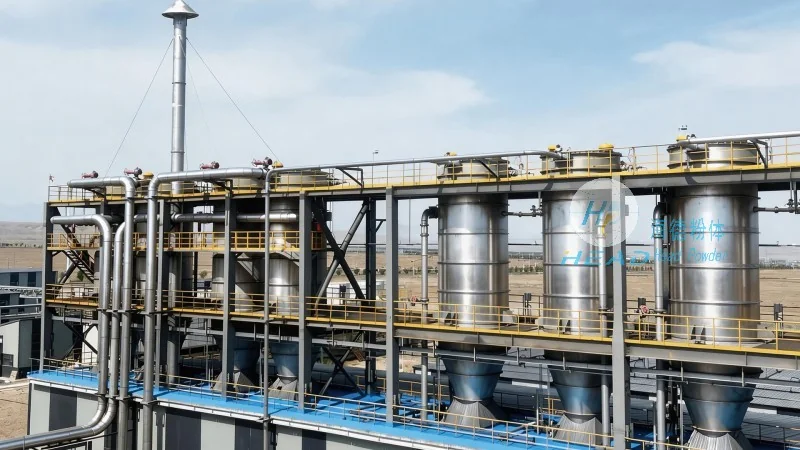
Applications of Stone Pneumatic Conveying Systems
Stone pneumatic conveying systems find extensive applications across multiple industries. In the construction sector, they are widely used to transport aggregates from stockpiles to batching plants or concrete mixing stations. This ensures a continuous and efficient supply of materials, reducing downtime and improving productivity. The system is also employed in mining operations to move crushed ore or rock from processing facilities to storage areas. In the aggregate production industry, pneumatic conveying is used to transport raw materials like limestone or sand to processing plants, facilitating the production of high-quality construction materials. Additionally, in the recycling industry, these systems help in transporting recycled aggregates from sorting facilities to recycling centers. The ability to handle abrasive and heavy materials makes pneumatic conveying an ideal choice for applications where mechanical conveyors may not be suitable due to their high maintenance costs or limited flexibility.
HeadPowder's Expertise in Designing and Implementing Stone Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner in the design and implementation of stone pneumatic conveying systems. With a team of experienced engineers and technicians, the company provides customized solutions tailored to the specific needs of each client. The design process begins with a thorough analysis of the material characteristics, including particle size, density, and moisture content, as well as the operational requirements such as distance, flow rate, and system layout. HeadPowder utilizes advanced software and simulation tools to model the system and optimize performance before manufacturing. The company's commitment to quality is evident in its adherence to international standards and rigorous testing protocols. Each system is manufactured using high-quality materials and components to ensure durability and reliability. Post-installation, HeadPowder offers comprehensive training and maintenance services to ensure the system operates at peak efficiency. The company's local presence in Shandong, China, allows for quick response times and on-site support, enhancing customer satisfaction and system performance. By combining technical expertise with customer-centric service, HeadPowder delivers pneumatic conveying systems that meet the highest industry standards and provide long-term value to its clients.