

Principle of Sugar Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for the sugar industry. The company, commonly known as headpowder, leverages decades of experience to deliver efficient and reliable solutions for bulk material handling in sugar processing facilities. This article delves into the fundamental principles behind sugar pneumatic conveying equipment, highlighting key components, operational mechanisms, and the technological advancements that enhance performance and safety.
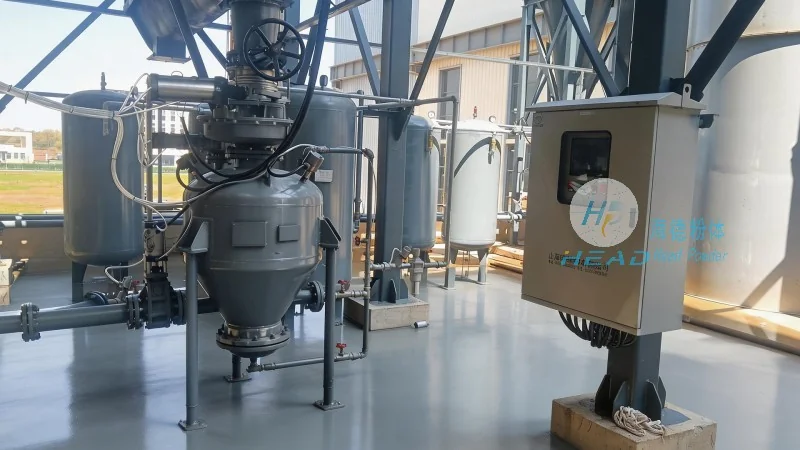
Core Components of Pneumatic Conveying Systems for Sugar
The pneumatic conveying equipment for sugar typically consists of several critical components that work in tandem to transport sugar from one location to another. These include the hopper or feeder, which holds the sugar and regulates the flow; the conveying line, which can be either positive or negative pressure systems; the air compressor or vacuum pump, which provides the necessary air or vacuum to move the material; and the receiver or discharge hopper, where the sugar is deposited. Each component plays a vital role in ensuring smooth and continuous operation, minimizing material degradation and optimizing energy efficiency.
How Pneumatic Conveying Works in Sugar Handling
The principle of pneumatic conveying for sugar involves the use of air to transport granular or powdered materials through a pipeline. In a positive pressure system, air is forced through the conveying line, carrying the sugar particles along with it. The air velocity is carefully controlled to ensure that the sugar remains suspended and moves efficiently without causing blockages or excessive wear on the equipment. Conversely, a negative pressure system uses a vacuum to draw the sugar into the conveying line, which is often preferred for applications requiring airtight containment or when the sugar needs to be transported from a higher to a lower elevation. The choice between positive and negative pressure depends on factors such as the distance, elevation changes, and the nature of the sugar being handled.
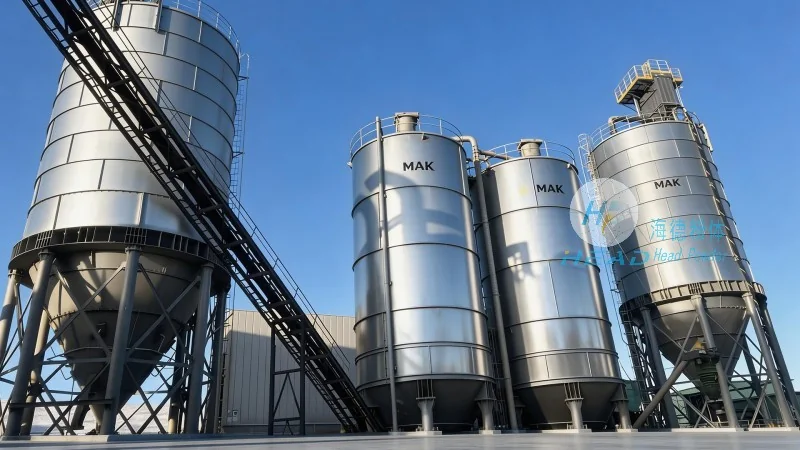
Advantages of Using Pneumatic Conveying for Sugar
Implementing pneumatic conveying equipment for sugar offers numerous advantages over traditional methods like belt conveyors or manual handling. One of the primary benefits is the ability to handle bulk quantities of sugar with minimal labor, reducing operational costs and improving productivity. The enclosed system also prevents contamination from dust, moisture, or other environmental factors, ensuring the quality and purity of the sugar. Additionally, pneumatic conveying systems are highly flexible, allowing for easy integration with existing processing lines and the ability to transport sugar to multiple destinations from a single source. The technology also minimizes material degradation, as the sugar is not subjected to excessive friction or impact during transport, which is crucial for maintaining its quality and market value.
Technological Innovations in Sugar Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd. continuously invests in research and development to enhance the performance of sugar pneumatic conveying equipment. Recent innovations include the integration of advanced control systems that monitor and adjust air pressure, flow rates, and material levels in real-time, ensuring optimal operation and preventing system failures. The use of high-quality materials, such as stainless steel and corrosion-resistant alloys, in the construction of conveying lines and components extends the equipment's lifespan and maintains hygiene standards required in the food industry. Furthermore, the company has developed customized solutions that address specific challenges in sugar processing, such as handling fine powders or dealing with high moisture content, by adjusting the design of the hopper, feeder, and air handling units.
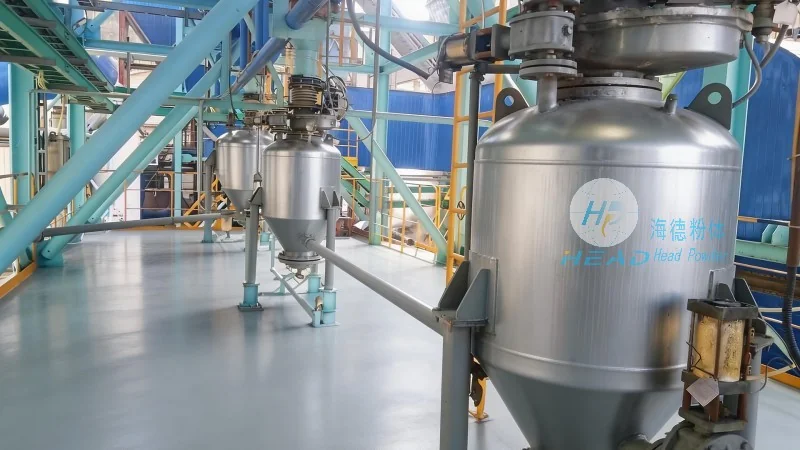
Applications and Industries Served
The pneumatic conveying equipment for sugar produced by headpowder is widely used in various stages of the sugar production and processing industry. These systems are essential in the transportation of raw sugar from storage silos to processing plants, as well as in moving refined sugar to packaging lines. They are also utilized in the handling of byproducts like molasses or sugar beet pulp, which require efficient and hygienic transport methods. The equipment is suitable for both large-scale industrial operations and smaller processing facilities, providing scalable solutions that meet the specific needs of each client. By serving a diverse range of industries, headpowder has established itself as a trusted partner for bulk material handling in the sugar sector.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd. stands as a leading provider of pneumatic conveying equipment for sugar, combining technical expertise with innovative solutions to meet the evolving needs of the industry. The company's commitment to quality, efficiency, and customer satisfaction has earned it a reputation for reliability and excellence. With a strong presence in Shandong, China, and a global reach, headpowder continues to advance the technology of sugar pneumatic conveying, ensuring that its customers can achieve optimal performance and cost-effectiveness in their bulk material handling operations. For businesses seeking to enhance their sugar processing capabilities, the principles and applications of pneumatic conveying equipment offer a robust and efficient solution.