

What is a Bulk Bag Pneumatic Conveying System? And What Are Its Design Principles?
A bulk bag pneumatic conveying system is a specialized industrial equipment designed to transport bulk materials from a storage container, such as a bulk bag or a hopper, to a processing or storage location. This system utilizes compressed air or other gases to create a flow of material through a pipeline, enabling efficient and safe material handling. The system is widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining, where handling large volumes of powders or granules is essential.
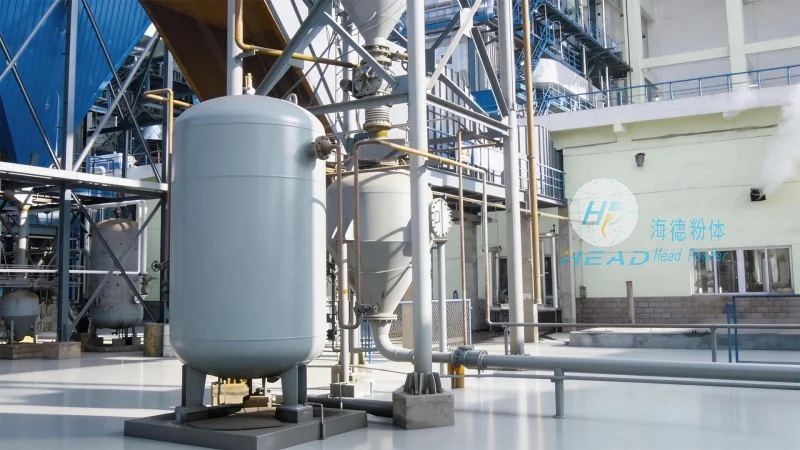
Key Components of a Bulk Bag Pneumatic Conveying System
The design of a bulk bag pneumatic conveying system involves several critical components that work together to ensure smooth operation. The main components include a bulk bag discharger, a hopper or receiving container, a conveyor line (typically a flexible or rigid pipe), a blower or air compressor, and a control system. The bulk bag discharger is responsible for opening the top of the bag and allowing the material to flow into the hopper. The hopper then feeds the material into the conveyor line, where it is propelled by the air flow generated by the blower. The control system monitors the pressure, flow rate, and other parameters to ensure optimal performance and prevent issues like blockages or overloading.
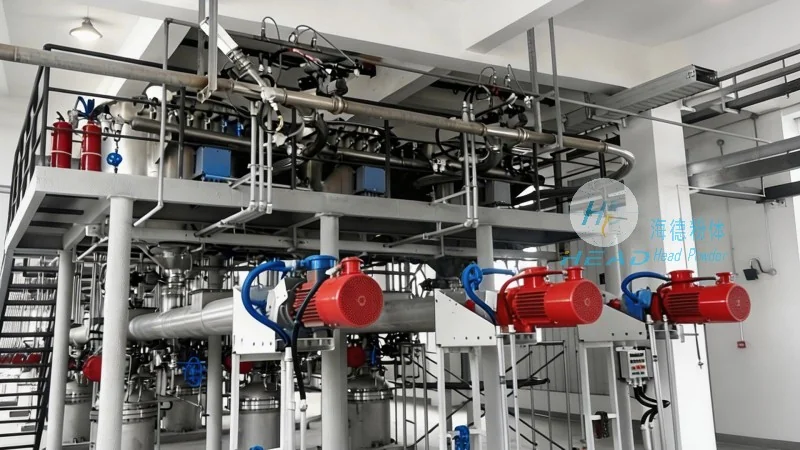
Design Principles for Efficient Bulk Bag Pneumatic Conveying
The design principles of a bulk bag pneumatic conveying system focus on maximizing efficiency, minimizing material degradation, and ensuring safety. One of the primary design considerations is the selection of the appropriate conveying method, which can be either pressure or vacuum-based. Pressure systems use a blower to push air and material through the line, while vacuum systems use a vacuum pump to draw material into the line. The choice between these methods depends on factors such as the material's properties, the distance to be conveyed, and the system's capacity. Another key design principle is the proper sizing of the conveyor line and blower, which must be matched to the material's flow characteristics to avoid excessive pressure drops or air consumption. Additionally, the system should incorporate features like filters and cyclones to separate the material from the air, ensuring that the material remains clean and free from contaminants. The control system plays a crucial role in maintaining consistent operation, with sensors and valves that adjust the air flow and pressure as needed to handle variations in material feed rate or line conditions.
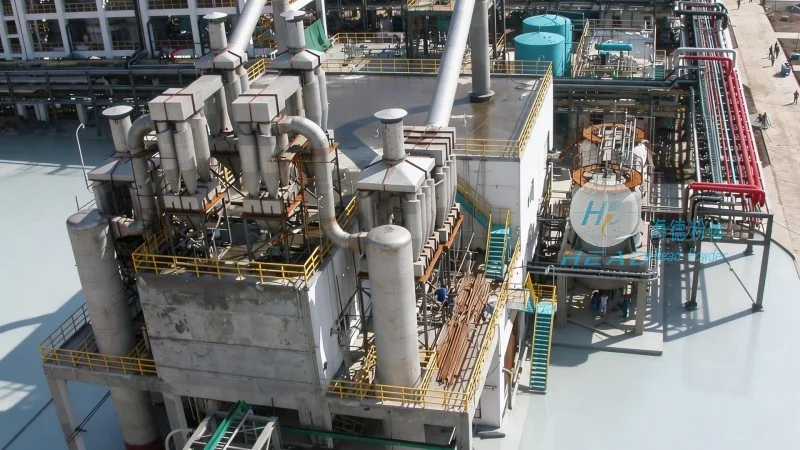
Applications and Benefits of Bulk Bag Pneumatic Conveying Systems
Bulk bag pneumatic conveying systems are used in a wide range of applications across different industries. In the food and beverage industry, they are used to transport ingredients like flour, sugar, and spices from bulk bags to processing equipment, ensuring a hygienic and efficient transfer process. In the pharmaceutical industry, these systems are essential for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where contamination control and precise dosing are critical. The chemical industry also relies on bulk bag pneumatic conveying systems to transport chemicals, powders, and granules, which may be hazardous or require specialized handling. The benefits of using such systems include improved safety by reducing manual handling of heavy or dusty materials, increased efficiency by automating the material transfer process, and cost savings by minimizing material loss and downtime. Additionally, these systems can handle a wide variety of materials, from fine powders to coarse granules, making them versatile and adaptable to different production needs.
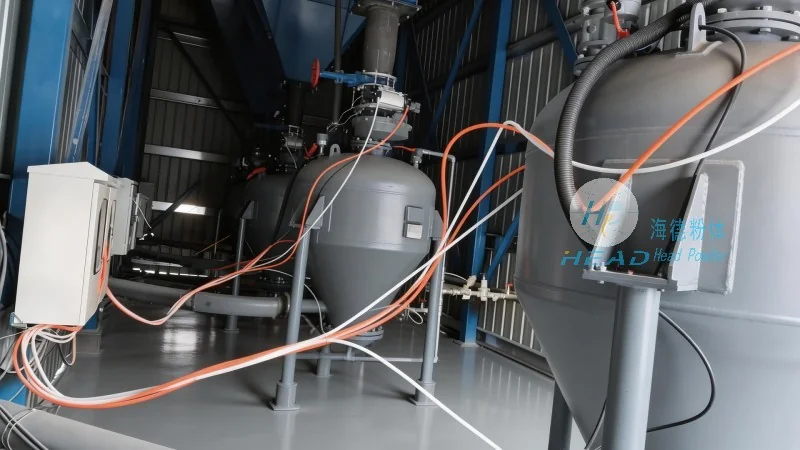
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of bulk bag pneumatic conveying systems and related industrial equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's products are designed to meet the specific needs of various industries, with a commitment to providing systems that are durable, easy to maintain, and cost-effective. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to research, development, and customer support. HeadPowder's expertise in pneumatic conveying technology ensures that its systems are built to the highest standards, with rigorous testing and quality control processes to ensure performance and reliability. Whether for new installations or system upgrades, HeadPowder offers comprehensive solutions tailored to the unique requirements of each client, helping them optimize their material handling processes and improve overall operational efficiency.