

What is a Tonne Bag Dust-Free Loading Station Pneumatic Conveying System? And What Are Its Design Pr
For industrial operations that require the safe and efficient handling of bulk materials, the tonne bag dust-free loading station with a pneumatic conveying system represents a sophisticated solution. This equipment is specifically designed to manage the transfer of materials from large bulk bags (tonne bags) into processing systems while maintaining a clean and dust-free environment. The system integrates several key components to achieve this, including a dust extraction unit, a loading hopper, and a pneumatic conveyor that transports the material to its final destination. Understanding the design principles behind this technology is crucial for industries such as food processing, pharmaceuticals, and chemical manufacturing, where contamination control is paramount.
Key Components and Their Functions
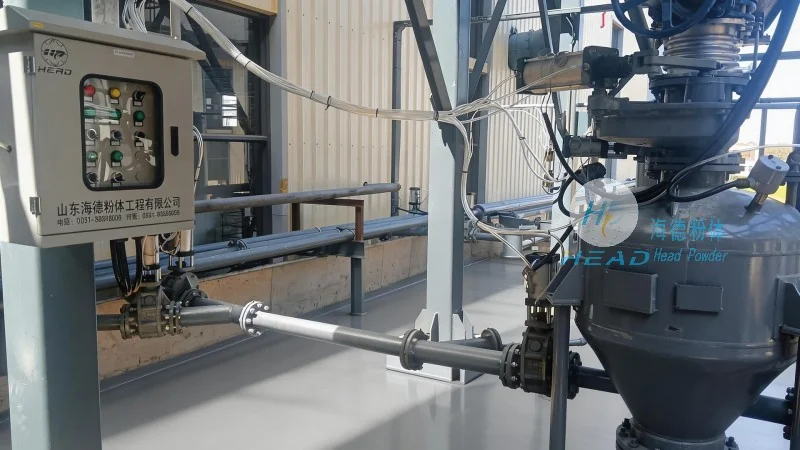
The tonne bag dust-free loading station typically consists of several interconnected parts, each playing a vital role in the overall operation. The primary components include the bulk bag unloading mechanism, a dust collection system, a loading hopper, and the pneumatic conveying pipeline. The bulk bag is placed on a frame or a lifting device, and the unloading process begins by opening the bag's top, allowing the material to flow into the hopper. Simultaneously, the dust extraction system activates, capturing any airborne particles and directing them to a filtration unit. The loading hopper then feeds the material into the pneumatic conveyor, which uses compressed air to transport the material through the pipeline to the processing equipment. The design ensures that the entire process is enclosed, minimizing the risk of dust dispersion and maintaining a safe working environment.
Design Principles and Operational Efficiency
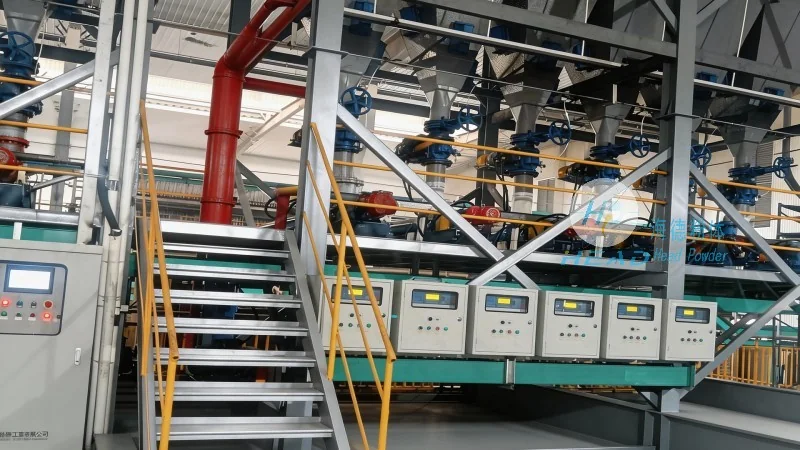
The design of a tonne bag dust-free loading station is guided by several key principles aimed at maximizing efficiency, safety, and material integrity. One of the core principles is the use of an enclosed system to prevent dust from escaping into the workspace. This is achieved through a combination of airtight connections and a negative pressure environment within the loading station. The dust extraction system is strategically placed to capture particles at the source, ensuring that the air leaving the system is clean and free from contaminants. Another important principle is the optimization of material flow, which involves the use of appropriate hopper designs and conveyor speeds to prevent blockages and ensure consistent material transfer. The system is also designed to handle a wide range of materials, from powders to granules, by adjusting the air pressure and flow rate as needed. This flexibility makes the system suitable for various industrial applications.
Advantages of Using a Tonne Bag Dust-Free Loading Station
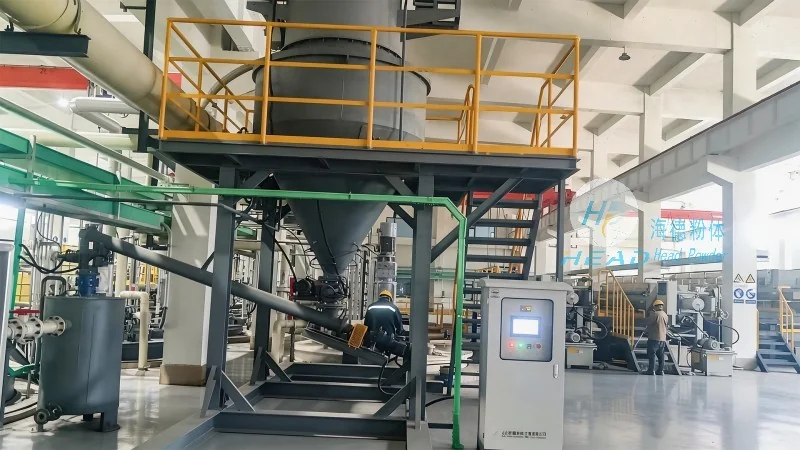
Implementing a tonne bag dust-free loading station with a pneumatic conveying system offers numerous advantages for industrial operations. Firstly, it significantly improves workplace safety by reducing the exposure of workers to dust and airborne particles. This is particularly important in industries where respiratory hazards are a concern. Secondly, the enclosed design helps maintain product quality by preventing contamination from external sources. The system also enhances operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing downtime. Additionally, the system is designed to be compact and space-efficient, making it suitable for facilities with limited floor space. The use of compressed air as the conveying medium also reduces the risk of material degradation compared to mechanical conveyors, which can cause friction and heat.
Application Examples and Industry Use Cases
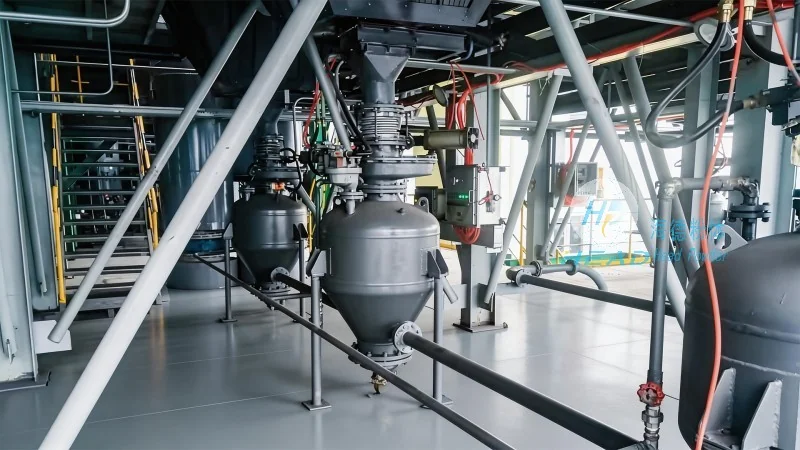
The tonne bag dust-free loading station is widely used in various industries that handle bulk materials. In the food and beverage industry, it is used to transfer ingredients such as flour, sugar, and spices into processing lines while maintaining a hygienic environment. In the pharmaceutical industry, the system is essential for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where contamination control is critical. The chemical industry also benefits from this technology when handling powders and granules, such as fertilizers or chemicals, to prevent dust explosions and ensure worker safety. Additionally, the system is used in the plastics and rubber industries for transferring raw materials into mixing and processing equipment. The versatility of the tonne bag dust-free loading station makes it a valuable asset for any industrial facility that requires efficient and safe material handling.