

What is Tonne Bag Automatic Feeding Powder Material Handling? And What Are Its Design Principles?
Understanding Tonne Bag Automatic Feeding Powder Material Handling Systems and Their Design Principles
Introduction to Tonne Bag Automatic Feeding Systems
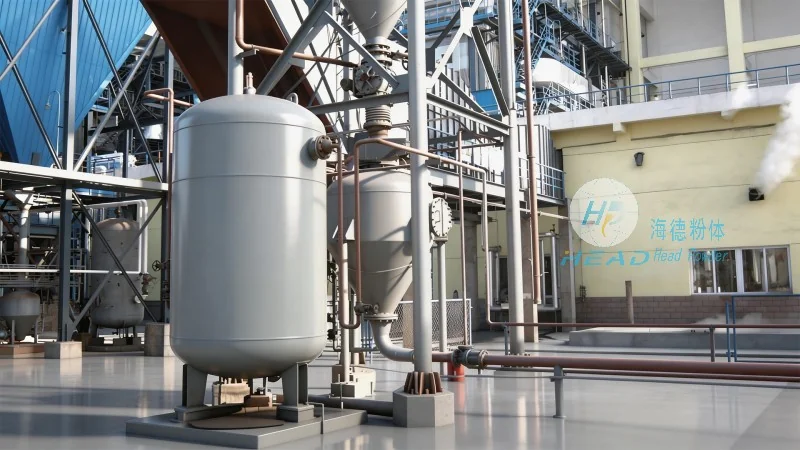
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder material handling solutions. One of their core offerings is the tonne bag automatic feeding system, a critical component for industries that rely on bulk powder processing. This system is engineered to efficiently transfer large quantities of powder from tonne bags—typically 1 tonne (1000 kg) containers—into production lines, storage silos, or processing equipment. The system addresses the challenges of manual handling, which is often labor-intensive, time-consuming, and prone to material loss or contamination.
The Core Functionality of Tonne Bag Automatic Feeding
The primary objective of a tonne bag automatic feeding system is to automate the transfer of bulk powders from sealed tonne bags into processing equipment. This process typically involves several key steps: first, the tonne bag is positioned on a loading platform or a dedicated hopper; second, the bag is opened or cut open by a mechanical or pneumatic device; third, the powder is discharged into a conveyor or a feeding hopper; and fourth, the empty bag is removed or recycled. The system is designed to handle a wide range of powders, including chemicals, food ingredients, pharmaceuticals, and industrial minerals, ensuring that the material remains intact and free from contamination throughout the transfer process.
The Design Principles Behind the Tonne Bag Automatic Feeding System
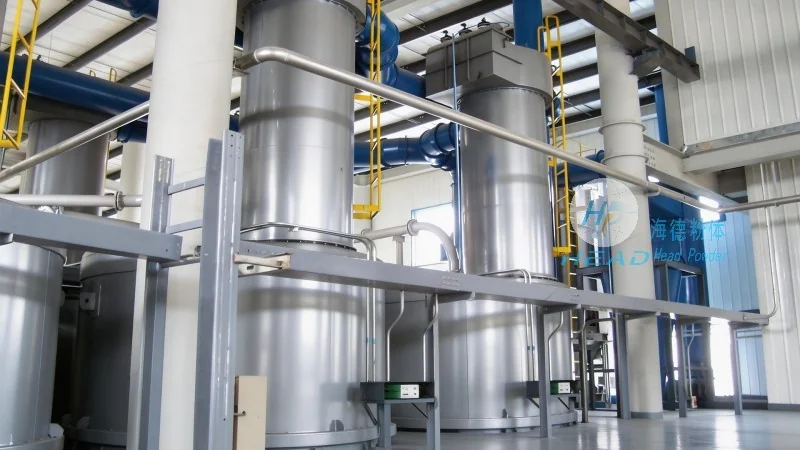
The design of a tonne bag automatic feeding system is guided by several fundamental principles to ensure efficiency, reliability, and safety. First, the system must be robust enough to handle the mechanical stresses of opening and discharging tonne bags, which can weigh up to 1000 kg and may contain abrasive or corrosive materials. This requires the use of high-quality materials, such as stainless steel or corrosion-resistant alloys, for components like the bag cutter, conveyor belts, and hoppers. Second, the system incorporates precise control mechanisms to regulate the flow rate of the powder. This is achieved through adjustable valves, variable-speed conveyors, or pneumatic regulators, which prevent overloading of downstream equipment and ensure consistent material delivery. Third, safety features are integrated to protect operators and equipment from potential hazards, such as dust explosions or material blockages. These may include dust collection systems, emergency stop buttons, and sensors that detect obstructions or overfilling.
Key Components and Their Roles
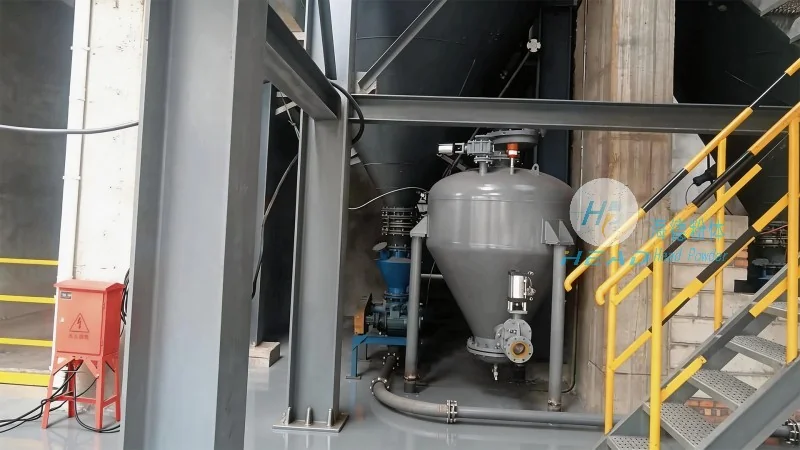
Several critical components work in tandem to make the tonne bag automatic feeding system function effectively. The bag opening mechanism is a key element, often using a rotary cutter or a pneumatic knife to safely cut through the bag's seal without damaging the powder inside. The discharge hopper or conveyor then collects the powder and transports it to the next stage of the process. A dust collection system is typically integrated to capture any airborne particles, ensuring a clean and safe working environment. Additionally, the system may include a weighing scale or a flow meter to monitor the quantity of material being transferred, which is essential for quality control and inventory management. The control panel, equipped with user-friendly interfaces and sensors, allows operators to monitor the system's performance and make adjustments as needed.
Benefits and Applications
The adoption of a tonne bag automatic feeding system offers numerous advantages for industrial operations. By automating the material handling process, companies can significantly reduce labor costs and minimize the risk of human error. The system also improves process efficiency by ensuring a consistent and continuous flow of material, which can enhance production throughput and reduce downtime. Furthermore, the automated system helps maintain product quality by preventing contamination from external sources and ensuring that the powder is handled gently, preserving its physical properties. These systems are widely used in industries such as food and beverage, pharmaceuticals, chemicals, and mining, where the handling of bulk powders is a daily operation.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of tonne bag automatic feeding systems and other powder material handling solutions. With a focus on innovation and customer satisfaction, the company designs systems that meet the specific needs of its clients, ensuring reliability, efficiency, and safety. By leveraging advanced engineering principles and high-quality components, HeadPowder delivers solutions that help industries streamline their operations and improve overall productivity. The company's commitment to quality and customer support makes it a preferred choice for businesses seeking to enhance their bulk powder handling capabilities.