

What is a Positive Pressure Dilute Phase Powder Pneumatic Conveying Equipment? And What Are Its Desi
Positive pressure dilute phase powder pneumatic conveying equipment is a specialized system designed to transport dry powders and particulate materials through a pipeline using compressed air. This technology is widely used in various industries such as food processing, pharmaceuticals, chemicals, and minerals, where the efficient and safe handling of bulk powders is critical. The system operates by generating a positive pressure within the conveying line, which propels the material from the source to the destination. Unlike negative pressure systems, positive pressure systems are generally more suitable for long-distance and high-capacity conveying due to their ability to maintain consistent pressure and prevent material leakage.
Key Design Principles of the Equipment
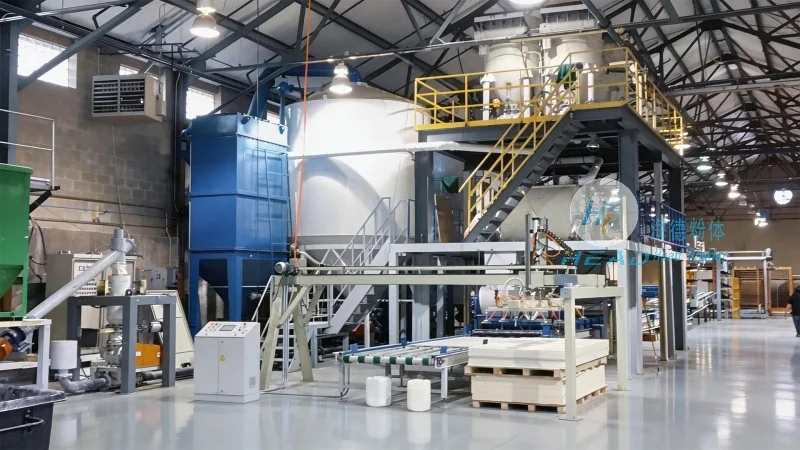
The design of positive pressure dilute phase powder pneumatic conveying equipment involves several critical principles to ensure optimal performance and reliability. First, the system must be capable of generating sufficient air pressure to overcome the resistance of the pipeline and the material being conveyed. This typically requires a high-pressure blower or compressor that can maintain a pressure of 0.5 to 1.5 bar above the ambient pressure. Second, the conveying line must be designed to minimize pressure drop and maintain a consistent flow rate. This is achieved through the use of smooth, straight pipelines with appropriate diameter and length, as well as the installation of flow control devices such as orifice plates and pressure regulators. Third, the system must incorporate proper material handling components, including feeders, cyclones, and dust collectors, to ensure the efficient separation of the conveyed material from the air stream. These components are crucial for maintaining the purity of the material and preventing contamination. Additionally, the design must consider the specific properties of the powder, such as particle size, density, and moisture content, to optimize the conveying process. For example, materials with high moisture content may require additional drying or conditioning steps to prevent caking or blockage in the pipeline.
Components and Working Mechanism
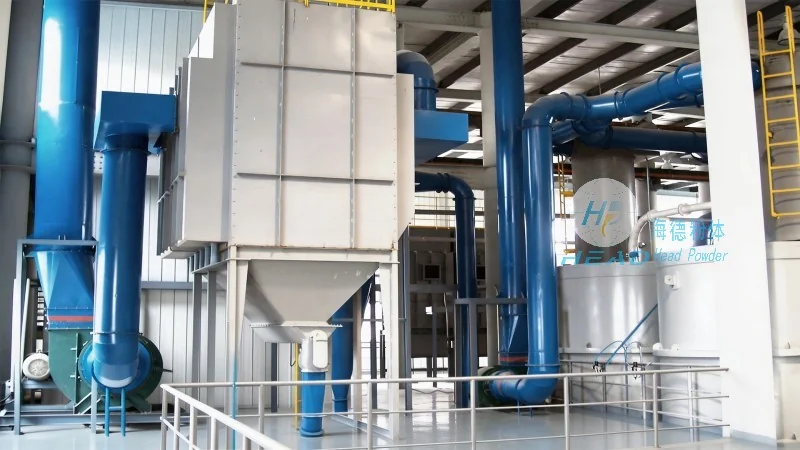
The positive pressure dilute phase powder pneumatic conveying system consists of several key components that work together to achieve the desired conveying performance. The primary components include a blower or compressor, a feeder, a conveying line, a cyclone separator, and a dust collector. The blower or compressor is responsible for generating the necessary air pressure and flow rate. It is typically a positive displacement blower or a centrifugal compressor, depending on the required pressure and flow rate. The feeder is used to introduce the powder material into the conveying line at a controlled rate. This can be a rotary valve, a screw feeder, or a pressure feeder, depending on the material properties and conveying requirements. The conveying line is a network of pipes that connects the feeder to the cyclone separator and the destination point. The line is usually made of stainless steel or other corrosion-resistant materials to prevent material degradation and ensure durability. The cyclone separator is a key component that separates the powder from the air stream. It works on the principle of centrifugal force, where the air and powder mixture enters the cyclone at a high velocity and is forced to rotate. The heavier powder particles are thrown against the inner wall of the cyclone and fall down into the collection hopper, while the air passes through the top of the cyclone and is discharged to the atmosphere. The dust collector is used to capture any fine particles that may escape from the cyclone separator and prevent them from being released into the environment. This component is typically a bag filter or an electrostatic precipitator, depending on the required filtration efficiency.
Advantages and Applications
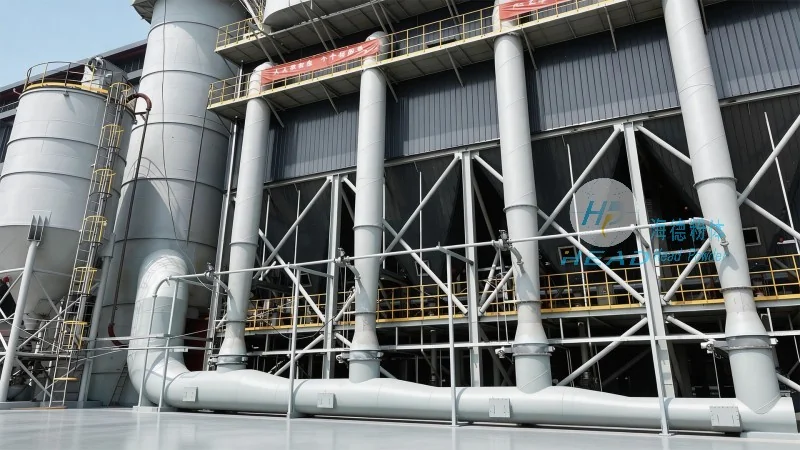
Positive pressure dilute phase powder pneumatic conveying equipment offers several advantages over other material handling methods. One of the main advantages is its ability to transport powders over long distances and at high capacities. The system can convey materials up to several kilometers with a capacity of several tons per hour, making it suitable for large-scale industrial applications. Another advantage is its flexibility in handling a wide range of powder materials, including fine powders, granules, and bulk materials. The system can also be adapted to different operating conditions, such as varying particle sizes and moisture content, by adjusting the design parameters. The equipment is also relatively easy to install and maintain, as it consists of modular components that can be easily replaced or repaired. This reduces downtime and maintenance costs for the user. In terms of applications, the positive pressure dilute phase powder pneumatic conveying system is widely used in the food industry for transporting flour, sugar, and other dry ingredients. It is also used in the pharmaceutical industry for conveying active pharmaceutical ingredients (APIs) and excipients. In the chemical industry, it is used for transporting powders such as pigments, catalysts, and chemicals. Additionally, it is used in the minerals industry for conveying ores and other bulk materials. The system is also suitable for applications where the material needs to be transported in a clean and hygienic environment, such as in the food and pharmaceutical industries.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
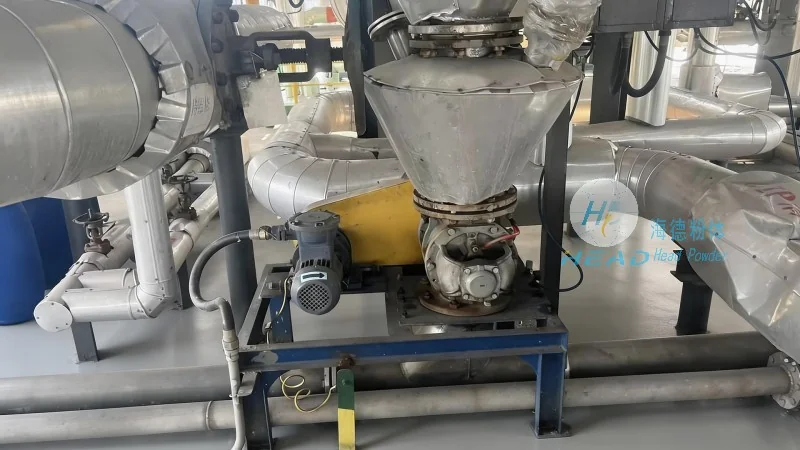
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of positive pressure dilute phase powder pneumatic conveying equipment. The company is located in Shandong, China, and has been in business for over 20 years, providing high-quality and reliable equipment to customers worldwide. HeadPowder specializes in designing and manufacturing customized conveying systems that meet the specific requirements of its clients. The company's products are known for their durability, efficiency, and ease of maintenance. HeadPowder's team of engineers and technicians has extensive experience in the field of powder handling and pneumatic conveying, and they work closely with customers to understand their needs and provide the best possible solutions. The company's equipment is widely used in various industries, including food, pharmaceuticals, chemicals, and minerals, and has earned a reputation for quality and reliability. HeadPowder is committed to providing excellent customer service and support, and it offers a range of services such as installation, maintenance, and training to its customers. The company's mission is to provide innovative and efficient solutions for powder handling and conveying, and it continues to invest in research and development to improve its products and services.