

What is a Pebble Powder Pneumatic Conveying Equipment? And What Are Its Design Principles?
For industries dealing with fine powders like pebbles, the selection of an efficient and reliable conveying system is crucial. This article delves into the world of pebble powder pneumatic conveying equipment, exploring its functionality and the underlying design principles that make it a preferred choice in various industrial applications.
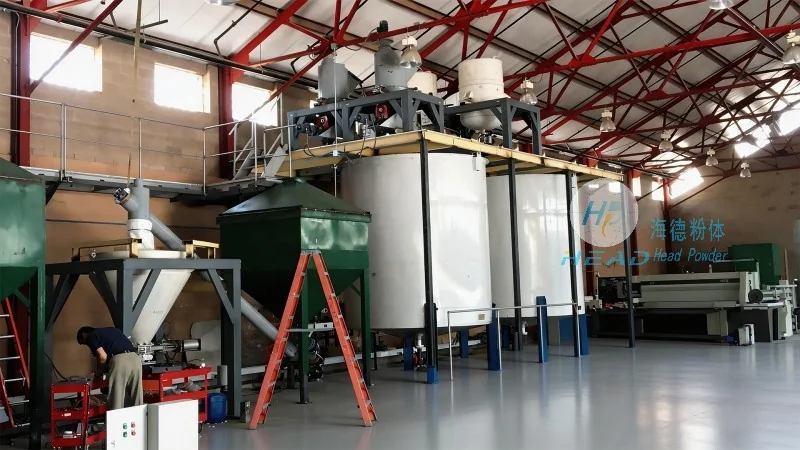
Understanding Pebble Powder Pneumatic Conveying Equipment
Pebble powder pneumatic conveying equipment is a specialized system designed to transport fine powder materials, such as pebbles, through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical conveyors, this system relies on the force of compressed air to move the material, offering several advantages in terms of flexibility, cleanliness, and reduced maintenance needs. The equipment is widely used in sectors like mining, construction, and chemical processing, where the handling of abrasive or sensitive powders requires precision and efficiency.
The Core Components and Working Principle
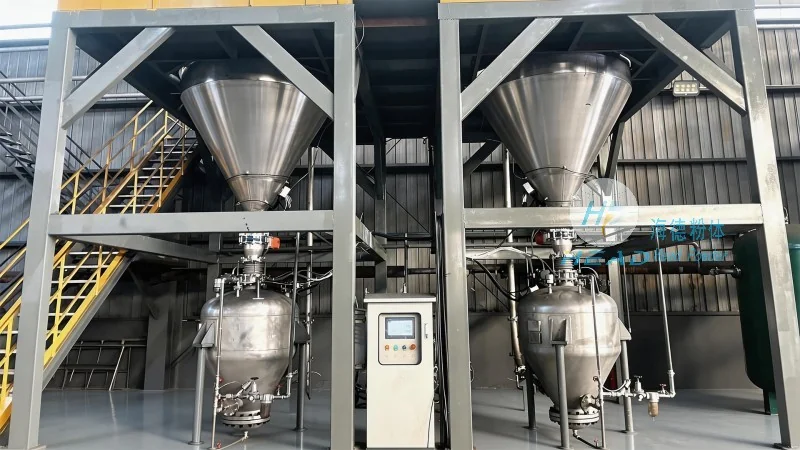
The operation of a pebble powder pneumatic conveying system involves several key components, each playing a vital role in the overall process. The primary components include a material hopper, a rotary airlock feeder, a conveying pipeline, a pressure vessel or receiver, and a dust collector. The material is first fed into the hopper, where it is then transferred to the rotary airlock feeder. This feeder controls the flow of material into the pipeline, ensuring a consistent and controlled discharge. Compressed air is then introduced into the pipeline, creating a flow that lifts and transports the pebbles through the system. The pressure vessel or receiver collects the conveyed material, while the dust collector captures any fine particles that may escape, maintaining air quality and preventing contamination.
Design Principles for Optimal Performance
The design of pebble powder pneumatic conveying equipment is based on several critical principles to ensure efficient and reliable operation. One of the key principles is the selection of appropriate air velocity, which must be high enough to overcome the gravitational forces acting on the particles but low enough to prevent excessive wear on the pipeline and components. The system's design also considers the particle size and density of the pebbles, as these factors directly impact the required air pressure and flow rate. Additionally, the pipeline layout and bends are carefully engineered to minimize pressure losses and maintain a smooth flow, reducing the risk of blockages or material degradation. The use of materials resistant to abrasion, such as stainless steel or special alloys, is essential to withstand the abrasive nature of pebble powders and extend the equipment's lifespan.
Advantages of Using Pebble Powder Pneumatic Conveying Equipment
Compared to traditional conveying methods, pebble powder pneumatic conveying equipment offers numerous benefits that make it an attractive option for many industries. One of the most significant advantages is the ability to transport materials in a closed system, which helps maintain product integrity and prevents contamination from external sources. This is particularly important for sensitive or high-value powders where cross-contamination could lead to quality issues. The system also provides flexibility in terms of layout, as the pipeline can be easily reconfigured or extended to accommodate changes in production needs or facility expansions. Furthermore, the reduced need for manual handling and the elimination of dust exposure improve workplace safety and compliance with environmental regulations. The equipment's compact design and low maintenance requirements also contribute to cost savings and operational efficiency.
Applications in Various Industries
Pebble powder pneumatic conveying equipment is versatile and finds applications in a wide range of industries. In the mining sector, it is used to transport crushed rock and ore powders from processing plants to storage or processing facilities. In construction, it helps in the efficient handling of cement, sand, and other fine aggregates, ensuring a consistent supply of materials for concrete production. The chemical industry also benefits from this equipment, as it can handle abrasive powders like limestone or silica, which are commonly used in chemical processing. Additionally, in the food and pharmaceutical industries, the closed system design ensures that the conveyed powders remain sterile and free from contamination, meeting stringent quality and safety standards.
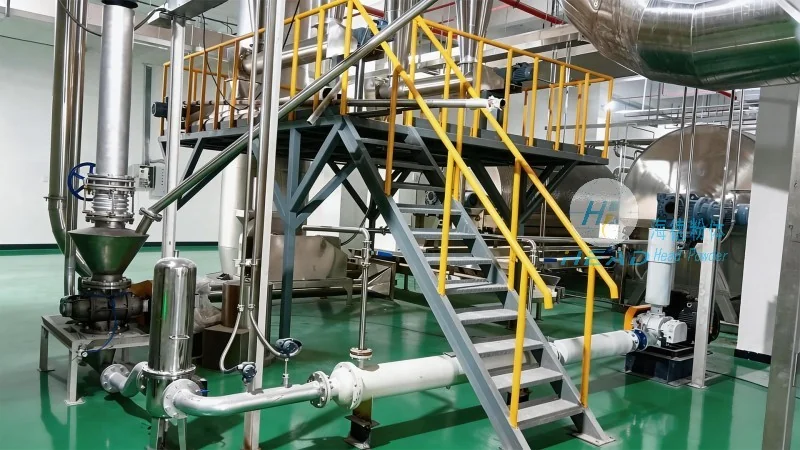
Customization and Scalability
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in designing and manufacturing customized pebble powder pneumatic conveying equipment to meet the specific needs of various industries. The company understands that each application has unique requirements, and therefore, offers tailored solutions that consider factors such as material characteristics, production capacity, and operational environment. With years of experience in the field, HeadPowder provides comprehensive engineering services, from initial design and consultation to installation and after-sales support. The company's expertise in material handling and pneumatic conveying systems ensures that clients receive equipment that is not only efficient but also durable and reliable. The equipment can be scaled to accommodate different production volumes, from small-scale operations to large industrial plants, making it suitable for a wide range of applications.
Conclusion
Pebble powder pneumatic conveying equipment is a sophisticated and efficient solution for transporting fine powder materials like pebbles. Its design, based on principles of air flow and material handling, offers numerous advantages over traditional conveying methods. By leveraging the power of compressed air, this system provides a clean, flexible, and cost-effective way to move materials in various industrial settings. As industries continue to demand higher efficiency and precision in material handling, the importance of well-designed pneumatic conveying equipment will only grow. With companies like Shandong HeadPowder Engineering Co., Ltd. leading the way in innovation and customization, the future of pebble powder pneumatic conveying looks promising, offering sustainable and reliable solutions for the evolving needs of the industry.