

Working Principle and Features of Sodium Hydrosulfite Pneumatic Conveying Equipment
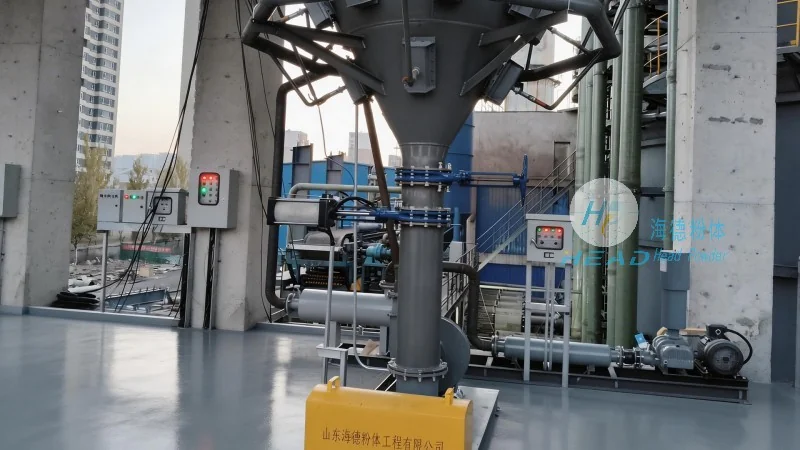
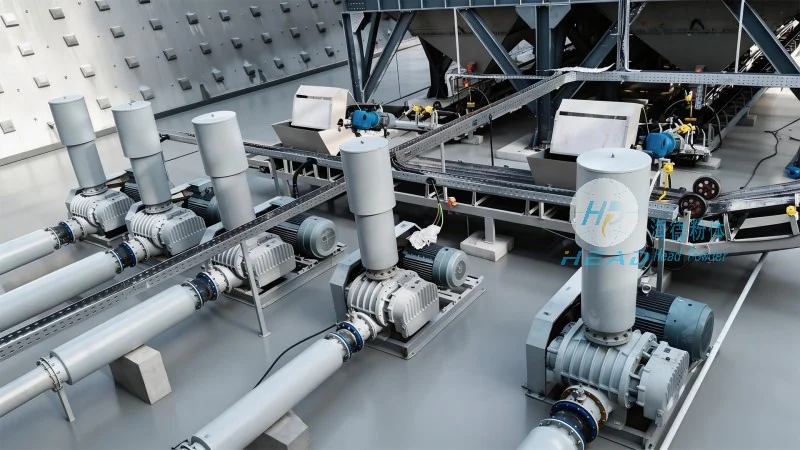
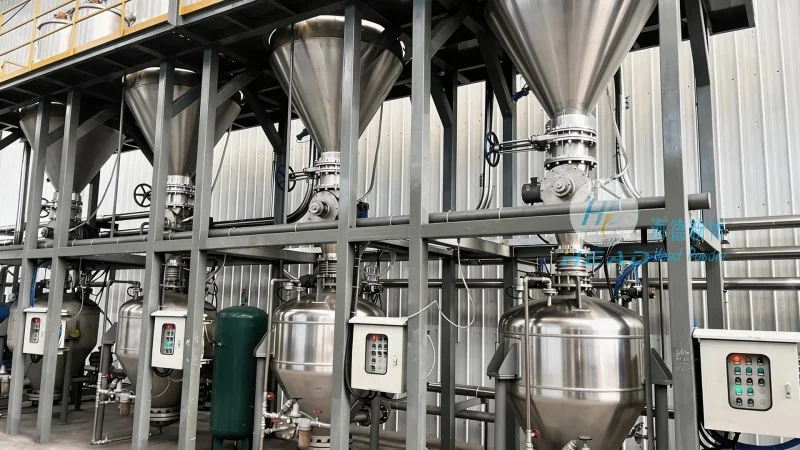
The pneumatic conveying system for sodium hydrosulfite operates on the principle of air suspension and pressure differential. The process begins with the solid material being fed into a hopper, which is equipped with a feeder mechanism to control the material flow rate. Simultaneously, a blower or compressor generates a high-pressure air stream, which is introduced into the conveying pipeline. As the air flows through the pipeline, it creates a negative pressure zone that draws the solid particles into the air stream. The solid particles are then fully suspended in the air and transported to the discharge point, where the air and material are separated. The separation is typically achieved using a cyclone or a bag filter, which captures the solid material and returns the air to the system for recirculation. This closed-loop system ensures minimal air loss and maintains the efficiency of the conveying process.
Key Features of the Pneumatic Conveying System
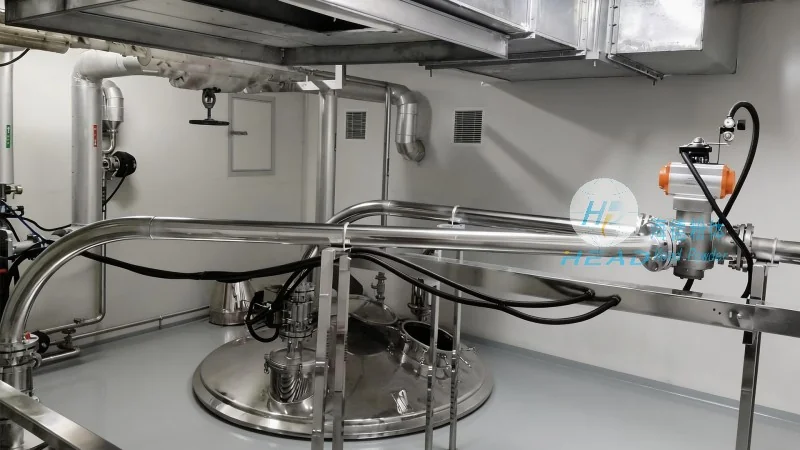
Several key features distinguish the pneumatic conveying equipment for sodium hydrosulfite. Firstly, the system is designed with a sealed and dust-tight construction to prevent the release of fine particles into the environment. This not only complies with environmental regulations but also maintains product purity, which is critical for downstream applications. Secondly, the adjustable air flow control allows operators to fine-tune the conveying rate based on the material's density, particle size, and pipeline length. This flexibility ensures optimal performance and prevents issues such as blockages or excessive pressure drops. Thirdly, the equipment incorporates corrosion-resistant materials, such as stainless steel or special alloys, to withstand the chemical properties of sodium hydrosulfite, which can be corrosive to standard metals. This design prolongs the equipment's service life and reduces maintenance costs. Additionally, the system includes monitoring and control devices, such as pressure sensors and flow meters, which provide real-time data on the conveying process. This allows for proactive maintenance and ensures that any deviations from the optimal operating conditions are detected and corrected promptly.
Application and Performance Benefits
The pneumatic conveying equipment is extensively used in the chemical manufacturing sector for transporting sodium hydrosulfite, a key intermediate in the production of dithionite-based chemicals. The system's ability to handle fine powders efficiently makes it ideal for applications where traditional methods, such as bucket elevators or belt conveyors, may cause material degradation or contamination. The high conveying efficiency of the system, typically ranging from 80% to 95% depending on the setup, minimizes material loss and reduces the need for reprocessing. This translates into significant cost savings for manufacturers. Furthermore, the sealed design of the equipment helps in maintaining a clean and safe working environment, reducing the risk of dust explosions and improving overall workplace safety. The system's reliability is another major benefit, as it operates continuously without the need for frequent stops, ensuring uninterrupted production. The consistent flow of material also enhances the quality of the final product, as it prevents segregation and ensures uniform mixing with other chemicals.
Company Information and Contact
HeadPowder Engineering Co., Ltd., a prominent enterprise based in Shandong, China, specializes in the design, manufacturing, and supply of specialized pneumatic conveying equipment. The company's commitment to innovation and quality has positioned it as a leading player in the chemical processing industry. With a team of experienced engineers and technicians, HeadPowder develops customized solutions tailored to the specific needs of clients. The company's facilities are equipped with advanced manufacturing equipment and stringent quality control measures, ensuring that each product meets the highest standards. HeadPowder's products are widely recognized for their durability, efficiency, and reliability, making them a preferred choice for chemical manufacturers worldwide. By leveraging its expertise in material handling and process engineering, HeadPowder continues to provide cutting-edge solutions that enhance operational performance and contribute to the success of its clients.