

Working Principle and Features of Powder Conveying Equipment for Food Additives
Efficient and reliable powder conveying equipment is crucial in the food industry, especially when handling food additives. This article explores the working principles and key features of such equipment, highlighting how they ensure safety, efficiency, and compliance with industry standards. The information presented is based on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field.
Working Principle of Powder Conveying Equipment for Food Additives
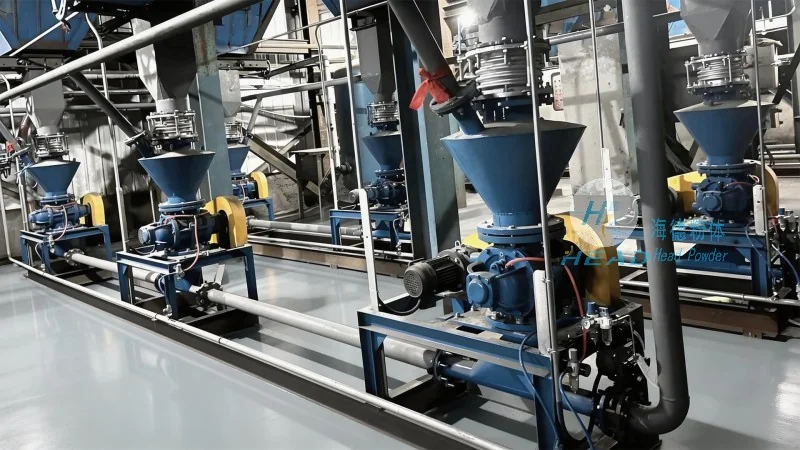
The core working principle of powder conveying equipment for food additives typically involves the transfer of dry powders from one location to another. There are several common methods employed, each with its own advantages depending on the specific application and material properties. One of the most widely used techniques is pneumatic conveying, which utilizes air pressure to move powders through a pipeline. This method is particularly effective for fine powders and can be categorized into pressure and vacuum systems. Pressure systems use compressed air to push the material forward, while vacuum systems create a negative pressure to draw the powder. Another common approach is mechanical conveying, such as screw conveyors or belt conveyors, which rely on mechanical force to move the material. These systems are often preferred for bulkier or more abrasive powders, as they provide direct contact and control over the material flow.
Key Features of Food Additive Powder Conveying Equipment
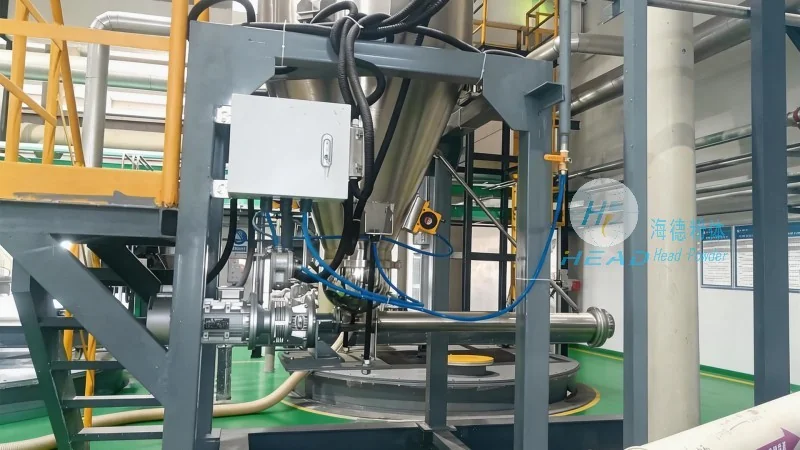
When selecting powder conveying equipment for food additives, several key features must be considered to ensure optimal performance and compliance with regulatory requirements. Firstly, the equipment must be designed to maintain the purity and integrity of the food additive. This means using materials that are non-reactive and easy to clean, such as stainless steel, to prevent contamination. Secondly, the system should offer high efficiency and low energy consumption. Advanced designs, like the ones offered by HeadPowder, incorporate optimized air flow and material handling mechanisms to reduce operational costs. Thirdly, safety features are paramount. The equipment must include explosion-proof components, dust collection systems, and proper sealing to prevent dust emissions and ensure worker safety. Additionally, the equipment should be easy to maintain and clean, with accessible components that allow for quick inspections and maintenance. Finally, the system should be flexible and adaptable to different production scales and powder types. This adaptability is crucial for food processing facilities that may need to handle various additives with different flow characteristics.
HeadPowder: A Leading Manufacturer of Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in Shandong, China, specializing in the design, manufacturing, and supply of advanced powder conveying equipment. With years of experience in the industry, HeadPowder has developed a range of solutions tailored to the specific needs of the food additive sector. The company’s products are engineered to meet stringent safety and hygiene standards, ensuring that they are suitable for handling sensitive food ingredients. HeadPowder’s team of experts works closely with clients to understand their unique requirements and provide customized solutions that enhance operational efficiency and product quality. The company’s commitment to quality and innovation has made it a trusted partner for many food processing companies worldwide.
Conclusion
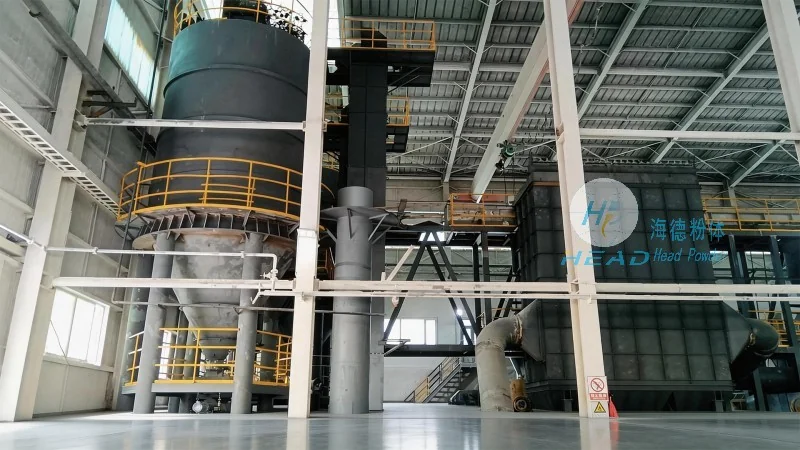
In conclusion, powder conveying equipment for food additives plays a vital role in ensuring the smooth operation of food processing facilities. Understanding the working principles and key features of such equipment is essential for selecting the right system that meets both operational and regulatory requirements. Companies like Shandong HeadPowder Engineering Co., Ltd. offer advanced solutions that combine efficiency, safety, and compliance, helping food manufacturers maintain high standards of product quality and safety. By investing in reliable powder conveying equipment, food processing facilities can enhance their productivity and ensure the consistent delivery of high-quality food additives.