

[WOKING PRINCIPLE AND FEATURES OF CENTRALIZED POWDER FEEDING AND CONVEYING SYSTEM EQUIPMENT]
Centralized powder feeding and conveying systems are essential in industrial settings where the efficient handling of bulk powders is critical. These systems are designed to streamline the process of transporting, storing, and distributing powders from a central location to various points of use within a facility. Understanding the working principle and key features of such equipment is vital for optimizing operational efficiency and ensuring product quality in industries like pharmaceuticals, food processing, and chemical manufacturing.
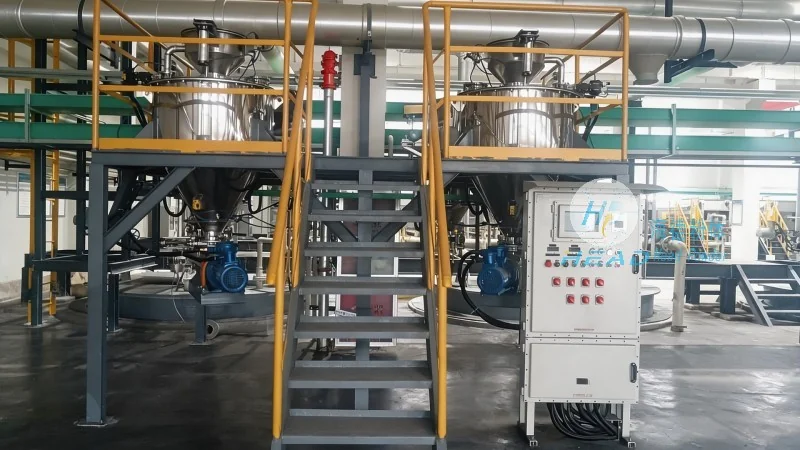
Introduction to Centralized Powder Feeding and Conveying Systems
At the core of a centralized powder feeding system is the ability to manage multiple powder sources and deliver them to different processing units or storage areas as needed. The system typically consists of several components, including hoppers, feeders, conveyors, and control panels. Each component plays a specific role in the overall operation, ensuring that powders are handled safely and efficiently.
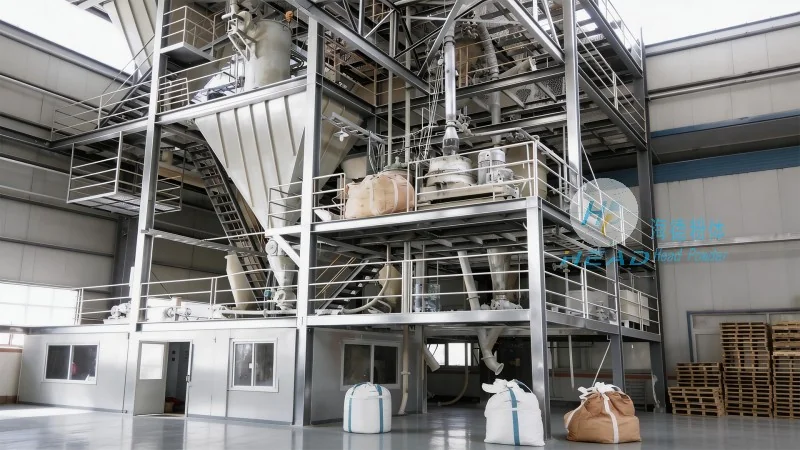
Working Principle of Centralized Powder Feeding Systems
The working principle of a centralized powder feeding system involves the following key steps: first, powders are stored in bulk hoppers or silos. Then, a feeder, such as a rotary valve or a vibratory feeder, controls the flow rate of the powder from the hopper. The feeder regulates the amount of material that is released into the conveyor system. The conveyor, which may be a pneumatic or mechanical type, transports the powder to the desired destination. Finally, the control panel monitors and adjusts the system parameters to maintain consistent performance and prevent issues like clogging or overfilling.
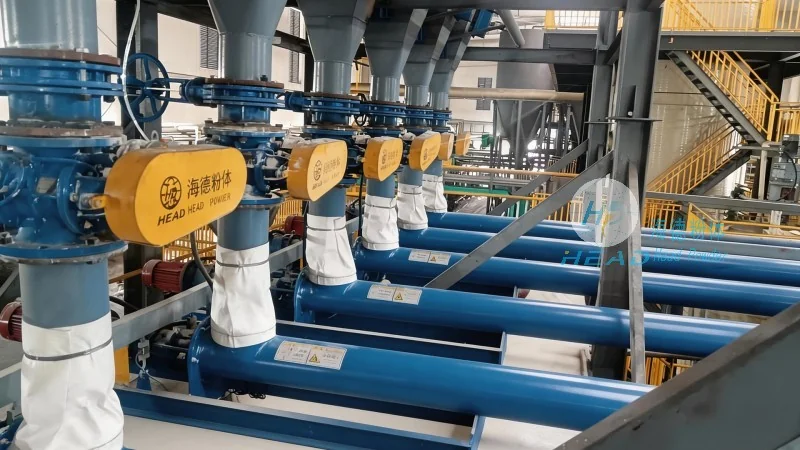
Key Features of Centralized Powder Conveying Equipment
Centralized powder conveying systems offer several advantages that make them ideal for modern industrial applications. These features include: 1. **Uniform Material Handling**: The system ensures consistent flow rates and particle size distribution, which is crucial for maintaining product quality in sensitive applications like pharmaceuticals. 2. **Space Efficiency**: By consolidating multiple feeding and conveying operations into a single system, the equipment saves valuable floor space in production facilities. 3. **Reduced Downtime**: Advanced control systems and robust construction minimize maintenance needs and downtime, leading to higher productivity. 4. **Safety and Compliance**: Many systems are designed with safety features and compliance with industry standards, such as those from the FDA or GMP, to ensure safe handling of powders in regulated environments. 5. **Scalability**: The modular design of these systems allows for easy expansion or integration with existing infrastructure as production needs grow.
Application Examples and Industry Benefits
Centralized powder feeding and conveying systems are widely used in various industries. For instance, in the pharmaceutical industry, these systems help maintain the purity and consistency of active pharmaceutical ingredients (APIs) during manufacturing. In food processing, they ensure that ingredients like flour, sugar, or spices are delivered accurately to production lines. In chemical manufacturing, the systems facilitate the handling of reactive or hazardous powders while minimizing exposure risks. The benefits of using such systems extend beyond efficiency, as they also contribute to cost savings through reduced material waste and improved process control.
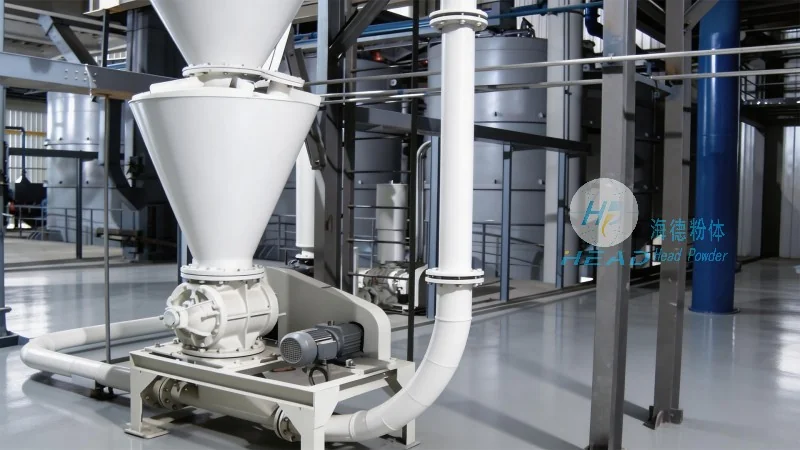
Conclusion and Company Overview
Centralized powder feeding and conveying systems are indispensable tools for modern industrial operations, offering a combination of efficiency, safety, and scalability. As demand for high-quality, consistent powder handling increases across industries, the importance of reliable and advanced conveying systems becomes more evident. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in powder handling solutions, provides customized systems designed to meet the unique requirements of various industries. With a commitment to innovation and adherence to industry standards, the company ensures that its equipment enhances operational performance, reduces downtime, and supports long-term business success. Based in Shandong, China, HeadPowder Engineering leverages years of expertise to deliver robust and efficient powder feeding and conveying systems for clients worldwide.