

Working Principle and Features of Compound Fertilizer Material Handling Systems
Compound fertilizer material handling systems are critical components in the modern fertilizer production and distribution chain. These systems are designed to efficiently transport bulk materials, such as nitrogen, phosphorus, and potassium compounds, from storage to processing units or for packaging. Understanding the working principle and key features of these systems is essential for optimizing operational efficiency and ensuring consistent product quality in fertilizer manufacturing facilities.
Working Principle of Compound Fertilizer Material Handling Systems
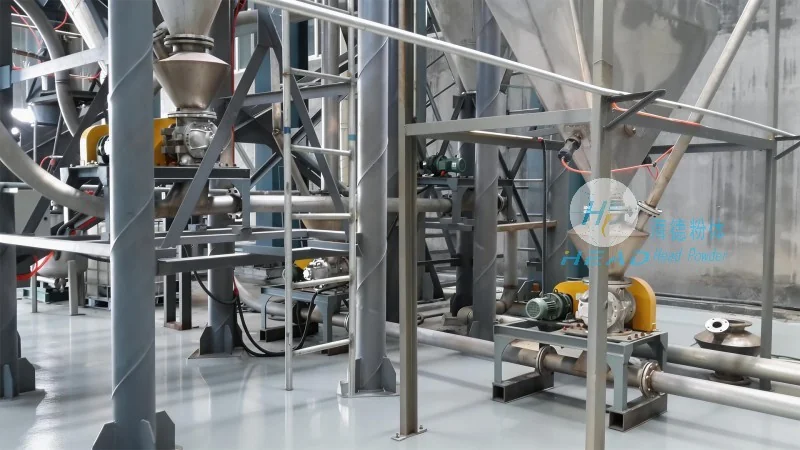
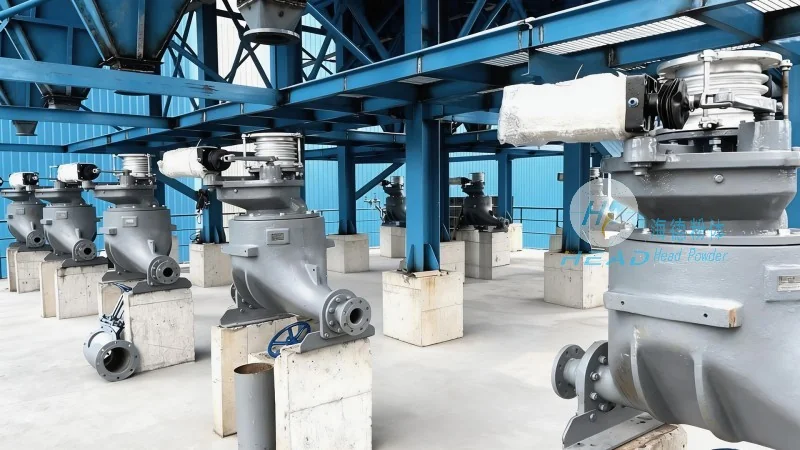
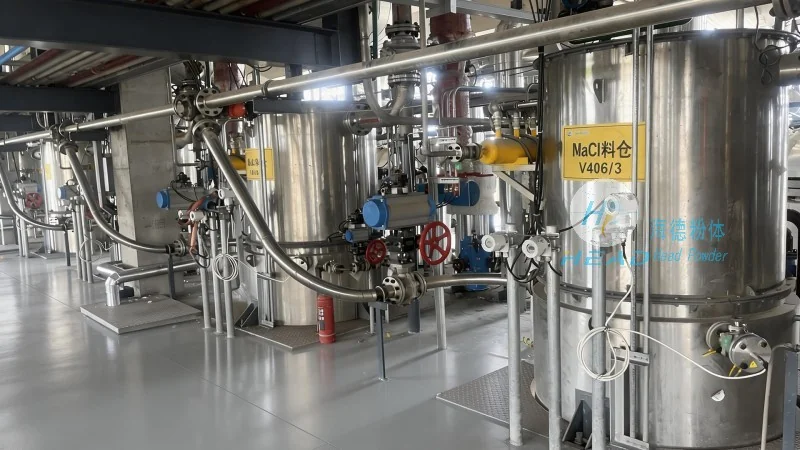
The working principle of a compound fertilizer material handling system typically involves several interconnected components that work in tandem to move and process raw materials. The process begins with the storage of raw materials, often in silos or bulk storage tanks. From there, the materials are fed into a series of conveyors or pneumatic systems that transport them to the mixing or granulation units. Key elements include material feeders, which control the flow rate of each ingredient, and conveyor belts or screw conveyors that ensure smooth movement. Pneumatic systems may also be used for transporting fine powders or granules, utilizing air pressure to move materials through pipelines. The system is often controlled by a central automation system that monitors and adjusts the flow rates, ensuring precise blending of nutrients. This automated control helps maintain the desired nutrient ratios in the final fertilizer product, which is crucial for meeting market specifications and customer requirements.
Key Features of Compound Fertilizer Material Handling Systems
Compound fertilizer material handling systems are characterized by several key features that enhance their performance and reliability. One of the primary features is the ability to handle a wide range of material types, including powders, granules, and bulk solids, with minimal degradation or segregation. This versatility is achieved through the use of specialized equipment such as rotary valves, which prevent material buildup and ensure consistent flow. Another important feature is the integration of advanced control systems, which provide real-time monitoring of material levels, flow rates, and system performance. These systems often include sensors and alarms to detect anomalies, such as blockages or overfilling, allowing for immediate corrective action. Additionally, many modern systems are designed with modular components, enabling easy maintenance and scalability. This modularity allows facilities to expand their processing capacity as demand grows without significant capital investment. The systems also prioritize safety, incorporating features like explosion-proof designs for handling potentially hazardous materials and dust suppression systems to prevent dust explosions. These safety measures are critical in fertilizer production, where dust and combustible materials are common.
About Shandong HeadPowder Engineering Co., Ltd.
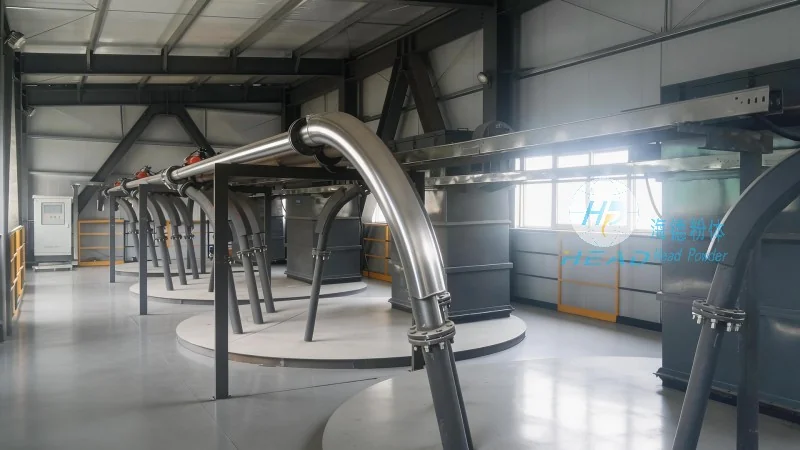
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial material handling systems, including those specifically designed for compound fertilizer production. HeadPowder is headquartered in Shandong, China, and has established a strong reputation for delivering high-quality, reliable equipment tailored to the unique needs of the fertilizer industry. The company’s expertise lies in designing and manufacturing systems that enhance operational efficiency, reduce downtime, and improve product consistency. With a focus on innovation and customer satisfaction, HeadPowder provides comprehensive solutions, from initial design and engineering to installation and after-sales support. The company’s facilities in Shandong are equipped with advanced manufacturing capabilities, ensuring that each system is built to meet international standards and customer specifications. HeadPowder’s commitment to quality and service has made it a trusted partner for fertilizer manufacturers worldwide, helping them optimize their material handling processes and achieve their production goals.