

Principle and Working Scene Characteristics of Rice Bran Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for various industrial applications. This article focuses on the rice bran pneumatic conveying system, detailing its operational principles and the specific working environments where it excels.
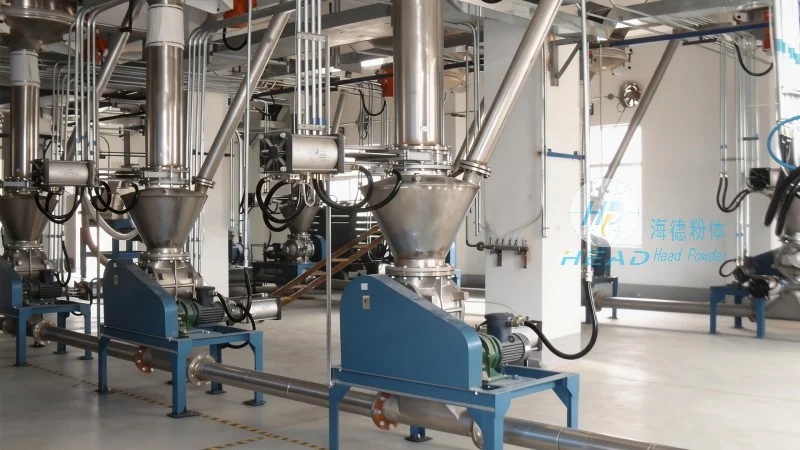
Company Overview and Expertise
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to providing innovative solutions in material handling and processing. With a strong presence in Shandong, China, the company leverages decades of industry experience to develop efficient and reliable systems tailored to customer needs. The company's commitment to quality and technical excellence ensures that each project is executed with precision, meeting the highest standards in the industry.
Introduction to Rice Bran Pneumatic Conveying Systems
Rice bran, a byproduct of rice milling, is rich in nutrients and widely used in food, feed, and industrial applications. Efficient and hygienic handling of rice bran is crucial for maintaining product quality and ensuring operational efficiency. Pneumatic conveying systems offer a solution by transporting the material through an enclosed pipeline using air pressure, eliminating the need for open chutes and reducing contamination risks.
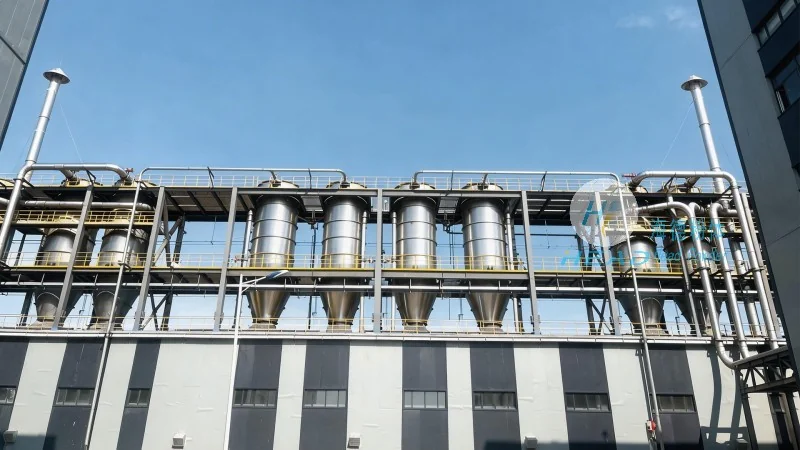
Principle of Pneumatic Conveying
The core principle of pneumatic conveying involves the use of compressed air to move bulk materials like rice bran through a pipeline. In a typical system, the rice bran is introduced into a hopper, where it is fed into the conveying line under controlled air pressure. The air flow creates a positive pressure or negative pressure environment, depending on the system design, to transport the material from the source to the destination. This method ensures a continuous, dust-free, and hygienic transfer of the material, which is particularly important for food-grade applications.
Working Scene Characteristics
The rice bran pneumatic conveying system is designed to operate in diverse industrial settings, including food processing plants, feed mills, and biofuel production facilities. Its adaptability to different working environments is a key feature, as it can be integrated into existing production lines or used as a standalone system. The system's ability to handle varying material flow rates and particle sizes makes it suitable for both small-scale and large-scale operations.
Key Advantages in Working Scenarios
In industrial applications, the rice bran pneumatic conveying system offers several advantages that enhance operational performance. Firstly, it provides a hygienic and dust-free transfer, which is essential for maintaining product quality and compliance with food safety regulations. Secondly, the system reduces labor costs by automating the material handling process, minimizing manual intervention and associated risks. Additionally, the enclosed pipeline design prevents material spillage and contamination, improving overall plant cleanliness and safety.
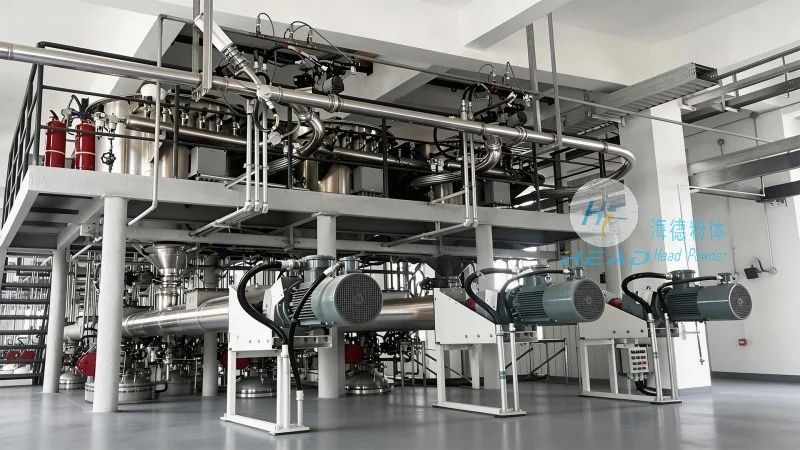
Application Examples and Operational Efficiency
HeadPowder's rice bran pneumatic conveying systems have been successfully implemented in various working scenarios, demonstrating their effectiveness in improving production efficiency. For instance, in a food processing plant, the system efficiently transports rice bran from the milling area to the storage silos, ensuring a smooth workflow and reducing downtime. In feed mills, the system enhances the mixing process by delivering rice bran to the mixing tanks at a consistent rate, optimizing the feed formulation. The system's reliability and low maintenance requirements further contribute to its widespread adoption in industrial settings.
Conclusion and Future Prospects
HeadPowder Engineering Co., Ltd. continues to innovate in the field of pneumatic conveying systems, focusing on developing solutions that meet the evolving needs of the industry. The rice bran pneumatic conveying system exemplifies the company's commitment to providing efficient, reliable, and hygienic material handling solutions. As industries increasingly prioritize sustainability and operational efficiency, such systems will play a crucial role in optimizing production processes and maintaining product quality. With its expertise and dedication to customer satisfaction, HeadPowder remains a trusted partner for businesses seeking advanced material handling solutions.