

Principle and Working Scene Characteristics of Tote Bag Powder Conveyors
For industrial operations that require efficient and reliable powder handling, the tote bag powder conveyor system has emerged as a critical solution. This equipment is designed to facilitate the seamless transfer of bulk powders from storage containers to processing units, ensuring minimal loss and maximum operational efficiency. The following sections will explore the fundamental principles behind these systems and highlight the key working scene characteristics that make them indispensable in various industrial applications, as offered by Shandong HeadPowder Engineering Co., Ltd.
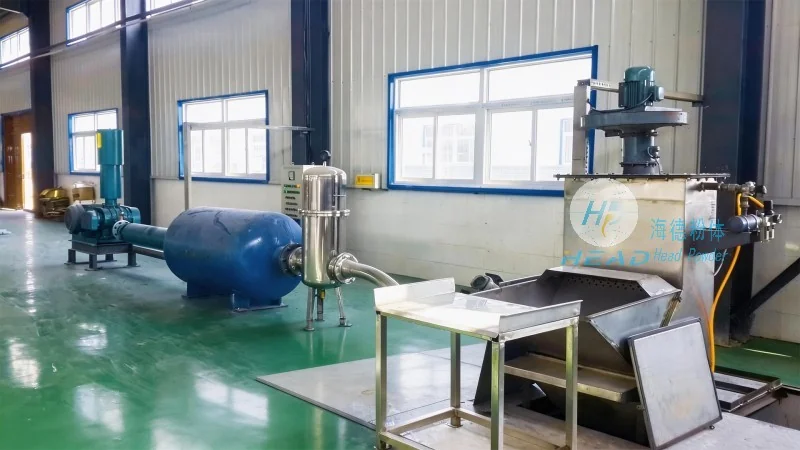
Understanding the Core Principles of Tote Bag Powder Conveyors
The tote bag powder conveyor operates on a simple yet effective principle: it uses a combination of mechanical components to lift, transport, and discharge bulk powders from tote bags. Typically, the system comprises a hopper that receives the powder from the tote bag, a conveyor mechanism (such as a screw or pneumatic system) that moves the material, and a discharge outlet that delivers the powder to the next stage of the process. The design emphasizes durability and adaptability, allowing it to handle a wide range of powder types, including fine powders, granules, and even cohesive materials. The mechanical design minimizes the risk of material degradation or contamination, which is crucial for industries where product quality is paramount. As a manufacturer specializing in bulk material handling solutions, Shandong HeadPowder Engineering Co., Ltd. has refined these principles to ensure optimal performance across diverse industrial needs.
Key Working Scene Characteristics of Tote Bag Powder Conveyors
One of the most notable characteristics of tote bag powder conveyors is their versatility in application. These systems are widely used in sectors such as pharmaceuticals, food processing, chemical manufacturing, and mining, where the handling of bulk powders is a daily necessity. The working scene characteristics that define their effectiveness include:
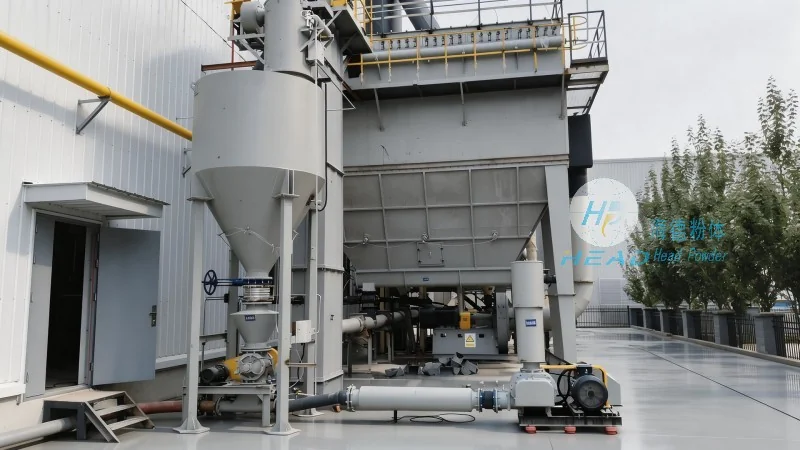
1. **Space Efficiency**: Tote bag powder conveyors are designed to optimize floor space, making them ideal for facilities with limited room. The compact design allows for easy integration into existing production lines without requiring extensive modifications.
2. **Low Maintenance Requirements**: The robust construction of these systems ensures long-term reliability with minimal downtime. Regular maintenance is straightforward, and the components are easily accessible, reducing the overall operational costs for businesses.
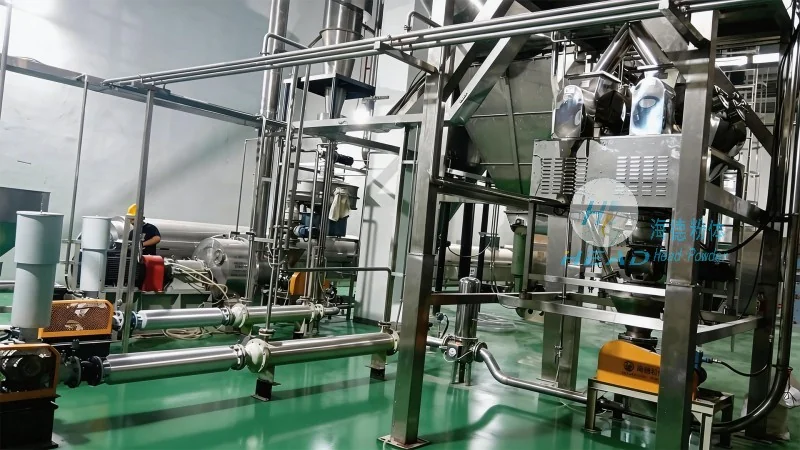
3. **Safety and Hygiene Compliance**: In industries like food and pharmaceuticals, where hygiene is non-negotiable, tote bag powder conveyors are engineered to meet stringent safety and sanitary standards. The system features sealed components that prevent cross-contamination and easy cleaning procedures that maintain a clean environment.
4. **Versatility in Material Handling**: The ability to handle diverse powder types, from fine powders that require gentle handling to bulkier granules, makes these conveyors a flexible solution for various production needs. This adaptability reduces the need for multiple types of equipment, streamlining operations.
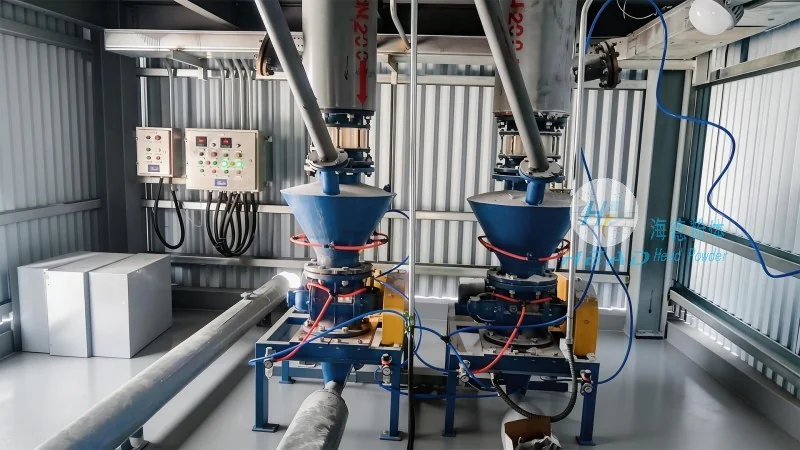
Application Scenarios and Operational Benefits
Real-world applications of tote bag powder conveyors showcase their practical advantages. For instance, in a pharmaceutical manufacturing plant, these systems are used to transfer raw materials from tote bags to mixing and processing equipment, ensuring a consistent and controlled flow of ingredients. In a food processing facility, the conveyors help maintain the quality and safety of ingredients by preventing dust and contamination during transfer. The operational benefits extend beyond efficiency; they also contribute to cost savings by reducing material waste and improving overall productivity. Shandong HeadPowder Engineering Co., Ltd. has tailored these systems to meet the specific demands of such industries, ensuring that clients achieve maximum value from their investment.
Conclusion: The Role of Tote Bag Powder Conveyors in Modern Industrial Operations
As industrial processes continue to evolve, the tote bag powder conveyor remains a vital component in the efficient handling of bulk powders. The combination of its fundamental principles and working scene characteristics makes it an indispensable tool for businesses seeking to enhance their operational efficiency while maintaining high standards of quality and safety. By understanding these aspects, industries can make informed decisions about integrating such systems into their production workflows, ultimately leading to improved performance and competitive advantages. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing advanced and reliable tote bag powder conveyor solutions that meet the evolving needs of modern industry.