

Principles and Working Scene Characteristics of Cereal Powder Conveying Machines
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of efficient conveying systems tailored for handling cereal powders. This article delves into the fundamental principles behind these machines and explores the diverse working environments where they are commonly employed, providing a comprehensive overview for industry professionals and potential clients.
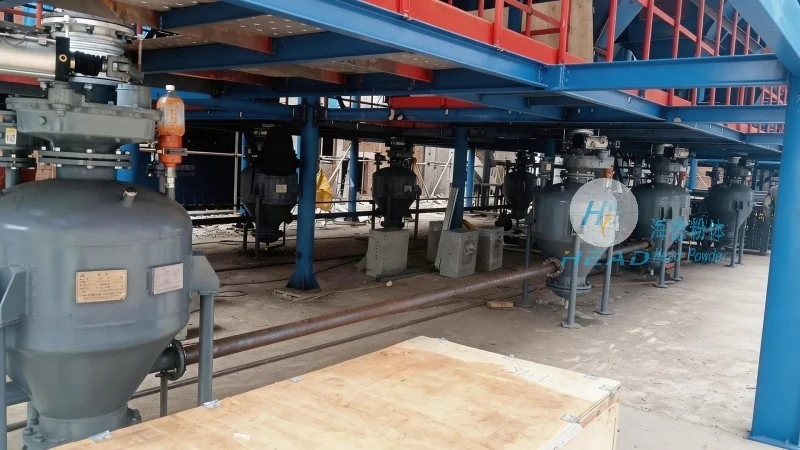
Principles of Cereal Powder Conveying Machines
The core principle of cereal powder conveying machines lies in their ability to transport bulk powder materials, such as cereal powders, from one location to another with minimal loss and maximum efficiency. These systems typically utilize mechanical components like screws, belts, or pneumatic mechanisms to move the powder through pipelines or containers. The design of the conveying mechanism is crucial as it must accommodate the specific properties of cereal powders, including their flowability, density, and potential for caking or segregation. For instance, some machines employ auger screws with variable pitch to control the speed and pressure of the powder flow, ensuring smooth and consistent transport. Additionally, the use of sealed systems prevents contamination and dust dispersion, which is critical in food processing applications where hygiene standards are paramount.
Working Scene Characteristics of Cereal Powder Conveying Machines
Cereal powder conveying machines are widely used in various industrial settings, each with distinct characteristics that influence their operational requirements. In food processing facilities, these machines are essential for transferring raw materials like oatmeal, cornflour, or wheat powder from storage silos to production lines. The working environment in such settings often involves high volumes of material and strict regulatory compliance, making the reliability and durability of the conveying equipment a top priority. For example, in a large-scale breakfast cereal manufacturing plant, the conveying system must handle thousands of tons of powder annually while maintaining consistent quality and preventing cross-contamination between different product lines.
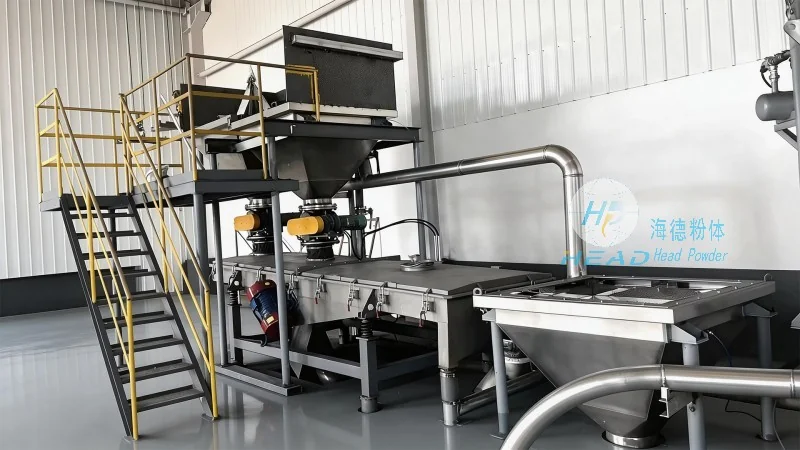
Application Examples in Different Industries
Beyond the food industry, cereal powder conveying machines find applications in pharmaceuticals, chemical manufacturing, and agricultural sectors. In pharmaceutical production, the machines are used to transport raw powders for drug formulations, where precision and cleanliness are non-negotiable. The sealed design and material compatibility with food-grade standards are often adapted to meet the stringent requirements of the pharmaceutical industry. Similarly, in chemical plants, these systems handle various powdered chemicals, ensuring safe and efficient material transfer while minimizing dust exposure and environmental impact. The adaptability of the conveying mechanisms, such as adjustable screw speeds and variable flow rates, allows them to accommodate different powder types and processing needs across these diverse industries.
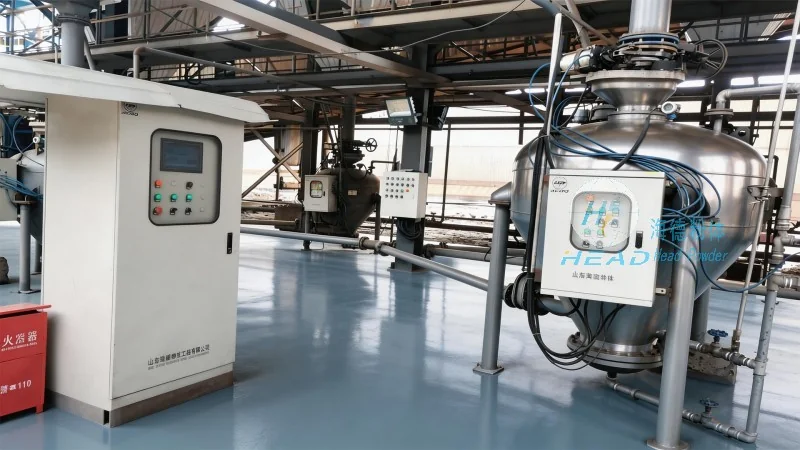
Key Features and Advantages
HeadPowder's cereal powder conveying machines are engineered with several key features that enhance their performance and reliability. One of the primary advantages is the use of robust, corrosion-resistant materials, such as stainless steel, to ensure durability in harsh operating conditions. The machines are also equipped with advanced control systems that allow for real-time monitoring of flow rates, pressure, and temperature, enabling operators to optimize performance and prevent equipment failures. Additionally, the modular design of the systems facilitates easy maintenance and replacement of components, reducing downtime and operational costs. These features collectively contribute to the high efficiency and long service life of the conveying equipment, making them a preferred choice for businesses in the cereal processing industry.
Conclusion and Company Information
HeadPowder Engineering Co., Ltd., located in Shandong, China, is committed to providing innovative and reliable conveying solutions for cereal powder handling. By understanding the unique challenges of powder transport, our team designs machines that balance efficiency, safety, and cost-effectiveness. Whether used in food processing, pharmaceuticals, or chemical manufacturing, our conveying systems are built to meet the demands of modern industrial operations. For businesses seeking to enhance their material handling capabilities, HeadPowder offers tailored solutions that ensure smooth and consistent powder transport, supporting productivity and compliance with industry standards.