

Principle and Working Scene Characteristics of Cement Raw Material Powder Conveying Machine
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder conveying systems tailored for the cement industry. Among their core offerings is the cement raw material powder conveying machine, a critical piece of equipment that ensures efficient and reliable transport of raw materials in cement production processes. This article delves into the fundamental principles behind this equipment and highlights its key working scene characteristics, providing insights into its practical applications and operational advantages.
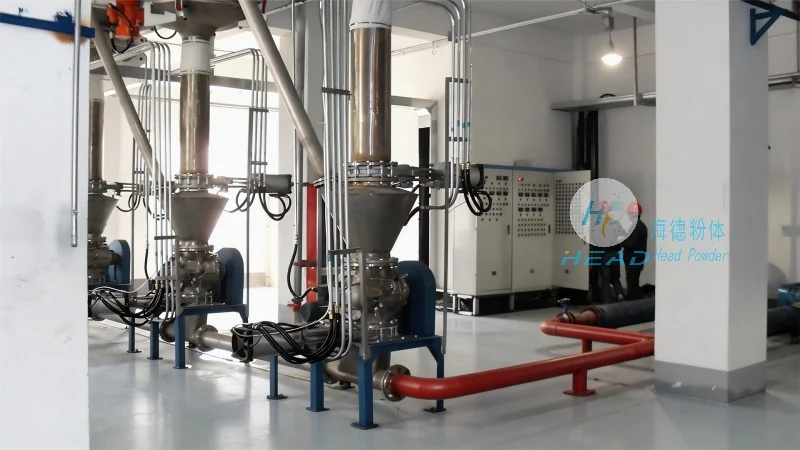
Cement Raw Material Powder Conveying Machine: Core Principles and Operational Scene Features
The cement raw material powder conveying machine operates on the principle of pneumatic or mechanical powder transport, depending on the specific design and material properties. For cement raw materials, which often include limestone, clay, and other minerals, the machine is engineered to handle fine powders with high efficiency. The primary mechanism involves the use of air or mechanical force to move the powder from a storage silo or hopper to the cement production line. Pneumatic conveying systems, for instance, utilize compressed air to create a flow that carries the powder through pipelines, while mechanical systems such as screw conveyors or bucket elevators rely on rotating components to transport the material. The choice of mechanism depends on factors like material moisture content, particle size, and the required conveying distance. HeadPowder’s machines are designed to optimize these parameters, ensuring minimal material degradation and maximum throughput.
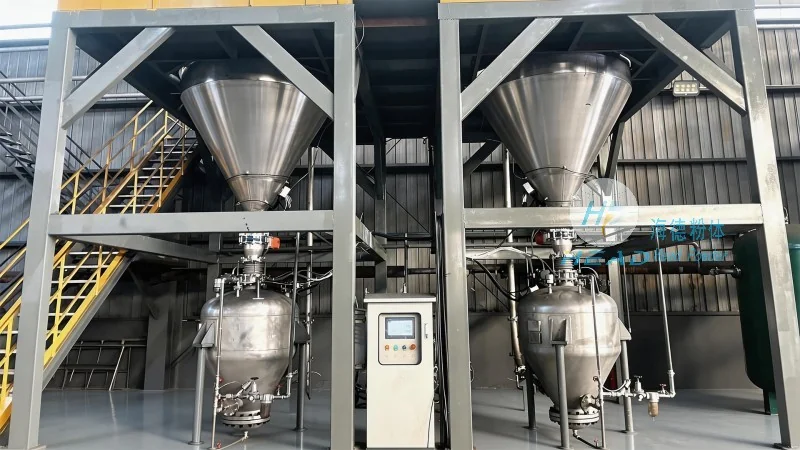
Key Working Scene Characteristics and Applications
The cement raw material powder conveying machine is widely used in various industrial settings, particularly in cement manufacturing plants where large volumes of raw materials need to be transported over considerable distances. Its working scene characteristics are tailored to meet the demands of these environments, including high dust control, energy efficiency, and durability. In cement plants, the machine is typically integrated into the raw material preparation stage, where it connects the raw material storage silos to the grinding and mixing units. The equipment is designed to handle the abrasive nature of cement raw materials, with components such as wear-resistant liners and robust drive systems that ensure long-term reliability. Additionally, the machine’s ability to operate in a closed system minimizes dust emissions, contributing to a cleaner and safer working environment. HeadPowder’s solutions are often customized to match the specific layout and operational requirements of each plant, ensuring seamless integration with existing infrastructure.
Operational Advantages and Performance Metrics
When deployed in the cement industry, the cement raw material powder conveying machine offers several operational advantages that enhance overall production efficiency. These include consistent material flow, reduced downtime due to maintenance, and improved safety through enclosed systems. Performance metrics such as conveying capacity, pressure drop, and energy consumption are carefully optimized in HeadPowder’s designs. For example, the company’s pneumatic conveying systems can achieve high conveying rates while maintaining low pressure drops, which reduces energy costs and extends the lifespan of the conveying lines. Mechanical systems, on the other hand, provide reliable performance in environments where air quality is a concern, as they do not generate dust during operation. The combination of these features makes the cement raw material powder conveying machine an indispensable tool for modern cement production, enabling manufacturers to meet high production targets while adhering to environmental regulations.
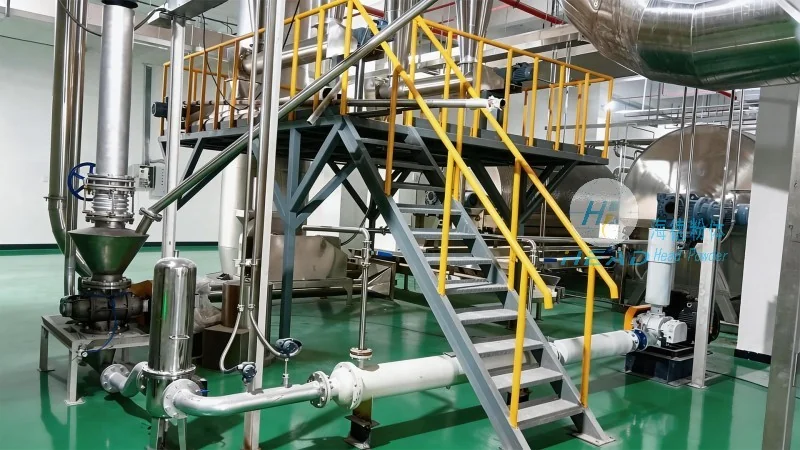
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd. is a professional engineering company headquartered in Shandong, China. With years of experience in the powder handling industry, the company specializes in the research, development, and manufacturing of advanced conveying and processing equipment. HeadPowder’s commitment to innovation and quality has made it a trusted partner for clients in the cement, chemical, and food industries. The company’s products are designed to meet international standards and are backed by comprehensive technical support and after-sales services. By leveraging advanced engineering and customer-centric solutions, HeadPowder continues to deliver high-performance equipment that enhances operational efficiency and sustainability in industrial applications.