

Principle and Working Scene Characteristics of Dry Cobblestone Material Conveying Systems
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. This article explores the core principles and operational characteristics of dry cobblestone material conveying systems, highlighting their applications and technical advantages.
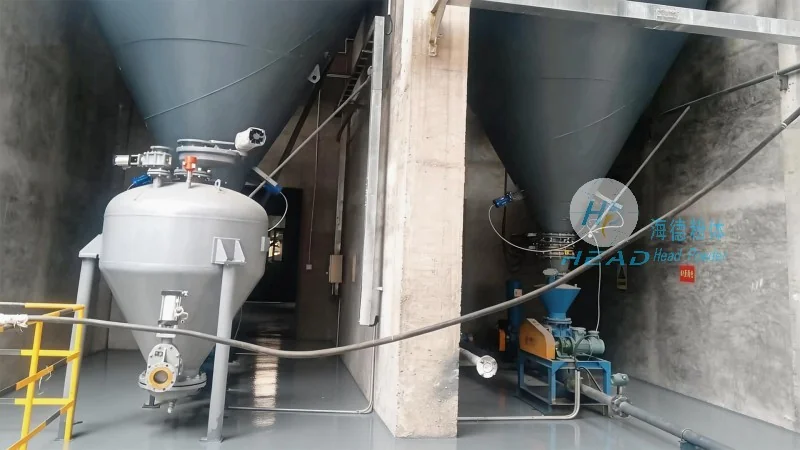
Understanding the Core Principle of Dry Cobblestone Material Conveying Systems
Dry cobblestone material conveying systems are engineered to efficiently transport dry, irregularly shaped materials such as cobblestones, gravel, and other bulk materials. The primary principle behind these systems involves the use of specialized conveyor mechanisms that can handle the unique physical properties of dry cobblestones, including their size variability and abrasive nature. Unlike traditional conveyor systems, which may struggle with such materials, dry cobblestone conveyors are designed with robust components and advanced control systems to ensure smooth and reliable operation. The system typically comprises a series of components, including feed hoppers, conveyor belts or chains, idlers, and drive units, all working in tandem to move the material from one location to another. The key to their effectiveness lies in the integration of heavy-duty materials and precise engineering, which minimizes wear and tear while maximizing throughput. HeadPowder's expertise in material handling technology ensures that these systems are optimized for durability and efficiency, making them suitable for demanding industrial environments.
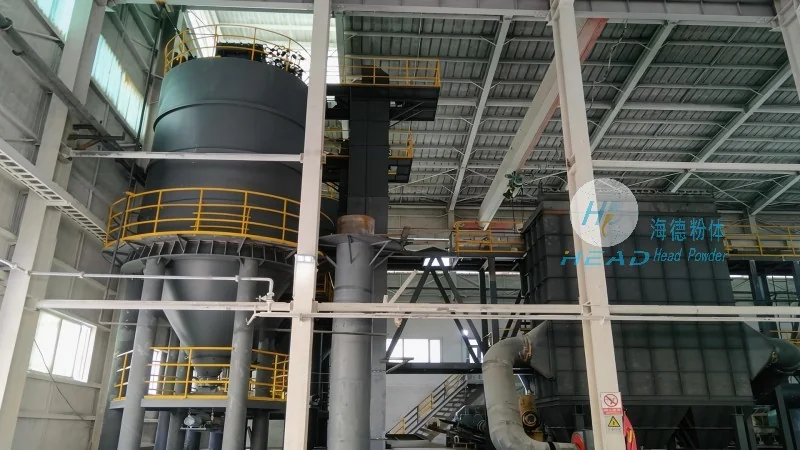
Key Working Scene Characteristics of Dry Cobblestone Material Conveying Systems
The operational characteristics of dry cobblestone material conveying systems are tailored to specific industrial applications, where the efficient movement of bulk materials is critical. These systems are commonly used in construction sites, where large quantities of cobblestones are required for paving and landscaping projects. The ability to handle irregularly shaped materials without causing damage or blockages is a significant advantage, as it allows for seamless integration into existing workflows. In addition, these systems are often employed in recycling facilities, where dry cobblestones are processed and reused in new construction projects. The consistent and controlled flow of material ensures that the recycling process is efficient and cost-effective. Another important application is in the mining and quarrying industry, where dry cobblestones are extracted and transported to processing plants. The robust design of these conveyors enables them to withstand the harsh conditions of mining operations, including dust, debris, and temperature fluctuations. Furthermore, the systems are adaptable to various operational scales, from small-scale projects to large industrial operations, making them versatile for different production needs. HeadPowder's systems are designed to meet the specific requirements of each working scene, ensuring optimal performance and minimal downtime.
Technical Advantages and Performance Metrics of Dry Cobblestone Conveying Systems
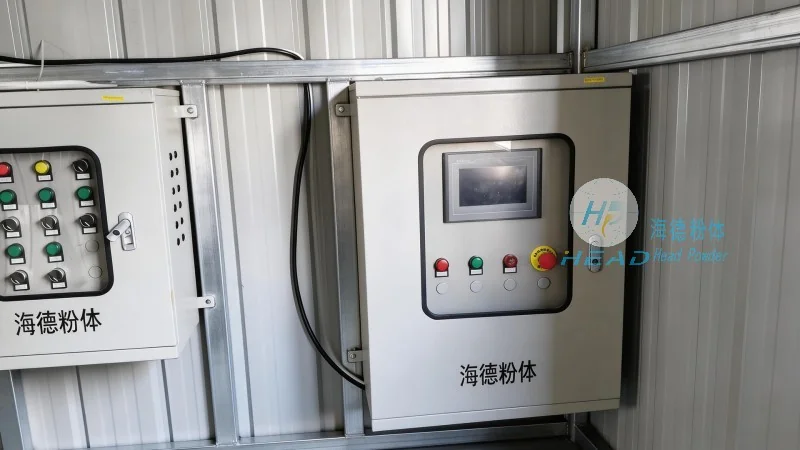
HeadPowder's dry cobblestone material conveying systems offer several technical advantages that enhance their performance and reliability. One of the primary benefits is the use of high-quality materials and components, which are resistant to abrasion and corrosion, extending the service life of the equipment. The advanced control systems provide precise monitoring and adjustment of the conveyor speed and load, ensuring consistent material flow. This leads to improved productivity and reduced operational costs. Additionally, the modular design of the systems allows for easy maintenance and repairs, minimizing downtime and maintenance expenses. The systems are also equipped with safety features, such as emergency stop buttons and overload protection, to ensure the safety of operators and equipment. Performance metrics, such as throughput capacity and energy efficiency, are optimized through rigorous testing and engineering, resulting in systems that deliver high performance while consuming minimal energy. HeadPowder's commitment to innovation and quality ensures that their dry cobblestone conveying systems are among the most reliable and efficient in the industry, meeting the demands of modern industrial applications.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced material handling solutions, including dry cobblestone material conveying systems. With years of experience and expertise in the field, HeadPowder has developed systems that are tailored to the unique needs of various industrial applications. The company's focus on quality, durability, and efficiency has made their products a preferred choice for businesses in the construction, mining, and recycling industries. By leveraging cutting-edge technology and robust engineering, HeadPowder continues to deliver high-performance solutions that enhance productivity and reduce operational costs. For more information about their dry cobblestone material conveying systems and other material handling solutions, please contact HeadPowder Engineering Co., Ltd. at their headquarters in Shandong, China.