

Operation Process and Working Principle of Coal Ash Material Handling System Equipment
Coal ash, as a byproduct of coal combustion in thermal power plants, requires efficient handling and transportation systems to ensure safe and reliable operation. The coal ash material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is designed to address these challenges through a comprehensive approach that integrates advanced technology and robust engineering solutions. This article will explore the operation process and working principle of such systems, highlighting key components, operational procedures, and the benefits of adopting modern material handling technologies.
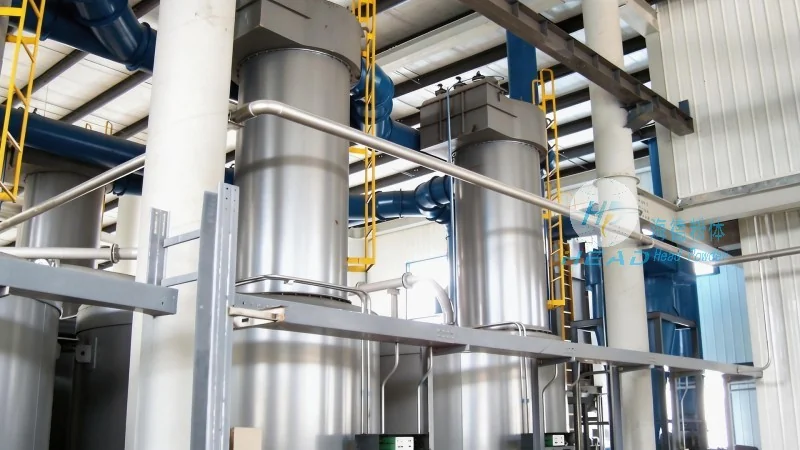
Overview of Coal Ash Material Handling Systems
Coal ash handling systems are critical infrastructure components in thermal power plants, responsible for the collection, storage, and transportation of coal ash. These systems typically consist of several interconnected parts, including ash collection devices, storage silos, conveying equipment, and discharge mechanisms. The design of these systems must adhere to strict safety and environmental regulations to minimize the risk of dust emissions and ensure compliance with industrial standards. Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of customized coal ash handling solutions tailored to the specific needs of power generation facilities.
Key Components and Their Functions
The coal ash material handling system comprises several key components, each playing a vital role in the overall operation. The primary components include ash collection hoppers, conveyor belts or screw conveyors, storage silos, and control systems. The ash collection hoppers are strategically positioned to capture ash from boilers or other combustion sources, ensuring a continuous flow of material. The conveying equipment, such as belt conveyors or pneumatic systems, transports the collected ash from the collection points to the storage silos. The storage silos are designed to hold large volumes of ash, providing a buffer for downstream processing or disposal. The control systems monitor and regulate the entire process, ensuring smooth operation and preventing system failures.
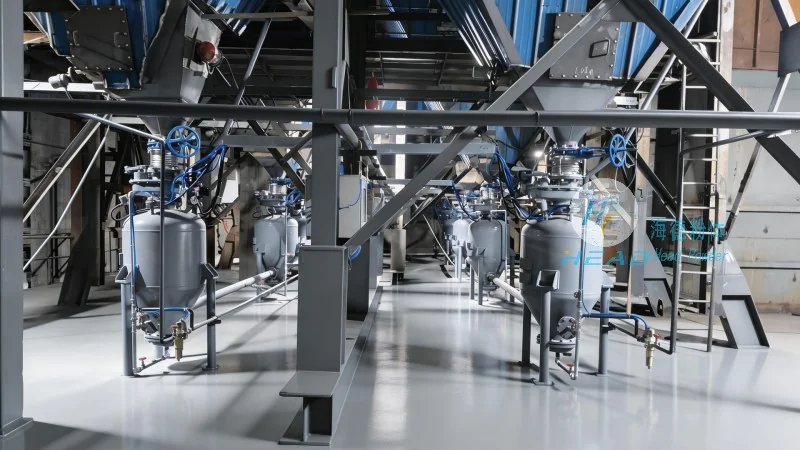
Operation Process of the Coal Ash Handling System
The operation process of the coal ash material handling system begins with the collection of ash from the combustion chamber. The ash falls into the collection hopper, where it is then transferred to the conveying equipment. The conveyor system moves the ash through a series of sections, possibly including elevators or incline conveyors, to transport it to the storage silo. The control system continuously monitors the flow rate, pressure, and temperature of the ash, adjusting the operation of the conveying equipment as needed to maintain optimal performance. When the storage silo reaches a certain level, the ash is discharged through a discharge mechanism, such as a gate valve or a rotary valve, for further processing or disposal. The entire process is automated, with minimal human intervention required, ensuring efficiency and safety.
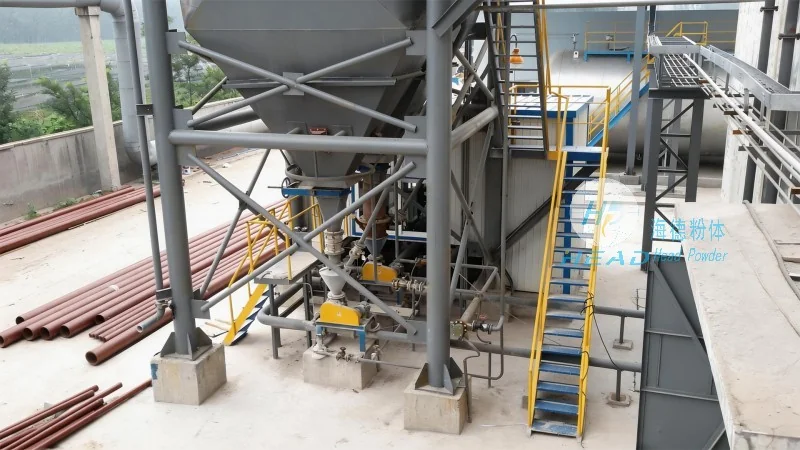
Working Principle of the System
The working principle of the coal ash material handling system is based on the principles of gravity and mechanical force. The ash collection hopper uses gravity to collect ash from the combustion source, while the conveying equipment utilizes mechanical power to transport the ash to the storage silo. The storage silo stores the ash under controlled conditions, preventing dust emissions and ensuring stable operation. The control system uses sensors and actuators to regulate the flow of ash, ensuring that the system operates within safe and efficient parameters. The system is designed to be robust and reliable, with redundant components to prevent failures and ensure continuous operation. The use of advanced materials and engineering designs enhances the durability and performance of the system, reducing maintenance costs and increasing operational efficiency.
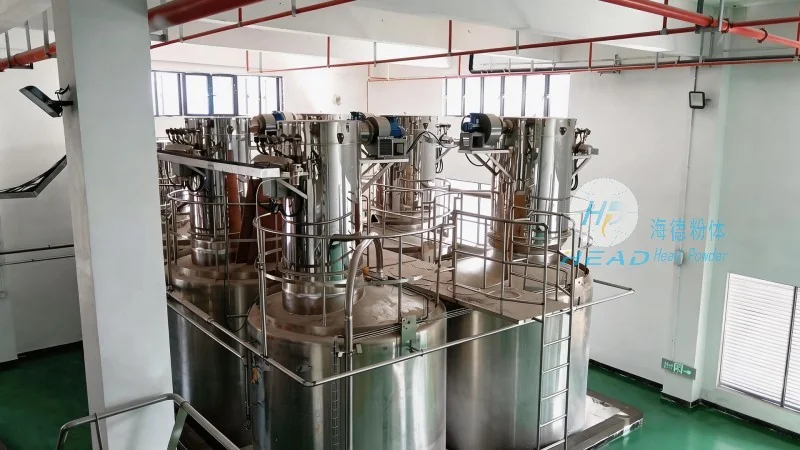
Benefits and Advantages of the System
The adoption of modern coal ash material handling systems offers several benefits to power generation facilities. These systems improve operational efficiency by reducing downtime and increasing throughput. They also enhance safety by minimizing the risk of dust explosions and other hazards associated with coal ash handling. The automated control systems provide real-time monitoring and data analysis, enabling operators to make informed decisions and optimize the system performance. Additionally, the systems are designed to comply with environmental regulations, reducing the environmental impact of coal ash disposal. The customized solutions provided by Shandong HeadPowder Engineering Co., Ltd. ensure that the systems are tailored to the specific needs of each facility, maximizing the benefits and minimizing the costs.
Conclusion
In conclusion, the coal ash material handling system equipment developed by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient and safe handling of coal ash. The system's operation process and working principle are based on advanced engineering principles and technology, ensuring optimal performance and reliability. The benefits of adopting such systems include improved operational efficiency, enhanced safety, and compliance with environmental regulations. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide customized solutions to meet the evolving needs of the power generation industry, ensuring that coal ash is handled in a responsible and sustainable manner.