

Operation Process and Working Principle of Coal Sand Material Handling System Equipment
The coal sand material handling system, as a critical component in industrial material transport, plays a vital role in ensuring efficient and safe material transfer. This system is designed to handle coal and sand materials, which are commonly used in various industrial applications such as mining, construction, and energy production. The operation process of this system involves several key stages, each contributing to the seamless movement of materials from the source to the destination. The system is engineered by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, ensuring high-quality and reliable performance.
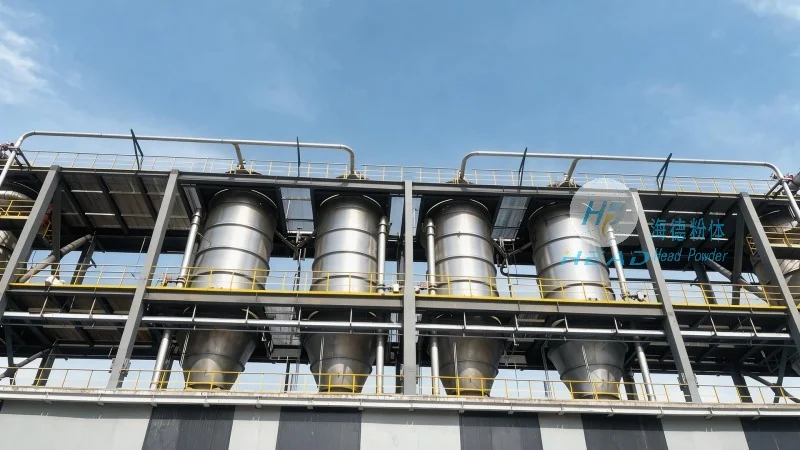
Key Components of the Coal Sand Material Handling System
The system typically consists of multiple components that work in harmony to achieve efficient material transport. These components include feeders, conveyors, storage bins, and control systems. The feeders are responsible for uniformly feeding the coal and sand materials into the conveyor system, ensuring a consistent flow rate. The conveyors, which can be of various types like belt conveyors or screw conveyors, transport the materials horizontally or vertically. Storage bins are used to temporarily hold the materials before they are further processed or transported. The control systems monitor and regulate the operation of all components, ensuring optimal performance and safety. Each component is designed to work in tandem, maximizing the system's overall efficiency.
Working Principle of the Material Handling System
The working principle of the coal sand material handling system is based on mechanical and hydraulic systems that facilitate the movement of materials. The feeders use mechanical mechanisms to deliver the materials into the conveyor. The conveyor system utilizes friction or gravity to move the materials along its path. For vertical transport, elevators or bucket elevators are employed to lift the materials to higher levels. The control system uses sensors and controllers to adjust the speed and direction of the conveyor, ensuring that the materials are transported at the desired rate. This integrated approach ensures that the system operates efficiently and reliably, minimizing downtime and maximizing productivity. The system's design allows for flexibility in handling different material types and sizes, making it suitable for diverse industrial applications.
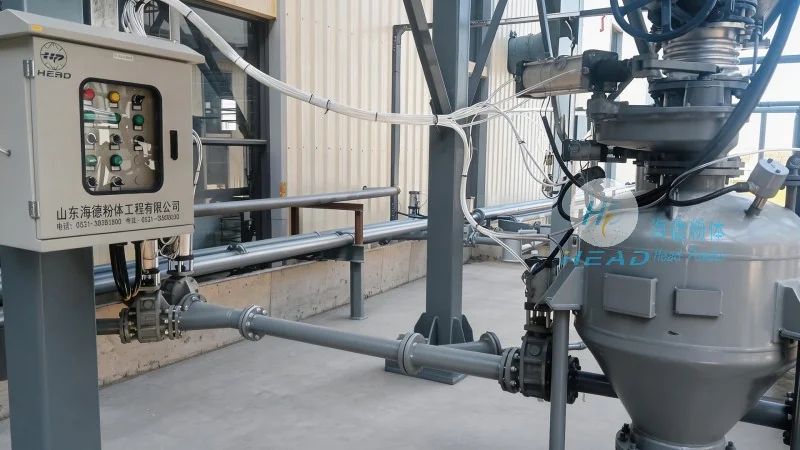
Operation Process Flow
The operation process of the coal sand material handling system begins with the raw materials being fed into the system through the feeders. The materials are then transported by the conveyor system to the storage bins or processing units. The control system continuously monitors the flow rate and position of the materials, adjusting the operation of the feeders and conveyors as needed. When the storage bins reach a certain level, the system may pause or slow down to prevent overfilling. The entire process is automated, with minimal human intervention required, except for periodic maintenance and monitoring. This automation not only enhances efficiency but also reduces the risk of human error, ensuring consistent material handling performance.
Advantages of the Coal Sand Material Handling System
The coal sand material handling system offers several advantages over traditional manual handling methods. Firstly, it significantly increases the efficiency of material transport, reducing the time and labor required for material handling. Secondly, it ensures consistent and uniform material flow, which is crucial for maintaining quality in downstream processes. Thirdly, the system enhances safety by minimizing the risk of accidents associated with manual handling of heavy or bulk materials. Additionally, the automated control system reduces the likelihood of errors and improves overall system reliability. These advantages make the system a preferred choice for industries that require high-volume and continuous material transport.
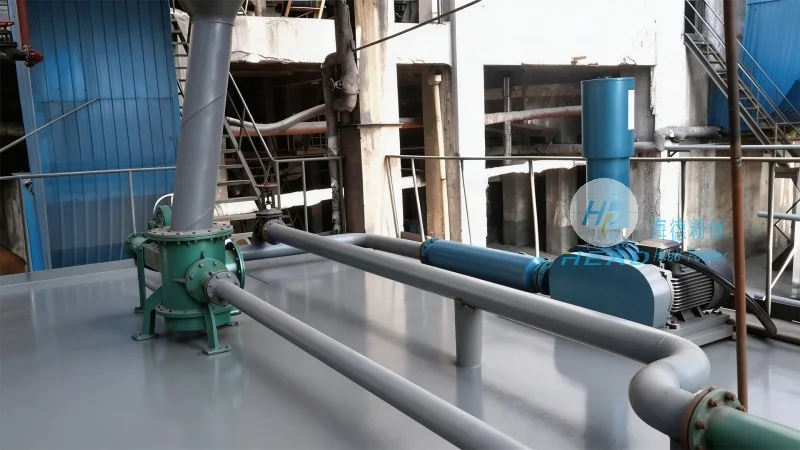
Application Scenarios
The coal sand material handling system is widely used in various industrial applications. In the mining industry, it is used to transport coal from the mine to processing facilities, where it is prepared for further use. In the construction industry, it is used to transport sand and other aggregates to construction sites, where they are used in concrete and other building materials. In the energy sector, it is used to transport coal to power plants for combustion, generating electricity. The system's adaptability to different materials and operating conditions makes it a versatile solution for various industrial needs. Its ability to handle bulk materials in large quantities makes it ideal for applications where high throughput is required.
Maintenance and Safety Considerations
To ensure the long-term performance and safety of the coal sand material handling system, regular maintenance is essential. This includes checking the condition of the conveyor belts, lubricating moving parts, and inspecting the control system components. Safety considerations are also critical, as the system handles bulk materials that can pose a risk of entrapment or injury. Proper safety measures, such as guardrails, emergency stop buttons, and regular safety training for operators, are necessary to prevent accidents. By adhering to these maintenance and safety practices, the system can operate efficiently and safely for extended periods. The manufacturer, Shandong HeadPowder Engineering Co., Ltd., provides comprehensive maintenance services and support to ensure the system's optimal performance and longevity.