

Operation Process and Working Principle of Corn Material Handling System Equipment
The corn material handling system equipment developed by Shandong HeadPowder Engineering Co., Ltd. based in Shandong, China, is engineered to provide efficient and reliable transport solutions for corn and other agricultural materials. This system integrates multiple components that work together to streamline the material handling process from intake to final storage or packaging.
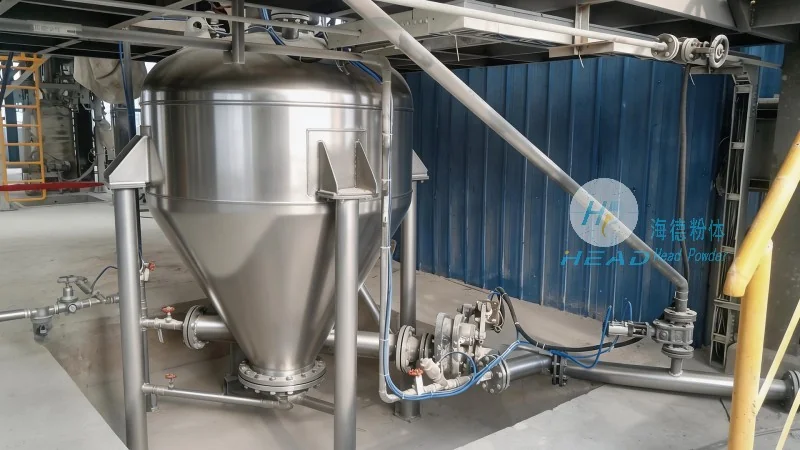
Operation Process of Corn Material Handling System Equipment
The operation process of the corn material handling system begins with the intake of raw corn material. The material is typically fed into the system through a hopper or a feeding conveyor, which ensures a consistent flow into the primary processing stage. The first major component is the primary conveyor or elevator, which lifts the corn from ground level to an elevated position, typically to a processing or storage level. This initial lifting step is crucial as it allows the material to be moved vertically, overcoming the height difference between the ground and the processing facility.
Following the lifting stage, the corn material is transferred to a processing unit. This unit may include cleaning equipment such as vibrating screens or air classifiers. The vibrating screens use mechanical vibrations to separate larger impurities like stones or debris from the corn kernels. Air classifiers, on the other hand, utilize air flow to separate lighter impurities or dust from the material. The cleaned corn then proceeds to the next stage, which is often a storage silo or a packaging line.
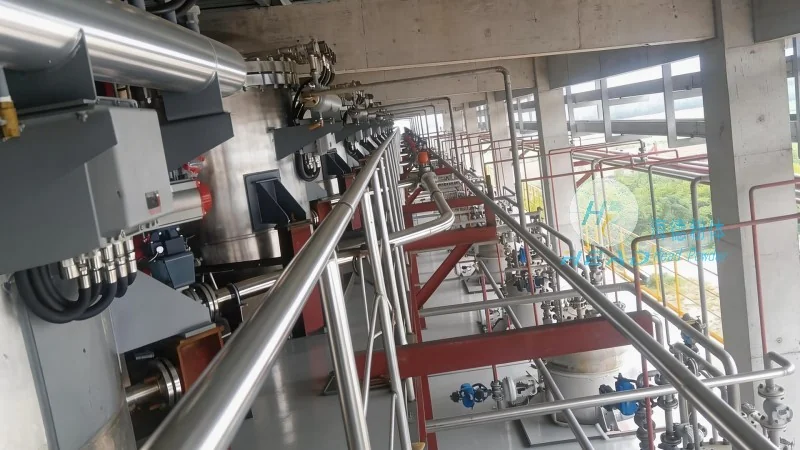
The final stage involves the storage or packaging of the processed corn. The corn is stored in large silos, which are designed to maintain the quality and moisture content of the grain. Alternatively, the corn may be packaged into bags or containers for distribution to markets. The system ensures that the material is handled gently to prevent damage to the kernels, which is essential for maintaining the quality of the final product.
Working Principle of Corn Material Handling System Equipment
The working principle of the corn material handling system is based on mechanical energy conversion and precise material flow control. The system is powered by electric motors that drive the conveyor belts, elevators, and other moving parts. These motors convert electrical energy into mechanical energy, which is then used to move the corn through the system.
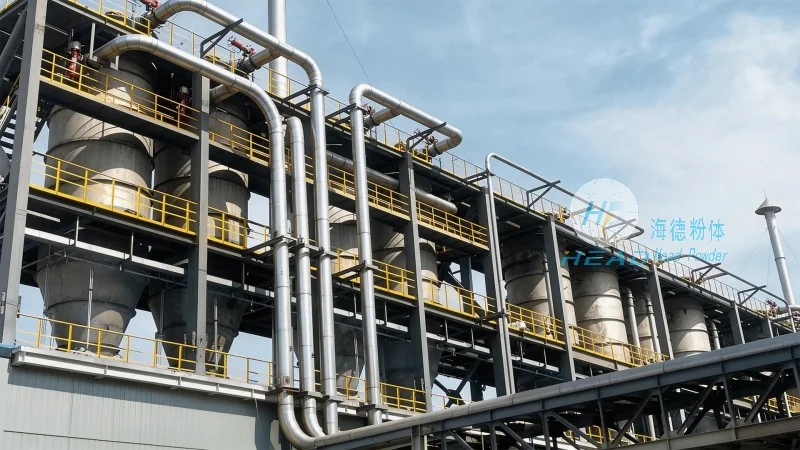
The control system plays a vital role in the operation. Sensors are installed at various points in the system to monitor the flow rate, position, and level of the material. For example, level sensors in the hopper detect when the material is low and trigger the feeding mechanism to add more material. Flow sensors in the conveyor belts monitor the speed and volume of the material, ensuring that the system operates at optimal capacity without overloading or underloading.
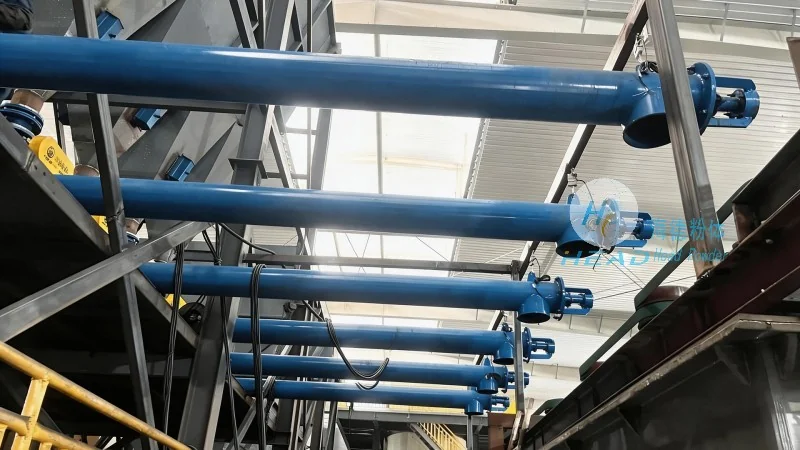
The system also incorporates safety features to prevent accidents and equipment damage. Overload sensors detect when the conveyor belt is carrying too much material and automatically reduce the speed or stop the system. This prevents blockages and reduces the risk of equipment failure. Additionally, the system is designed with easy access points for maintenance, allowing technicians to perform routine checks and repairs without disrupting the entire operation.
In summary, the corn material handling system equipment from Shandong HeadPowder Engineering Co., Ltd. combines advanced technology and robust design to provide efficient and reliable solutions for corn material transport. The integrated components and precise control systems ensure that the material is handled safely and effectively from intake to final storage or packaging.