

Operation Process and Working Principle of Coke Material Pneumatic Conveying
For industrial applications requiring efficient and reliable transport of coke material, pneumatic conveying systems offer a robust solution. These systems are designed to handle bulk materials like coke, ensuring smooth and continuous operation in various industrial settings. The technology behind pneumatic conveying leverages air flow to move material through pipelines, providing a dust-free and compact method of material handling compared to traditional methods.

Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner for industries seeking efficient material transport solutions. HeadPowder's expertise lies in developing customized systems tailored to specific operational requirements, ensuring optimal performance and reliability for clients across different sectors.
Key Components and Working Principle
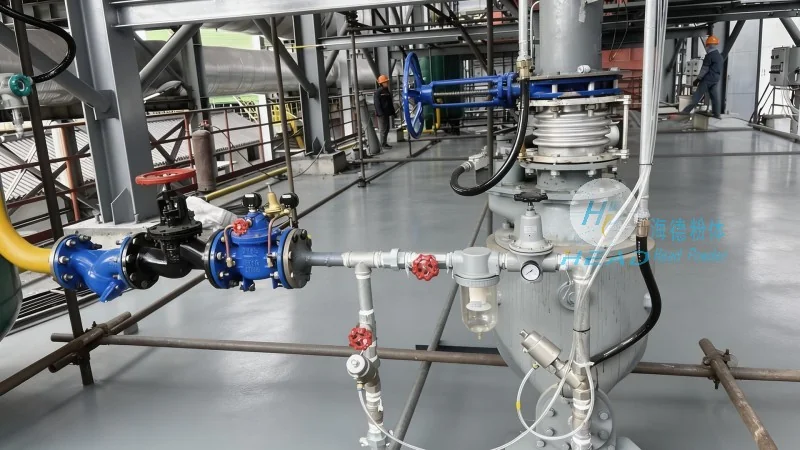
The core of a pneumatic conveying system for coke material involves several key components that work in tandem to achieve efficient material transport. The system typically includes a hopper for material storage, a conveyor line with appropriate piping, a blower or air compressor to generate the necessary air pressure, and a control system to regulate the flow. The working principle revolves around the use of air to create a flow that lifts and transports the coke particles through the pipeline. As air is introduced into the system, it creates a low-pressure zone that draws the material from the hopper into the conveyor line. The material is then carried along the pipeline by the air stream, with the velocity and pressure maintained to ensure stable transport without material degradation or blockage.
Operation Process of Coke Material Pneumatic Conveying
The operation process of a coke material pneumatic conveying system begins with material loading into the hopper. The material is then fed into the conveyor line as air is introduced by the blower. The air flow creates a consistent stream that moves the coke particles through the pipeline to the discharge point. The system is equipped with sensors and controls to monitor the flow rate, pressure, and material level, ensuring that the operation remains stable and efficient. During the process, the system maintains a consistent air pressure and flow rate to prevent material settling or blockage in the pipeline. The discharge point is designed to handle the material smoothly, ensuring that it is deposited accurately at the intended location. The entire process is automated, allowing for continuous operation with minimal human intervention, which enhances productivity and reduces operational costs.
Advantages of Pneumatic Conveying for Coke Material Handling
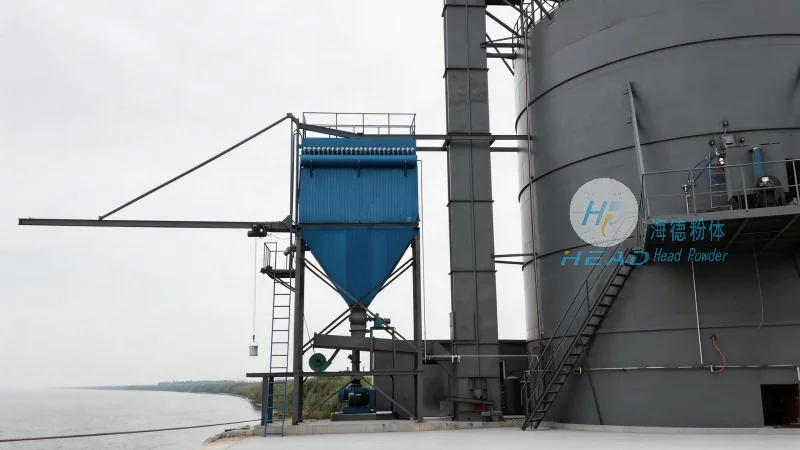
Compared to traditional material handling methods such as belt conveyors or bucket elevators, pneumatic conveying offers several advantages for coke material transport. One of the primary benefits is the ability to handle material in a dust-free environment, which improves workplace safety and reduces the risk of material contamination. The system also provides a compact and space-saving solution, as the conveyor line can be installed in a vertical or horizontal configuration, optimizing the use of available space in industrial facilities. Additionally, pneumatic conveying systems are highly flexible, allowing for easy integration with existing production lines and modifications to accommodate changes in material flow requirements. The technology also minimizes material degradation, as the gentle handling by air flow preserves the quality of the coke material, which is crucial for downstream processes.
Customization and Application Scope
HeadPowder recognizes that each industrial application has unique requirements, and therefore, offers customized pneumatic conveying solutions tailored to specific needs. The company's engineers work closely with clients to understand their operational challenges and design systems that meet their performance and efficiency goals. The applications of coke material pneumatic conveying span across various industries, including steel production, chemical processing, and power generation. In steel plants, for example, the system is used to transport coke from storage facilities to blast furnaces, ensuring a steady supply of material for the production process. In chemical plants, the system may be used to handle coke as a raw material for various chemical reactions, requiring precise control over the material flow. The versatility of the system makes it suitable for a wide range of industrial applications, providing a reliable solution for material transport needs.