

Introduction to Cobalt Hydroxide Pneumatic Conveying Equipment and Its Structural Principles
For industrial applications involving the handling of cobalt hydroxide, efficient and reliable material transport is crucial. The pneumatic conveying system, specifically designed for this purpose, offers a solution that combines advanced engineering with practical functionality. This equipment is essential for processes that require the safe and effective movement of cobalt hydroxide from one location to another within a production facility. The design of such a system is tailored to meet the unique characteristics of cobalt hydroxide, ensuring optimal performance and minimal material degradation.
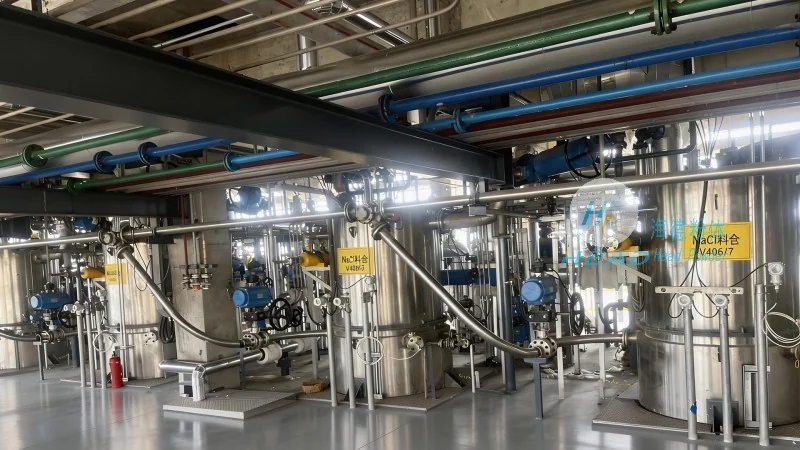
HeadPowder, a leading manufacturer in the field, specializes in the development and production of high-quality pneumatic conveying equipment. As a company based in Shandong, China, HeadPowder leverages its expertise and local manufacturing capabilities to deliver robust solutions for various industrial needs. The company's commitment to precision engineering and customer satisfaction is reflected in the design and construction of its pneumatic conveying systems.
The core of the cobalt hydroxide pneumatic conveying equipment lies in its structural components, which are engineered to handle the specific properties of cobalt hydroxide. The system typically includes a hopper for material storage, a feeder to control the flow rate, and a conveying pipeline that transports the material through the use of air pressure. The hopper is designed with a sloped bottom to facilitate smooth material discharge, preventing blockages and ensuring consistent flow. The feeder, often a rotary valve or a screw feeder, regulates the amount of material entering the pipeline, maintaining a stable conveying rate.
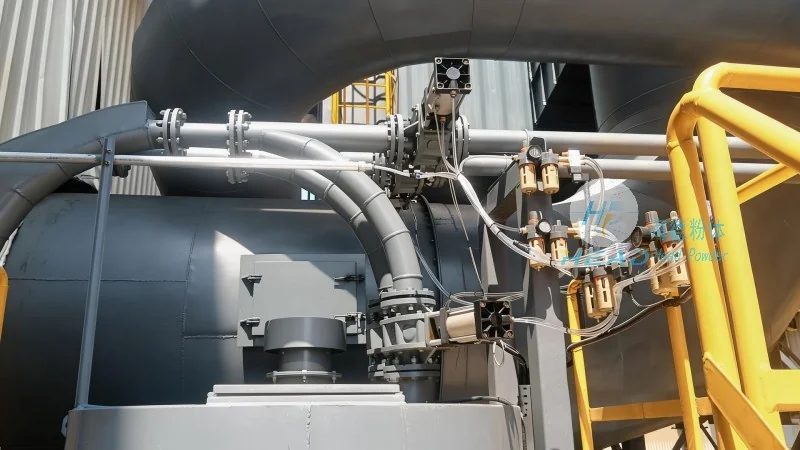
The conveying pipeline is a critical component, constructed from materials that are resistant to corrosion and wear, suitable for the chemical properties of cobalt hydroxide. The system may incorporate various sections, such as vertical and horizontal runs, with appropriate bends and elbows to direct the material flow. The air pressure system, which drives the conveying process, is carefully designed to provide sufficient velocity to keep the material suspended and prevent settling. This ensures that the material travels efficiently through the pipeline without clogging or losing its integrity.
At the receiving end of the system, a separator or a cyclone is used to separate the material from the air stream. The separator works by utilizing centrifugal force to pull the heavier cobalt hydroxide particles out of the air, allowing the air to be recirculated or discharged. This step is vital for maintaining the purity of the material and preventing contamination. The separated material is then collected in a receiving hopper, ready for further processing or storage.
The control system of the pneumatic conveying equipment plays a pivotal role in its operation. It monitors and adjusts various parameters, such as air pressure, flow rate, and material level, to ensure the system runs smoothly and efficiently. Modern control systems often include sensors and automation features that provide real-time data and allow for remote monitoring. This enhances operational safety and reduces the need for manual intervention, making the process more reliable and cost-effective.
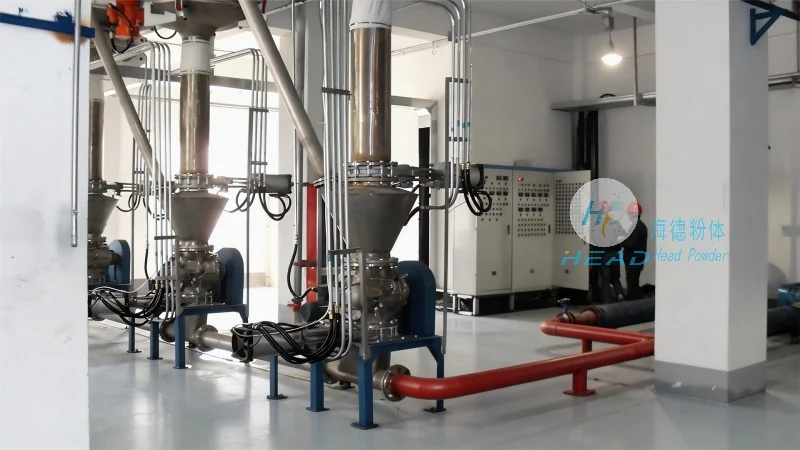
HeadPowder's approach to designing and manufacturing cobalt hydroxide pneumatic conveying equipment is rooted in a deep understanding of the material's behavior and the requirements of industrial applications. The company's engineers work closely with clients to tailor the system to specific process needs, ensuring that the equipment meets both performance and safety standards. By integrating advanced materials and engineering principles, HeadPowder delivers solutions that are durable, efficient, and tailored to the unique demands of cobalt hydroxide handling.
In summary, the cobalt hydroxide pneumatic conveying equipment is a sophisticated system that combines structural engineering with pneumatic principles to facilitate the efficient transport of cobalt hydroxide. From the initial storage in the hopper to the final separation at the receiving end, each component is designed to work in harmony, ensuring optimal performance. HeadPowder, with its expertise and commitment to quality, provides reliable solutions that support the industrial processes involving cobalt hydroxide, contributing to the overall efficiency and productivity of the manufacturing operations.