

Long - Distance Pneumatic Conveying System for Corn Kernels
Efficient and reliable long - distance pneumatic conveying systems are crucial for the modern agricultural and food processing industries, particularly when handling bulk materials like corn kernels. These systems ensure seamless material transport from storage to processing facilities, maintaining product quality and operational efficiency. In this context, Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, offers advanced solutions tailored to the specific needs of corn kernel transportation.
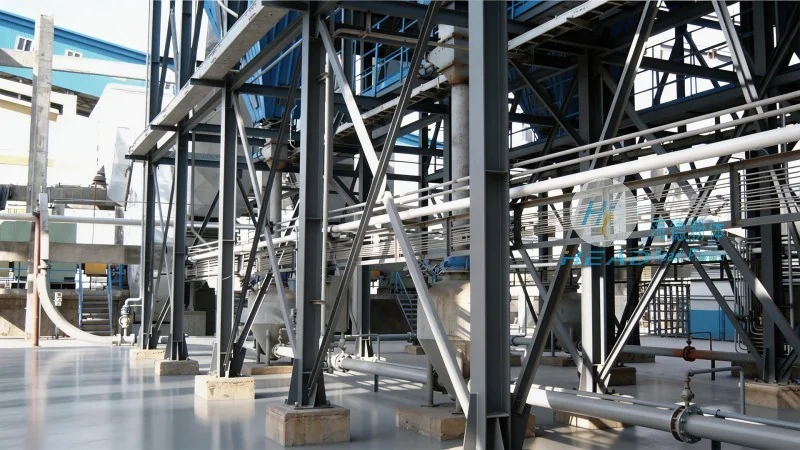
Company Overview and Expertise
HeadPowder, the professional brand under Shandong HeadPowder Engineering Co., Ltd., specializes in designing and manufacturing high - performance pneumatic conveying systems. With years of experience in the industry, the company has built a strong reputation for delivering robust, durable, and energy - efficient solutions. The company's engineering team leverages cutting - edge technology and extensive knowledge to develop systems that meet the stringent requirements of corn kernel handling, ensuring optimal performance in various operational conditions.
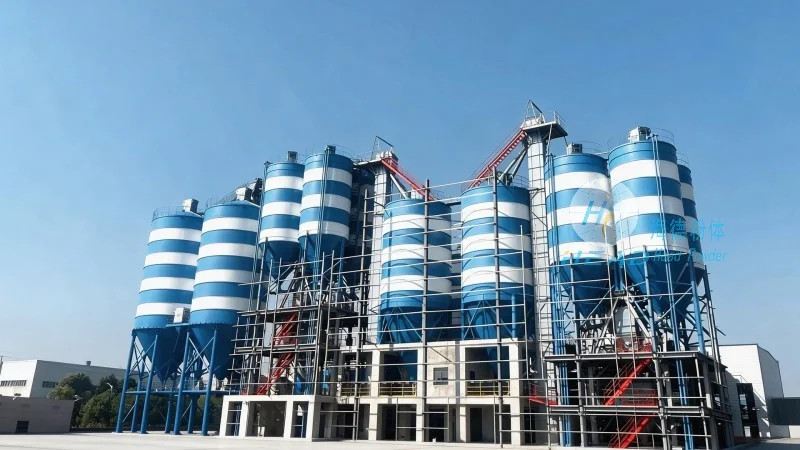
Key Features of the Long - Distance Pneumatic Conveying System
The long - distance pneumatic conveying system for corn kernels is engineered with several key features that enhance its functionality and reliability. Firstly, the system utilizes advanced air - flow control mechanisms to maintain consistent material flow rates, preventing blockages and ensuring smooth transport over extended distances. The design incorporates high - quality materials resistant to corrosion and wear, which is essential for handling corn kernels that may contain moisture or impurities. Additionally, the system is equipped with intelligent monitoring and control systems that allow operators to track performance in real - time, enabling quick adjustments to maintain optimal operation. This technology not only improves efficiency but also reduces downtime and maintenance costs.
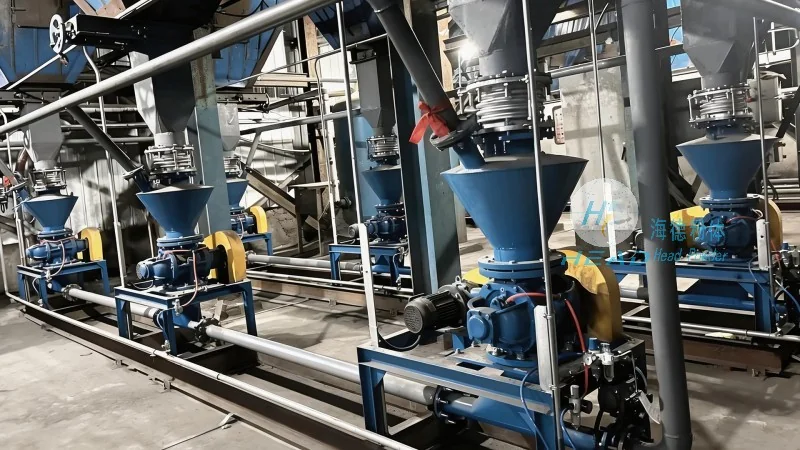
Application and Operational Benefits
These conveying systems are widely used in corn processing facilities, including grain elevators, feed mills, and bio - fuel production plants. The primary benefit is the ability to transport large volumes of corn kernels over long distances without the need for intermediate storage or manual handling. This reduces labor costs and minimizes the risk of product contamination or loss. The system's design also allows for flexible integration with existing processing lines, making it a cost - effective upgrade for facilities looking to improve their material handling capabilities. Furthermore, the energy - efficient operation of the system contributes to lower operational costs and a smaller environmental footprint, aligning with modern sustainability goals in the agricultural sector.
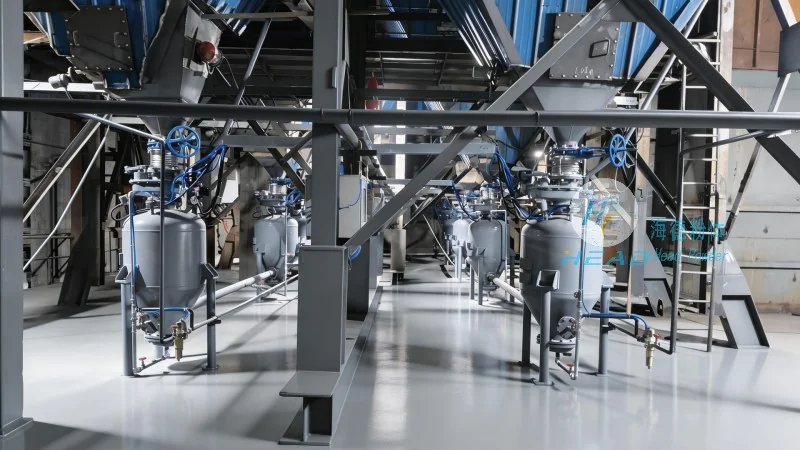
Customization and After - Sales Support
Shandong HeadPowder Engineering Co., Ltd. understands that each corn processing facility has unique requirements. Therefore, the company offers customized solutions tailored to specific site conditions, material characteristics, and operational needs. The engineering team works closely with clients to design systems that maximize efficiency and minimize costs. After the system is installed, the company provides comprehensive after - sales support, including regular maintenance services, technical assistance, and spare parts supply. This ensures that the system continues to operate at peak performance throughout its service life, providing long - term value to the client.