

Classification and Application Analysis of Dust Air-Driven Conveying Systems
HeadPowder, a leading provider in the field, specializes in dust air-driven conveying systems. These systems are essential for efficiently transporting fine particles and dust in various industrial applications. The technology leverages air pressure or vacuum to move materials, offering a flexible and effective solution for material handling challenges.
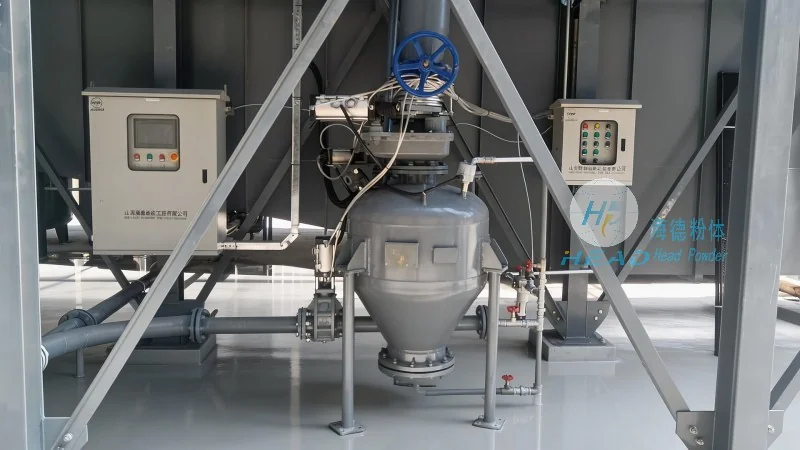
Classification of Dust Air-Driven Conveying Systems
There are primarily two main categories of dust air-driven conveying systems: positive pressure and negative pressure systems. Positive pressure systems use compressed air to push material through a pipeline, while negative pressure systems employ vacuum to draw material into the system. Each type has distinct advantages and is suited to different operational requirements.
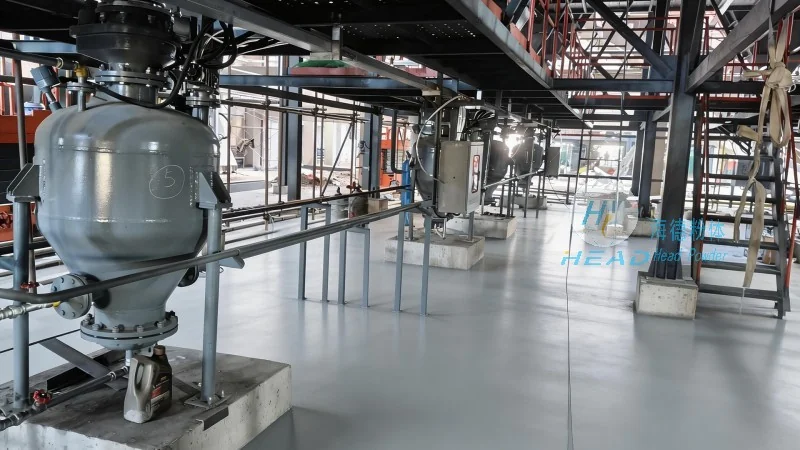
Positive Pressure Conveying Systems
Positive pressure systems are commonly used for applications requiring high material flow rates and long-distance transport. They are particularly effective in environments where dust containment is critical. The system operates by injecting compressed air into the material stream, creating a pressure differential that propels the material forward. This method ensures consistent material flow and minimal particle degradation. HeadPowder's positive pressure solutions are designed to handle a wide range of dust types, from light powders to heavy granules, with high efficiency and reliability.
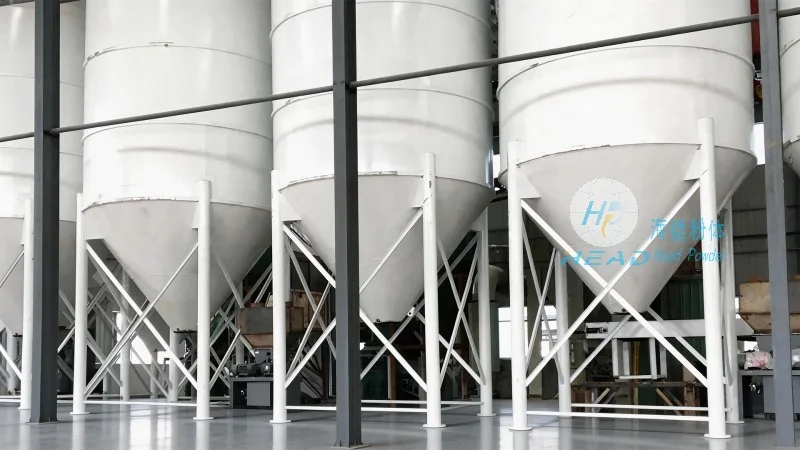
Negative Pressure Conveying Systems
Negative pressure systems are ideal for applications where dust collection and containment are paramount, such as in pharmaceutical or food processing industries. These systems use vacuum to draw material from a source and transport it to a collection point. The design minimizes dust emissions and ensures a clean working environment. HeadPowder's negative pressure solutions are equipped with advanced filtration and control mechanisms to maintain high air quality and operational safety.
Application Analysis of Dust Air-Driven Conveying Systems
The versatility of dust air-driven conveying systems makes them applicable across multiple industries. In the chemical industry, these systems are used to transport powders and granules for processing and storage. In the mining sector, they facilitate the movement of ore and tailings. The construction industry benefits from their ability to handle bulk materials like cement and sand. Additionally, in the food and pharmaceutical sectors, the systems ensure hygienic material handling, adhering to strict regulatory standards. HeadPowder's systems are tailored to meet the specific needs of each industry, ensuring optimal performance and compliance.
About HeadPowder Engineering Co., Ltd.
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted provider of advanced material handling solutions, focusing on dust air-driven conveying systems. With a commitment to innovation and quality, HeadPowder delivers systems that enhance operational efficiency and safety for its clients. The company's expertise lies in customizing solutions to meet diverse industrial requirements, ensuring reliable and effective material transport across various applications.