

Introduction to Fertilizer Pneumatic Conveying and the Working Principle of Pneumatic Conveying Syst
Pneumatic conveying systems have become a cornerstone in the agricultural and fertilizer industries, offering efficient and reliable methods for transporting bulk materials like fertilizers. These systems utilize air or gas to move powders and granules through pipelines, eliminating the need for traditional mechanical conveyors and reducing operational costs and maintenance requirements. For businesses in the fertilizer sector, understanding the principles and applications of pneumatic conveying is crucial for optimizing material handling processes and enhancing overall productivity.
The Working Principle of Pneumatic Conveying Systems
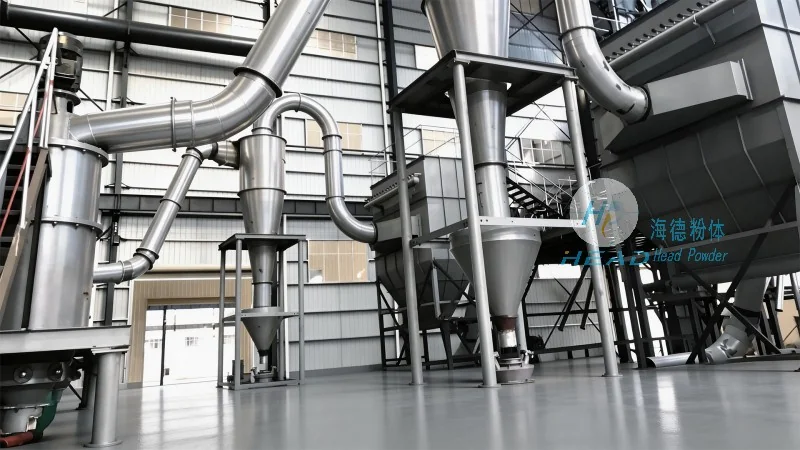
Pneumatic conveying operates on the fundamental principle of using air pressure to move material through a closed pipeline system. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure (or vacuum) systems. In positive pressure systems, air is forced into the pipeline at a higher pressure than the ambient air, pushing the material forward. This method is often used for short to medium distance transport and is suitable for handling abrasive or sticky materials. Negative pressure systems, on the other hand, create a vacuum in the pipeline, drawing material into the system from the source. This approach is ideal for longer distances and for materials that are sensitive to pressure changes or for applications requiring a closed environment to prevent dust emissions.
Key Advantages of Pneumatic Conveying for Fertilizer Transport
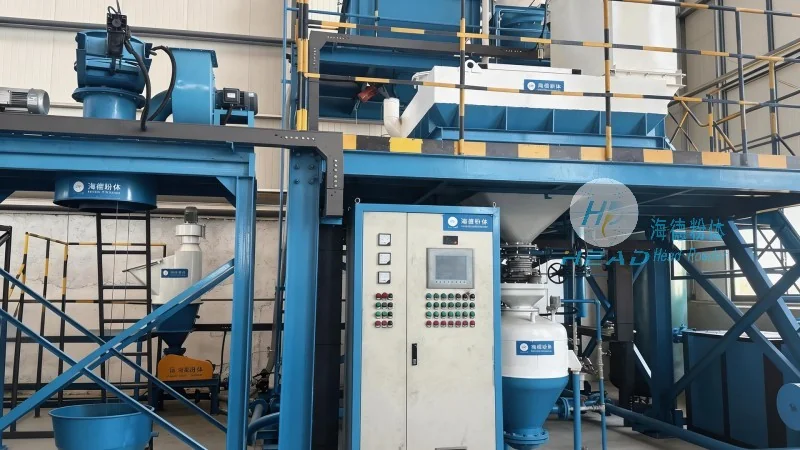
When applied to fertilizer handling, pneumatic conveying systems offer several distinct advantages. Firstly, they provide a clean and dust-free transfer process, which is essential for maintaining product quality and compliance with environmental regulations. Unlike mechanical systems that can generate dust and cause contamination, pneumatic conveying keeps the material enclosed within the pipeline, reducing the risk of product degradation and ensuring a consistent quality output. Secondly, these systems are highly efficient in terms of energy consumption and operational speed. By using air as the conveying medium, the system can move large volumes of fertilizer quickly and with minimal labor, leading to significant time and cost savings. Additionally, pneumatic conveying systems are flexible and can be easily integrated into existing production lines or expanded to accommodate increased production demands. The ability to customize the system design to match specific fertilizer types, such as granular or powdered forms, further enhances its applicability across different fertilizer products.
HeadPowder: Specializing in Pneumatic Conveying Solutions for Fertilizers
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and supply of advanced pneumatic conveying systems tailored for the fertilizer industry. With a strong presence in China, particularly in Shandong, HeadPowder leverages its extensive experience and technical expertise to deliver high-quality, reliable solutions that meet the unique demands of fertilizer handling. The company’s commitment to innovation and customer-centric approach ensures that each system is customized to the specific requirements of the client, whether it involves bulk material transport, storage, or processing. HeadPowder’s products are engineered to withstand the harsh conditions often encountered in fertilizer operations, such as high temperatures, corrosive substances, and abrasive materials, ensuring long-term durability and minimal downtime. By partnering with HeadPowder, fertilizer companies can enhance their operational efficiency, reduce maintenance costs, and improve overall product quality, all while adhering to the highest standards of safety and environmental compliance.
Conclusion: The Role of Pneumatic Conveying in Modern Fertilizer Handling
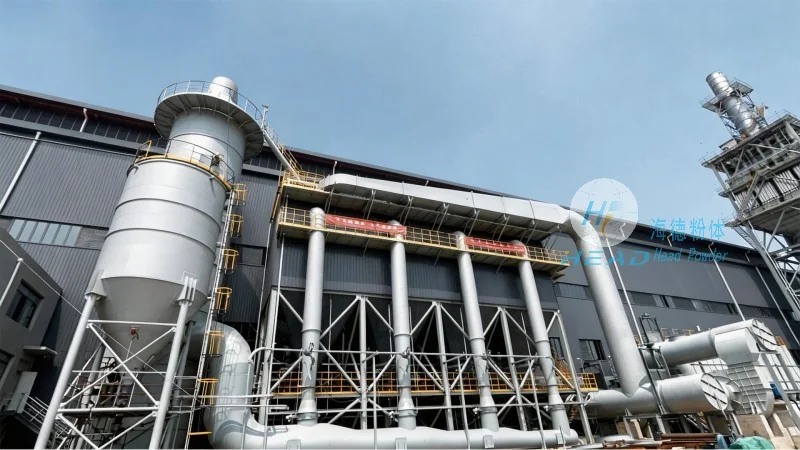
As the fertilizer industry continues to evolve, the importance of efficient and reliable material handling systems cannot be overstated. Pneumatic conveying, with its proven advantages in speed, cleanliness, and flexibility, remains a preferred choice for many businesses. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in advancing this technology, providing tailored solutions that address the specific challenges faced by fertilizer manufacturers. By investing in advanced pneumatic conveying systems, fertilizer companies can not only improve their operational performance but also contribute to sustainable and environmentally friendly practices, ensuring long-term success in a competitive market. The integration of such systems into fertilizer handling processes is a strategic move that aligns with the industry’s need for efficiency, quality, and sustainability.