

Principle of Phosphorus Pentoxide Pneumatic Conveying System
Phosphorus pentoxide (P₂O₅) is a highly reactive and hygroscopic chemical compound widely used in various industrial applications, including chemical synthesis, pharmaceutical production, and as a desiccant. The efficient and safe handling of P₂O₅ is critical due to its corrosive nature and potential for rapid moisture absorption. Pneumatic conveying systems offer a reliable method for transporting this hazardous material, ensuring minimal exposure to personnel and maintaining product integrity.
Core Principles of Pneumatic Conveying for Phosphorus Pentoxide
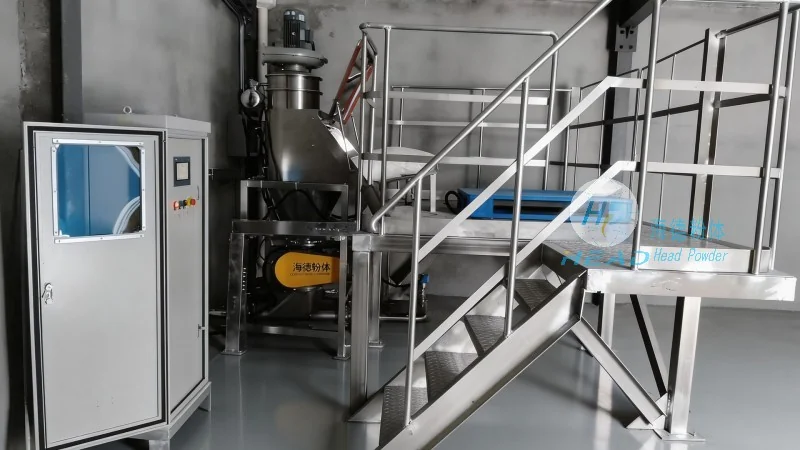
The fundamental principle of pneumatic conveying involves the use of air or other gases to transport solid particles through a pipeline. In the case of phosphorus pentoxide, the system typically operates under negative pressure (suction) or positive pressure (blowing) to move the material from a source to a destination. The choice of pressure type depends on factors such as the material's properties, the distance of transport, and the system's design requirements. Negative pressure systems are often preferred for handling P₂O₅ due to their ability to prevent dust leakage and maintain a controlled environment, reducing the risk of inhalation or contamination.
System Components and Their Functions
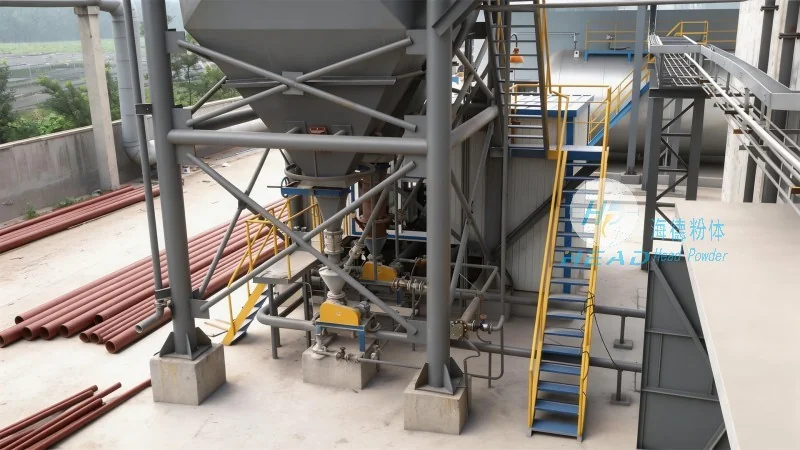
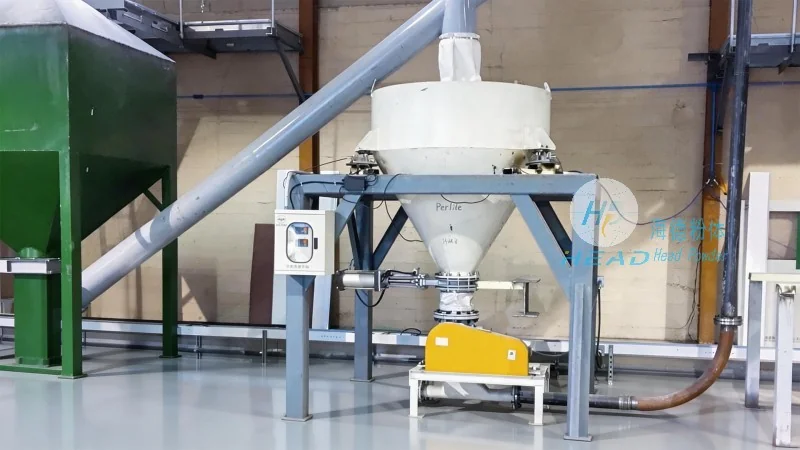
A typical phosphorus pentoxide pneumatic conveying system comprises several key components, each playing a crucial role in the overall operation. The primary components include a material feeder, a conveying pipeline, a dust collector or filter system, and a control unit. The material feeder is responsible for accurately metering the P₂O₅ and introducing it into the conveying stream. This component must be designed to handle the material's hygroscopic and abrasive characteristics, often incorporating features like a sealed hopper and a rotary valve to prevent moisture ingress and material buildup. The conveying pipeline is usually made of corrosion-resistant materials, such as stainless steel or PTFE-coated tubing, to withstand the chemical properties of P₂O₅ and minimize degradation over time. The pipeline design includes appropriate bends and fittings to maintain a smooth flow and prevent blockages. The dust collector or filter system is essential for capturing any fine particles that may escape during transport, ensuring compliance with environmental regulations and protecting downstream equipment from contamination. The control unit monitors and regulates the system's operation, adjusting air flow, pressure, and material feed rates to maintain optimal performance and safety.
Advantages of Pneumatic Conveying for Phosphorus Pentoxide Handling
Implementing a pneumatic conveying system for phosphorus pentoxide offers several advantages over traditional methods like bucket elevators or belt conveyors. One of the most significant benefits is the ability to handle the material in a closed system, which minimizes dust exposure and reduces the risk of environmental contamination. This is particularly important for P₂O₅, as it is a hazardous substance that requires strict safety protocols. Additionally, pneumatic conveying systems can transport the material over longer distances with less energy consumption compared to other methods, making them more cost-effective for large-scale operations. The system's flexibility also allows for easy integration with existing production lines, enabling seamless material transfer between processes. Furthermore, the closed nature of the system helps maintain the material's quality by preventing moisture absorption or contamination from external sources, which is critical for applications where the purity of P₂O₅ is paramount.
Application Examples and Industry Impact
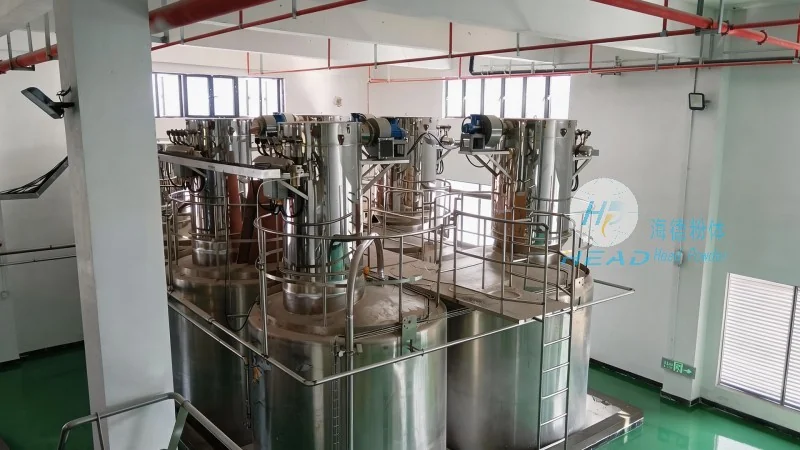
The phosphorus pentoxide pneumatic conveying system is widely used in various industries where P₂O₅ is a key raw material. In the chemical industry, the system is employed in the production of phosphoric acid, which is a precursor for fertilizers and other chemicals. The efficient transport of P₂O₅ ensures a steady supply of raw material to the production line, enhancing overall productivity. In the pharmaceutical sector, the system is used in the manufacturing of certain drugs that require high-purity P₂O₅ as an intermediate. The closed and controlled environment of the pneumatic conveying system helps maintain the material's purity, which is essential for meeting regulatory standards and ensuring product safety. Additionally, the system is utilized in the food industry for the production of certain food additives that incorporate P₂O₅ as a component. The ability to handle the material safely and efficiently has contributed to increased productivity and reduced operational risks in these industries.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for the handling and processing of hazardous materials. With a strong focus on innovation and safety, the company has developed advanced pneumatic conveying systems tailored to the unique requirements of phosphorus pentoxide and other reactive chemicals. HeadPowder's expertise lies in designing and manufacturing systems that meet the highest industry standards, ensuring reliable and efficient material transport while minimizing risks to personnel and the environment. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the chemical and pharmaceutical industries, providing tailored solutions that enhance operational efficiency and safety.
Conclusion
In conclusion, the phosphorus pentoxide pneumatic conveying system represents a sophisticated and effective solution for the safe and efficient handling of this critical chemical. By leveraging the principles of pneumatic transport and incorporating advanced engineering components, the system ensures minimal exposure to personnel, maintains product integrity, and supports high productivity in industrial applications. As a leader in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide reliable solutions that meet the evolving needs of the industry, contributing to safer and more efficient material handling practices.