

What is an Automatic Quantitative Pneumatic Powder Conveyor? And What Are Its Design Principles?
Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the research, development, and production of advanced powder handling equipment. The company focuses on providing high-quality solutions for efficient and reliable powder transportation in various industrial applications.
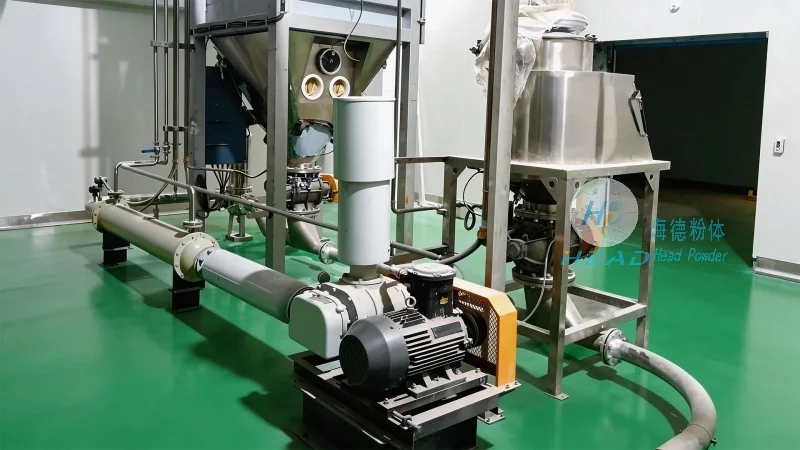
Introduction to the Automatic Quantitative Pneumatic Powder Conveyor
The automatic quantitative pneumatic powder conveyor is a sophisticated piece of equipment designed to transport and dose powders or bulk materials with high precision and efficiency. This system integrates pneumatic conveying technology with automated control mechanisms, enabling seamless and controlled movement of powders from one location to another. As a key component in modern powder processing industries, it plays a crucial role in optimizing production lines and ensuring consistent material handling.
Design Principles and Working Mechanism
The design of the automatic quantitative pneumatic powder conveyor is based on the fundamental principles of pneumatic conveying, which utilizes air as the medium to transport solid particles. The system typically consists of several core components, including a hopper for material storage, a rotary valve or feeder for controlled discharge, a pipeline system for conveying, and a receiver for material collection. The quantitative mechanism is achieved through precise control of the air flow rate and the feeding speed, ensuring that the desired amount of powder is delivered at a consistent rate. The control system, often equipped with sensors and programmable logic controllers (PLCs), monitors and adjusts the parameters in real-time to maintain accuracy and prevent overloading or underloading.
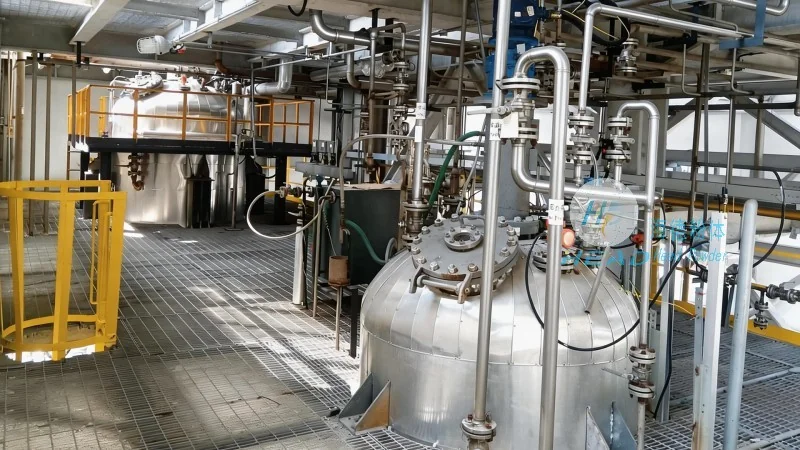
Technical Features and Advantages
One of the primary advantages of this conveyor is its ability to handle a wide range of powder characteristics, from fine powders to bulk materials, with minimal degradation or segregation. The pneumatic system provides a dust-free and hygienic environment, which is particularly important in industries such as food, pharmaceuticals, and chemicals where product purity is critical. Additionally, the automatic quantitative feature allows for precise dosing, reducing waste and improving process efficiency. The system is also designed for easy maintenance and cleaning, with components that can be easily disassembled and sanitized, ensuring compliance with industry standards and regulations.
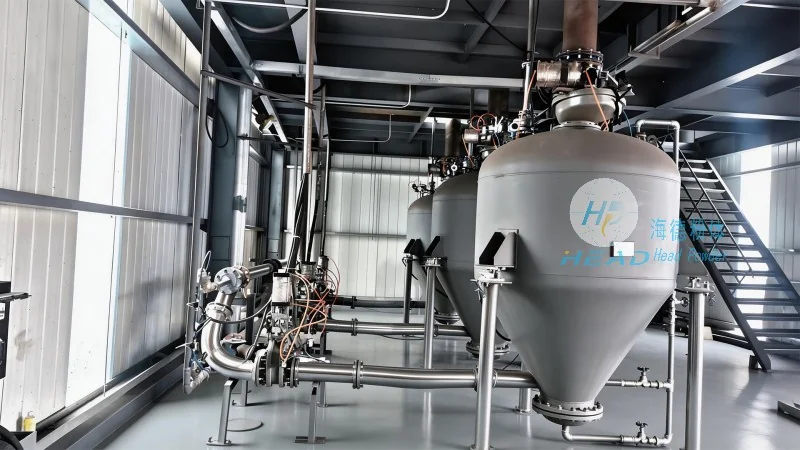
Applications in Industrial Settings
The automatic quantitative pneumatic powder conveyor is widely used in various industries where bulk powder handling is essential. In the food and beverage industry, it is used for transporting ingredients like flour, sugar, and spices with high accuracy, ensuring consistent product quality. In the pharmaceutical sector, it plays a vital role in the handling of active pharmaceutical ingredients (APIs) and excipients, maintaining strict purity and dosage requirements. The chemical industry also benefits from this equipment for transporting raw materials and finished products, enhancing safety and efficiency in production processes. Furthermore, in the agricultural and mining sectors, it aids in the transport of fertilizers, minerals, and other bulk materials, improving operational productivity.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. offers the automatic quantitative pneumatic powder conveyor as a reliable and efficient solution for modern powder handling needs. By combining advanced pneumatic technology with precise automation, this equipment ensures consistent performance, high accuracy, and minimal maintenance. With its ability to handle diverse powder types and its compliance with industry standards, it is an essential asset for businesses seeking to optimize their production processes and enhance overall operational efficiency.